Identified steel-plate and coating review, setup of a handheld plasma cutter, independent support of retained plate and cut piece, controlled cutting, authorized consumable replacement and inspection handover.
Stop for damaged torch or cables, unreliable work-return connection, failed fume controls, fire risk or changing plate support. Hold the final separating cut if either piece could tip, fall or interrupt the return path.
Reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and site approval are required before use.
1. Legal and technical scope
For covered general-industry cutting, OSHA 1910.252 addresses fire prevention, personnel protection and ventilation. Where its fire-watch conditions apply, the federal rule requires at least a half hour of post-work fire watch; applicable site, adopted-code or insurer requirements may be more protective. Construction cutting requires the relevant Part 1926 welding and cutting provisions. Equipment servicing and electrical work require their applicable energy-control rules and qualified scope.
Determine Federal OSHA or the applicable OSHA-approved State Plan, including public/private employer coverage. State Plans must be at least as effective and can impose different or additional requirements. The actual activity determines construction versus general-industry scope. Manufacturer instructions, consensus standards, project design and site approvals have distinct roles; this page is not a finding of nationwide compliance.
| Basis | Application and limits |
|---|---|
| OSHA 1910.252 | Selected fire authorization, fire watch, hot-metal warning and ventilation provisions; jurisdiction and actual cutting conditions matter. |
| OSHA 1910.147 | Applicable general-industry servicing energy controls; not an internal electrical repair instruction. |
| Hypertherm handheld air-plasma overview | Manufacturer overview including retained work-return connection. It explicitly does not replace the actual operator manual. Model-specific settings and internal service procedures were not adopted. |
2. Scope and required inputs
Included: Identified steel-plate and coating review, setup of a handheld plasma cutter, independent support of retained plate and cut piece, controlled cutting, authorized consumable replacement and inspection handover.
Separate review: Unknown containers or piping, confined spaces, underwater cutting, automated cutting-system servicing and internal power-supply electrical maintenance require separate assessment and qualified procedures.
| Input | Required evidence |
|---|---|
| Plan plate and cut path | Plate and cut-piece IDs; Cut path and final support; Material and coating evidence; Lower-area work boundary |
| Inspect supply and gas | Supply earth and insulation; Work-return connection; Service and energy boundary; Gas hose and filter condition |
| Cut and monitor | Extraction and air conditions; Screens and filter selection; Sparks and combustibles; Settings and cut condition |
| Inspect and hand over | Heat and access restrictions; Storage and removal condition; Part inspection and open defects; Fire-watch closure record |
Use actual model instructions for supply, gas, consumables, current, torch position, isolation and cooling. Review material and coating hazards, extraction, eye and skin protection and noise. Determine support loading and cut sequence from the actual geometry; no universal support spacing or equipment setting is provided.
3. Eight-stage JSA
P = likelihood; S = severity; R = risk under the site method; A = acceptance or authorization as defined by the site. Leave these blank until actual assessment and control verification. A low score does not override a legal requirement, product limit or unreleased hold point.
| Job stage | Hazards and effects | Failure factors | Required controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Plan plate and cut path | 1. Cut-piece fall2. Wrong plate cut3. Hazardous coating fumes4. Person struck below | 1. Final separation unreviewed2. Plate ID confused3. Coating unknown4. Lower work uncoordinated | 1. Review both resulting pieces2. Match plate and cutting layout3. Identify metal and coating4. Coordinate lower exclusion | 1. Plate and cut-piece IDs2. Cut path and final support3. Material and coating evidence4. Lower-area work boundary | ||||
| 2. Set support and shielding | 1. Plate movement crush2. Fire from sparks3. Cable insulation damage4. Nearby arc-eye injury | 1. Support inadequate2. Combustibles below table3. Lead touches hot edge4. Screens incomplete | 1. Secure suitable supports2. Remove or protect combustibles3. Protect lead and hose routes4. Control radiation and access | 1. Support and restraint2. Spark-reach inspection3. Cable and hose routing4. Screens and required PPE | ||||
| 3. Inspect supply and gas | 1. Electrical shock2. Stored-charge injury3. Hose release4. Wrong gas operation | 1. Torch insulation damaged2. Servicing scope confused3. Connection defective4. Gas specification ignored | 1. Inspect torch and leads2. Define isolation and authority3. Check hoses and connections4. Use specified gas conditions | 1. Supply earth and insulation2. Work-return connection3. Service and energy boundary4. Gas hose and filter condition | ||||
| 4. Verify separation support | 1. Cut piece drops2. Retained plate tips3. Molten-metal impact4. Return path interrupted | 1. Support outside final piece2. Sequence not reviewed3. Person below cut4. Clamp on falling piece | 1. Support each resulting piece2. Confirm final cutting sequence3. Exclude below and drop area4. Keep approved return path | 1. Piece weight and support2. Retained-plate stability3. Drop zone and removal method4. Return clamp placement | ||||
| 5. Cut and monitor | 1. Fume inhalation2. Arc-radiation injury3. Fire development4. Hot-torch contact | 1. Extraction fails2. Protection unsuitable3. Sparks reach combustibles4. Nozzle adjusted while active | 1. Maintain specified extraction2. Use correct radiation protection3. Watch exposed areas4. Stop before torch adjustment | 1. Extraction and air conditions2. Screens and filter selection3. Sparks and combustibles4. Settings and cut condition | ||||
| 6. Service and clear pieces | 1. Stored-energy shock2. Gas-pressure release3. Hot-consumable burn4. Sharp-edge cut | 1. Switch off used alone2. Residual gas ignored3. Cooling skipped4. Piece stored unstably | 1. Apply permitted service procedure2. Control supply and residual energy3. Confirm safe handling condition4. Remove pieces by planned method | 1. Isolation and service authority2. Gas and cooling condition3. Compatible consumables4. Stable removed-piece storage | ||||
| 7. Hold and restore controls | 1. Unsupported piece falls2. Damaged torch reused3. Continued fume exposure4. Shock during rework | 1. Support change ignored2. Unstable arc forced3. Extraction not restored4. Stop confused with isolation | 1. Hold affected cutting path2. Inspect isolated equipment3. Restore fume and fire controls4. Review support and return again | 1. Support and affected section2. Torch consumables and return3. Control restoration evidence4. Safe restart authorization | ||||
| 8. Inspect and hand over | 1. Hot-piece burn2. Edge laceration3. Uninspected part used4. Smoldering fire spreads | 1. Heat not identified2. Storage unstable3. Part identity lost4. Post-work watch incomplete | 1. Mark hot and sharp material2. Use stable storage3. Link part and inspection record4. Complete required fire closure | 1. Heat and access restrictions2. Storage and removal condition3. Part inspection and open defects4. Fire-watch closure record |
4. Hypothetical scenario and failure mechanisms
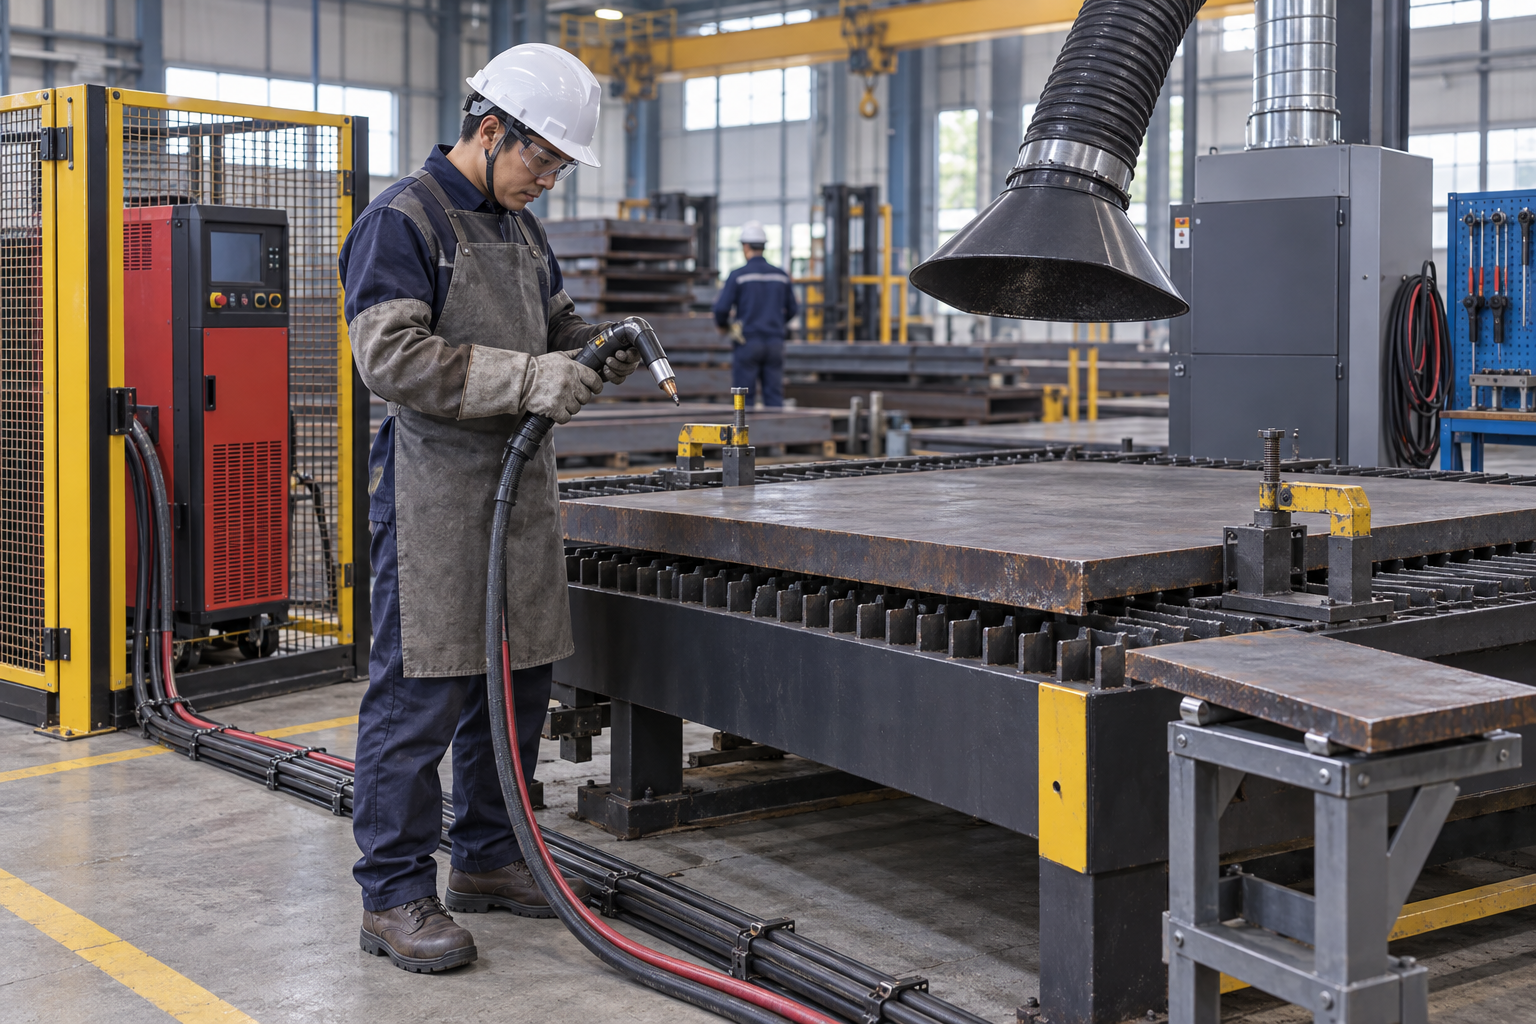 Retained source illustration: an AI-generated educational concept, not a real incident photograph or evidence of equipment suitability.
The following scenario, comparisons and example records are hypothetical teaching material. They do not reproduce actual incidents, measurements, signatures or approvals.
| Item | Hypothetical situation |
|---|---|
| Initial state | A supported steel plate is being cut into smaller pieces. |
| Change | The final connecting strip will be severed while the cut piece has no independent stable support. |
| Failure path | The crew treats the stability of the still-connected plate as proof of stability after separation. |
| Possible harm | The piece can tip or fall, exposing workers to impact, sharp edges, hot metal and cable damage. |
| Barrier | Hold the final cut, review both pieces, return connection and removal sequence, and confirm support and the exclusion area before continuing. |
The last cut changes the load path. Assess the retained plate and separated piece individually, including center of gravity, support contact and the removal method. A worker must not catch or steady a falling hot cut piece by hand.
The work-return lead completes the cutting circuit; protective grounding has a different safety function. Maintain the specified return connection on the retained work or approved cutting table. Do not attach it to a piece that will fall away.
Torch consumable replacement and internal power-supply maintenance are different scopes. Trigger release alone is not safe servicing. Follow model-specific disconnection, torch safety, gas and cooling instructions; internal stored-charge work belongs to appropriately qualified personnel.
Fume and fire controls must follow the actual steel, coating and surroundings. Screen nearby people from arc radiation without defeating ventilation. Inspect below and on the opposite side for spark travel and heat conduction, and maintain the required post-work fire watch.
| Decision | Reason and evidence |
|---|---|
| Known facts | The final connecting strip will be severed while the cut piece has no independent stable support. |
| Unresolved | The crew treats the stability of the still-connected plate as proof of stability after separation. |
| Hold reason | Stop for damaged torch or cables, unreliable work-return connection, failed fume controls, fire risk or changing plate support. Hold the final separating cut if either piece could tip, fall or interrupt the return path. |
| Evidence needed | Extraction and air conditions; Screens and filter selection; Sparks and combustibles; Settings and cut condition. |
| Next decision | Hold the final cut, review both pieces, return connection and removal sequence, and confirm support and the exclusion area before continuing. |
5. Conditional decisions and common errors
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Final support uncertain | Hold the separating cut. | Both pieces and removal load path. | Stable support and exclusion accepted. |
| Coating unknown | Hold affected cutting. | Material identity and exposure assessment. | Suitable controls defined. |
| Extraction stops | Stop cutting and restore controls. | Cause and operating performance. | Controls rechecked. |
| Torch requires internal repair | Isolate and refer qualified service. | Model procedure and service authority. | Required repair and verification complete. |
| Comparison | Situation A | Situation B |
|---|---|---|
| Plate stable before cut | Each resulting piece has accepted support after separation. | Only the connected plate was checked. |
| Torch trigger released | Required servicing isolation and cooling are verified. | Consumables are handled immediately. |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Confirm scope, task sequence, exclusion and stop authority. Coordinate plan plate and cut path with affected operations. |
| Technical reviewer | Resolve the actual design and equipment limits: Plate and cut-piece IDs; Cut path and final support; Material and coating evidence; Lower-area work boundary. |
| Work crew | Perform inspect supply and gas using the approved procedure; report any mismatch before proceeding. |
| Inspector / assessor | Verify Isolation and service authority; Gas and cooling condition; Compatible consumables; Stable removed-piece storage. Record what was actually checked and what remains unresolved. |
| Release / receiving authority | Confirm Heat and access restrictions; Storage and removal condition; Part inspection and open defects; Fire-watch closure record. Transfer restrictions and the next permitted stage. |
These are responsibility examples, not invented statutory credentials. Meet the actual training, competent-person, qualified-person and licensing requirements for the assigned work. Anyone may raise a hazard and request a stop; only the designated authority may release the affected stage after evidence is reviewed.
7. Hold points and record comparison
| Hold point | Evidence before release | Confirmation / approval |
|---|---|---|
| HP-0 Start | Scope, jurisdiction, equipment identity, responsible people and emergency arrangements. | |
| HP-1 Inspect supply and gas | Supply earth and insulation; Work-return connection; Service and energy boundary; Gas hose and filter condition | |
| HP-2 Verify separation support | Piece weight and support; Retained-plate stability; Drop zone and removal method; Return clamp placement | |
| HP-3 Hold and restore controls | Support and affected section; Torch consumables and return; Control restoration evidence; Safe restart authorization | |
| HP-4 Inspect and hand over | Heat and access restrictions; Storage and removal condition; Part inspection and open defects; Fire-watch closure record |
Hold points are internal evidence gates. They do not replace statutory permits or actual signatures. Recheck affected gates after a change, abnormal event or shift transfer. The blank record must identify the evidence, person, time, limits and release scope.
| Record | Insufficient record | Record checklist |
|---|---|---|
| Support | Extra stand added | □ Piece weight and support□ Retained-plate stability□ Drop zone and removal method□ Return clamp placement |
| Equipment | Power checked | □ Supply earth and insulation□ Work-return connection□ Service and energy boundary□ Gas hose and filter condition |
| Cutting | Cut looks good | □ Extraction and air conditions□ Screens and filter selection□ Sparks and combustibles□ Settings and cut condition |
| Transfer | Work finished | □ Heat and access restrictions□ Storage and removal condition□ Part inspection and open defects□ Fire-watch closure record |
The □ boxes are static prompts, not saved or interactive approvals. Each checks one record element. A tick alone does not establish suitability or permission to restart. Link equipment IDs and supporting records; retain unresolved matters and the earlier record when conditions change.
8. Site checklist and emergency response
| Check item | Result | Person / action |
|---|---|---|
| Plate and cut-piece IDs | ||
| Support and restraint | ||
| Supply earth and insulation | ||
| Piece weight and support | ||
| Extraction and air conditions | ||
| Isolation and service authority | ||
| Support and affected section | ||
| Heat and access restrictions | ||
| Emergency arrangements and unresolved restrictions communicated |
Stop work: Stop for damaged torch or cables, unreliable work-return connection, failed fume controls, fire risk or changing plate support. Hold the final separating cut if either piece could tip, fall or interrupt the return path.
Emergency response: Stop cutting from a safe position, warn others and control access to unstable or hot pieces. Activate the fire alarm and call 911 for fire beyond the trained response capability or serious injury. Designated personnel may isolate electrical and gas supplies only from a safe location. Do not touch electrically exposed equipment or enter below an unstable plate to attempt rescue.
9. Sources and review limits
Official-source review date: October 14, 2026. The following review is limited to the public provisions or selected manufacturer material identified below. It does not establish that any authority approved this article or the actual installation.
- OSHA 1910.252: Selected fire authorization, fire watch, hot-metal warning and ventilation provisions; jurisdiction and actual cutting conditions matter.
- OSHA 1910.147: Applicable general-industry servicing energy controls; not an internal electrical repair instruction.
- Hypertherm handheld air-plasma overview: Manufacturer overview including retained work-return connection. It explicitly does not replace the actual operator manual. Model-specific settings and internal service procedures were not adopted.
- OSHA State Plans: jurisdiction and coverage overview; identify the actual state program before use.
Paid consensus standards and site-specific calculations, manuals, inspection records and product certificates were not independently obtained or verified unless specifically identified. Korean legal citations remain in the preserved Korean source as source history; they are not represented as US legal duties.
10. PDF guidance and FAQ
PDF A covers basic task controls; B examines technical failures; C focuses on supervision, evidence and handover. Each has six rows and three items per main cell. They are complementary extracts: apply all eight body stages and the applicable site procedure. An omitted stage is not permission to omit its controls. PDF HP-0 through HP-4 are worksheet labels; match the event, evidence and authority rather than assuming they match another permit by number.
P/S/R/A, actual measurements, confirmations and signatures remain blank. The PDFs are uncompleted reference worksheets, not issued work permits.
Content group ID: jsa-plasma-platecut
Is stable support before cutting enough?
No. Verify the retained plate and separated piece after the final connection is cut.
Can the work clamp go on the falling piece?
No. Keep the specified return connection on retained work or an approved table so separation does not break the intended path.
Can consumables be changed when the trigger is released?
Trigger release alone is insufficient. Apply the actual model disconnection, torch-safety, gas and cooling procedure.
Are painted plates treated like bare steel?
Identify coating and base-metal hazards and resolve the required exposure and fire controls before cutting.
Has a professional verified or approved this document?
No. This is AI-assisted reference material. Editorial and layout checks are not a physical inspection or professional technical approval. Obtain qualified professional review and required site approval before use.
11. Revision history and authorship
Reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and site approval are required before use.
This system has not physically inspected the equipment, structures, ground, atmosphere or worksite. The document does not replace legal advice, manufacturer procedures, engineering design, inspection certificates, qualification evidence, the site risk assessment or an actual work permit.
Before use, a suitably qualified and authorized person must review the actual equipment, loads, methods, protection, inspection and emergency arrangements and resolve open issues. Record the real reviewer, organization, qualifications, delegated authority, reviewed documents, date, signature, exclusions and conditions of approval separately.
| Date | Version | Change | Review status |
|---|---|---|---|
| 2026-09-20 | 1.0 | Korean source revision retained in the source snapshot. | Historical editorial status; not US professional approval. |
| 2026-09-23 | 1.1 | Korean source revision retained in the source snapshot. | Historical editorial status; not US professional approval. |
| 2026-10-14 | US 1.0 | US localization of the assigned Korean source; task reasoning, educational image and history retained; US scope and sources reviewed. | AI-assisted editorial work; professional approval not performed. |