Removing the chuck key prevents one ejection hazard. It does not verify jaw contact, permitted projection, support or cutting stability.
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
Stop conditions first
Stop for unverified workholding/support, loose tooling, missing guarding, abnormal vibration, stock movement, entanglement hazards or unexpected restart. Lower speed alone does not resolve an unknown cause.
1. US legal and technical basis
General-industry metalworking under applicable OSHA 1910.212 guarding and 1910.147 servicing energy control. Foreign technical guidance does not replace US requirements.
| Reference | Use and limit |
|---|---|
| OSHA 29 CFR 1910.212 | Selected general machine-guarding principles; no machine-specific design certification. |
| OSHA 29 CFR 1910.147 | Applicable servicing/adjustment energy-control scope and safe-state verification. |
| CCOHS Metalworking Machines - Lathes | Selected general precautions: secure work, remove key, avoid entanglement and measure/clean only after stopping. Foreign technical guidance; filing and numerical examples excluded. |
| OSHA State Plans | Federal baseline and State Plan coverage reviewed. Confirm the applicable state program and employer coverage; this edition does not establish nationwide compliance. |
Determine whether Federal OSHA or an applicable State Plan governs the employer and work. Standards incorporated into a regulation must be read in their legally applicable edition. Other NFPA/ANSI guidance and manufacturer instructions have distinct roles; they are not automatically federal law.
2. Scope and required inputs
Included
External turning of a short round metal bar within verified chuck, workholding, support and machine limits on a manual lathe; setup, cutting, stopped measurement and handover.
Separate assessment
Long bar projecting behind the spindle, eccentric stock, CNC, threading, parting, boring, rotating filing/sanding, chuck changes and heavy lifting require separate plans.
| Input | Evidence needed |
|---|---|
| Plan stock and cut | Material/dimensions; Drawing revision; Chuck/support limits; Part criteria |
| Inspect machine and zone | Guard/stop condition; Exclusion and shields; Floor/bed clear; Operator competence |
| Secure stock and clearance | Jaw/contact condition; Travel/clearance; Projection/support; Key/tool count |
| Clean and transfer | Cleanup/guard state; Power/key state; Part/setting record; Receiver and restrictions |
Selected public official provisions were checked on October 14, 2026. This is not a complete legal audit. No actual equipment manual, site measurements, engineering calculations, product certification or professional technical approval was supplied. Full paid NFPA/ANSI standards and state/local amendments were not reviewed. Check actual equipment, jurisdiction and project requirements before use.
Select task-appropriate eye, hand, foot, skin and hearing protection from the exposure assessment. Where respiratory protection is necessary, use the applicable respiratory-protection program; PPE does not replace isolation, guarding, support or ventilation.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Plan stock and cut | 1. Stock ejection2. Wrong material cut3. Unsupported projection4. Wrong finished part | 1. Limits unknown2. ID missing3. Support not assessed4. Drawing outdated | 1. Match stock and drawing2. Check material suitability3. Verify workholding limits4. Define inspection criteria | 1. Material/dimensions2. Drawing revision3. Chuck/support limits4. Part criteria | ||||
| 2. Inspect machine and zone | 1. Entanglement2. Flying chips3. Slip injury4. Delayed stop | 1. Guard defective2. People exposed3. Oil on floor4. Stop inaccessible | 1. Verify guards and controls2. Protect adjacent people3. Clear floor and bed4. Keep stop accessible | 1. Guard/stop condition2. Exclusion and shields3. Floor/bed clear4. Operator competence | ||||
| 3. Isolate and set tooling | 1. Unexpected rotation2. Hand cut3. Tool release4. Wrong cutting condition | 1. Power available2. Sharp tool mishandled3. Holder loose4. Settings improvised | 1. Control energy for setup2. Handle isolated edges safely3. Secure correct tooling4. Use documented settings | 1. Isolation state2. Tool/holder condition3. Fastening/support4. Speed/feed/depth basis | ||||
| 4. Secure stock and clearance | 1. Stock slips2. Chuck collision3. Support failure4. Key ejection | 1. Jaw contact poor2. Travel interferes3. Projection excessive4. Key left in chuck | 1. Verify effective jaw grip2. Check permitted clearances3. Apply specified support4. Remove key immediately | 1. Jaw/contact condition2. Travel/clearance3. Projection/support4. Key/tool count | ||||
| 5. Start and cut | 1. Entanglement2. Workpiece ejection3. Chip eye injury4. Tool failure | 1. Gloves/loose clothing2. Grip inadequate3. Shield missing4. Cut forced | 1. Remove entanglement items2. Use controlled first cut3. Retain guards/shields4. Stop abnormal behavior | 1. Clothing/hair/gloves2. Cutting response3. Guarded zone4. Tool/work stability | ||||
| 6. Stop and measure | 1. Coasting contact2. Restart during access3. Sharp-chip injury4. Hot-stock burn | 1. Switch-off assumed safe2. Control unsecured3. Hands clear chips4. Hot work touched | 1. Wait for full standstill2. Prevent restart for access3. Use chip-removal tools4. Assess handling temperature | 1. Actual standstill2. Access/energy state3. Chip-removal method4. Measurements/temperature | ||||
| 7. Hold faults and restart | 1. Repeated ejection2. Hidden chuck damage3. Symptom masked4. Defective part released | 1. Speed only reduced2. Inspection omitted3. Cause unrecorded4. Restart equals quality pass | 1. Keep fault hold2. Inspect isolated setup3. Verify cause and correction4. Inspect affected parts | 1. Fault/settings record2. Jaw/tool/support findings3. Corrected setup evidence4. Restart/part disposition | ||||
| 8. Clean and transfer | 1. Residual chips cut2. Unattended restart3. Wrong next setup4. Defect forgotten | 1. Chips left2. Power unsecured3. Settings not shared4. No handover | 1. Clean after safe stop2. Secure machine3. Transfer approved settings4. Record remaining defects | 1. Cleanup/guard state2. Power/key state3. Part/setting record4. Receiver and restrictions |
Actual risk assessments, measurements, checks, approvals and signatures have not been performed. Keep unverified fields blank and link the actual site records. P/S/R/A mean likelihood, severity, site-method risk and site-defined acceptance/authorization; a score cannot waive a required control.
4. Failure mechanisms and hypothetical case
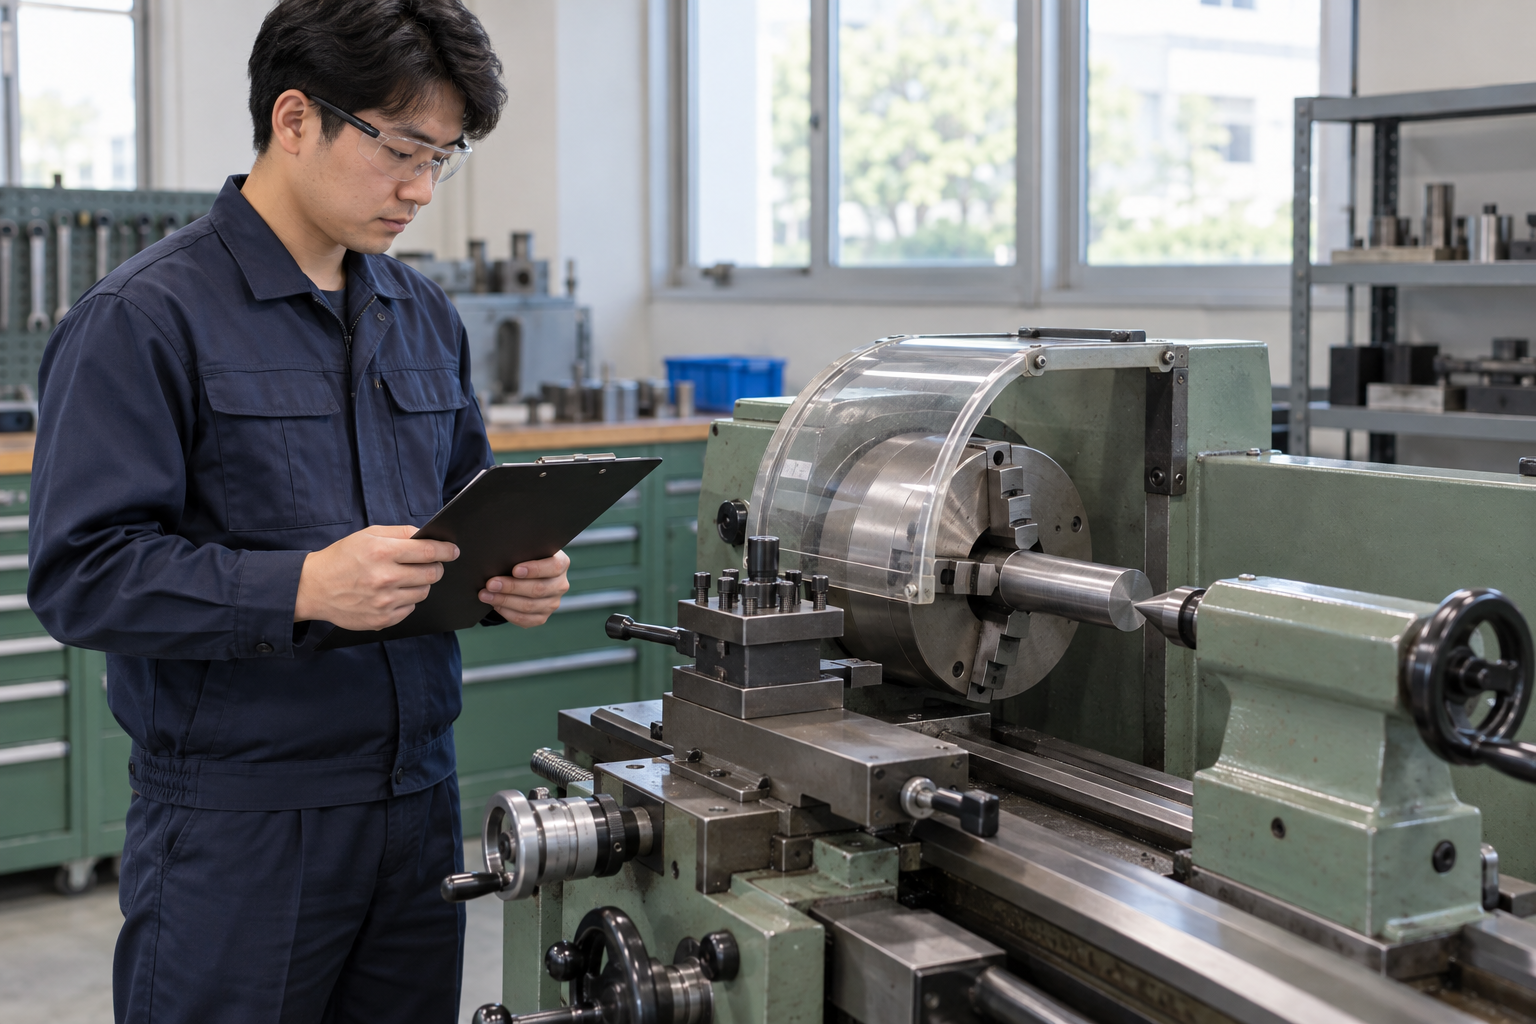
The retained illustration is an AI-generated educational image from the retained source edition. It is not an actual incident photograph, approved drawing, equipment certification or proof that the depicted arrangement is safe.
Effective workholding depends on jaw contact, chuck condition, stock projection and the cutting forces. No universal definition of short bar replaces actual component limits; do not force a poor setup by overtightening after vibration.
Keep gloves, jewelry, loose clothing and unsecured hair away during rotating operation. Hand protection for handling isolated sharp stock is a different phase. The general PPE paragraph must be applied consistently with this entanglement control.
A switched-off spindle may coast. Measure or remove chips only after complete stop and appropriate prevention of restart. Use a suitable brush, hook or other cleanup tool; never wrap a hand around chips or brake the chuck by hand.
A quiet no-load test does not prove stability under cut. Use documented material/tool/machine settings, observe the controlled first cut, and separate restart authorization from acceptance of previously machined parts.
Hypothetical decision example
Hypothetical example: vibration and repeated surface marks appear during the first cut. The key was removed but projection and jaw contact were not documented. The next operator proposes reducing speed. Maintain the hold until isolated inspection resolves workholding/tool condition and any affected workpiece is separately inspected.
The example is fictional; no incident, measurement, inspection or approval is asserted.
Task flow: Plan stock and cut → Inspect machine and zone → Isolate and set tooling → Secure stock and clearance → Start and cut → Stop and measure → Hold faults and restart → Clean and transfer
5. Hold and proceed decisions
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Vibration appears | Stop; inspect isolated setup | Jaw/tool/support findings | Cause corrected |
| Measurement needed | Stop fully; prevent restart | Standstill and access check | Safe access verified |
| Workholding unclear | Hold startup | Chuck/projection/support limits | Setup accepted |
| Part previously cut | Segregate for inspection | Dimensions/surface findings | Quality disposition complete |
Similar observation, different conclusion
| Observation | Supported conclusion | What remains unresolved |
|---|---|---|
| Chuck key removed | Loose key no longer present | Jaw/support suitability unresolved |
| Vibration decreases | Symptom changes | Cause and prior part quality unproved |
6. Roles and supervision
| Role | Responsibility |
|---|---|
| Work supervisor | Coordinate plan stock and cut, affected operations, stop signals and stage transitions. |
| Technical/equipment reviewer | Verify Material/dimensions, Drawing revision, actual instructions and unresolved technical limits. |
| Task crew | Apply the stated controls, report changes and keep actual checks and signatures factual. |
| Inspector/test lead | Connect Actual standstill, Access/energy state to the required acceptance criteria. |
| Receiving authority | Accept the recorded restrictions, Part/setting record, Receiver and restrictions, and follow-up ownership. |
These are responsibility examples, not invented statutory credentials. Verify actual competence, training and authority for the assigned work.
Supervision and handover controls
| Stage | Management controls | Evidence |
|---|---|---|
| Plan review | 1. Assign technical owner2. Close task-specific questions3. Match stock and drawing | 1. Material/dimensions2. Drawing revision3. Part criteria |
| Competence | 1. Verify required competence2. Assign stop authority3. Verify guards and controls | 1. Guard/stop condition2. Training and task briefing3. Operator competence |
| Prestart evidence | 1. Inspect actual equipment2. Link evidence to this stage3. Verify effective jaw grip | 1. Jaw/contact condition2. Travel/clearance3. Key/tool count |
| Change control | 1. Stop and secure the area2. Review affected controls3. Keep fault hold | 1. Fault/settings record2. Jaw/tool/support findings3. Restart/part disposition |
| Shift handover | 1. Identify remaining restrictions2. Confirm receiving responsibility3. Clean after safe stop | 1. Cleanup/guard state2. Power/key state3. Receiver and restrictions |
| Closeout | 1. Record defect disposition2. Archive factual evidence3. Clean after safe stop | 1. Cleanup/guard state2. Power/key state3. Receiver and restrictions |
7. Hold points and record quality
| Hold point | Evidence before release | Actual record |
|---|---|---|
| HP-0 Start | External turning of a short round metal bar within verified chuck, workholding, support and machine limits on a manual lathe; setup, cutting, stopped measurement and handover. | |
| HP-1 Inspect machine and zone | Guard/stop condition; Exclusion and shields; Floor/bed clear; Operator competence | |
| HP-2 Secure stock and clearance | Jaw/contact condition; Travel/clearance; Projection/support; Key/tool count | |
| HP-3 Hold faults and restart | Fault/settings record; Jaw/tool/support findings; Corrected setup evidence; Restart/part disposition | |
| HP-4 Clean and transfer | Cleanup/guard state; Power/key state; Part/setting record; Receiver and restrictions |
Hold points are internal evidence gates. They do not establish that a statutory permit exists or has been approved. Recheck affected gates after changes, faults and shift handover.
Record comparison - hypothetical templates
The 16 boxes below identify record elements, not completed checks or approvals. They are static symbols. Link equipment/location, date, actual findings and the separate record reference; preserve unresolved items.
| Record | Insufficient entry | Required record elements |
|---|---|---|
| Plan stock and cut | "Checked" without supporting facts | □ Material/dimensions□ Drawing revision□ Chuck/support limits□ Part criteria |
| Isolate and set tooling | "Checked" without supporting facts | □ Isolation state□ Tool/holder condition□ Fastening/support□ Speed/feed/depth basis |
| Start and cut | "Checked" without supporting facts | □ Clothing/hair/gloves□ Cutting response□ Guarded zone□ Tool/work stability |
| Hold faults and restart | "Checked" without supporting facts | □ Fault/settings record□ Jaw/tool/support findings□ Corrected setup evidence□ Restart/part disposition |
8. Pre-work checks and emergency response
| Check required | Result | Checker/action |
|---|---|---|
| Plan stock and cut: Material/dimensions | ||
| Inspect machine and zone: Guard/stop condition | ||
| Isolate and set tooling: Isolation state | ||
| Secure stock and clearance: Jaw/contact condition | ||
| Start and cut: Clothing/hair/gloves | ||
| Stop and measure: Actual standstill | ||
| Hold faults and restart: Fault/settings record | ||
| Clean and transfer: Cleanup/guard state |
Stop work
Stop for unverified workholding/support, loose tooling, missing guarding, abnormal vibration, stock movement, entanglement hazards or unexpected restart. Lower speed alone does not resolve an unknown cause.
Emergency response
Use the emergency stop from a safe position and prevent further motion. Do not pull a person or clothing against rotating parts or attempt to catch ejected stock. Clear the area and call 911 for serious injury. Trained responders must control energy and stored forces before release; preserve the faulted setup for investigation.
9. Official sources and review limits
Official public-source check: October 14, 2026. The review concerns the selected passages described below, not endorsement of this article.
| Official source | Checked scope and limit |
|---|---|
| OSHA 29 CFR 1910.212 | Selected general machine-guarding principles; no machine-specific design certification. |
| OSHA 29 CFR 1910.147 | Applicable servicing/adjustment energy-control scope and safe-state verification. |
| CCOHS Metalworking Machines - Lathes | Selected general precautions: secure work, remove key, avoid entanglement and measure/clean only after stopping. Foreign technical guidance; filing and numerical examples excluded. |
| OSHA State Plans | Federal baseline and State Plan coverage reviewed. Confirm the applicable state program and employer coverage; this edition does not establish nationwide compliance. |
Selected public official provisions were checked on October 14, 2026. This is not a complete legal audit. No actual equipment manual, site measurements, engineering calculations, product certification or professional technical approval was supplied. Full paid NFPA/ANSI standards and state/local amendments were not reviewed. Check actual equipment, jurisdiction and project requirements before use.
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
10. PDF use and frequently asked questions
PDF A summarizes core controls; B emphasizes technical failures; C covers supervision, records and handover. Each uses six stages from or aligned with the eight-stage body. All actual risk, measurement, check and signature fields are blank. Use a separate linked record where more space is needed.
Are gloves required during turning?
Do not wear gloves near rotating work; use phase-specific protection when handling isolated sharp stock.
May a caliper touch slowly rotating stock?
No. Wait for complete stop and control restart before measurement.
Does a lower speed release a vibration hold?
Resolve the cause and verify the corrected setup before restarting.
Does restart approval accept the earlier parts?
No. Their dimensions, surface and any damage need separate disposition.
Has a professional approved this JSA?
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
11. Authorship and revision history
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
| Date/version | Editorial history | Technical approval |
|---|---|---|
| September 23, 2026 / Korean v1.0 | Korean source: initial article, evidence, hypothetical decisions and body/PDF editorial checks. | Professional technical approval not performed |
| October 14, 2026 / US v1.0 | US localization: Preserves vibration/reduced-speed case and separates key removal, workholding, restart and part quality. Explicit no-glove rotating phase and stopped measurement controls retained. | Not performed |
Source topic: https://smartjsabridge.com/ko/case-study/jsa-lathe-bar-turning
Content group: jsa-lathe-bar-turning