The plate-to-fixture connection and the fixture-to-table connection both need restraint. A heavy vise can rotate with its plate when the bit catches; vise mass is not a substitute for attachment. Keep the drill breakthrough path below the plate clear of hands and equipment.
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and site authorization are required before use.
Stop before starting
Stop for unverified restraint, any plate or vise movement, abnormal vibration, binding, broken tools, faulty guarding or stop controls. Reassess after repositioning, bit replacement and any changed condition.
1. Legal and technical scope
| Basis | Scope and limits |
|---|---|
| OSHA 1910.212 | General-industry machine guarding, chips and fixed-machine anchoring. |
| OSHA 1910.147 | Covered servicing and verified hazardous-energy control; construction excluded. |
This edition assumes general-industry work under 1910.212 and covered servicing under 1910.147. The actual machine, bit, material and fixture instructions establish permitted speed, feed and gripping conditions; no universal RPM or torque is invented. Construction and State Plan requirements need separate applicability review.
2. Scope and required inputs
Included work
Manual-feed drilling of a single identified metal plate on a securely installed drill press, using a suitable fixture. Recheck restraint at every repositioning and inspect holes after full stop and safe isolation.
Separate assessment
Magnetic/portable drills, field enlargement of installed structures, concrete anchors, hand polishing on rotating tools, round stock, stacks, special materials, CNC feed and tapping need separate plans. This is not design approval for a new hole.
| Required input | Evidence to obtain |
|---|---|
| Identify plate and hole | Plate identity; Drawing and hole ID; Fixture grip area; Machine and bit limits |
| Inspect machine area | Cover and stop; Shield and eye PPE; Cable condition; Access boundary |
| Set up isolated | Isolation point; Bit grip and key; Speed basis; Table lock and clearance |
| Clamp plate and fixture | Plate-to-fixture grip; Fixture-to-table fixing; Plate support; Lower clearance |
No actual equipment model, SDS, site measurements, design calculations or authorization record was supplied. Product-specific limits and methods must be verified before use. Federal OSHA is a baseline within its scope; determine the applicable State Plan and local requirements. Manufacturer guidance is not government approval; an incorporated standard differs from voluntary guidance. No nationwide-compliance or expert-approval claim is made.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Technical and procedural controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Identify plate and hole | 1. Wrong material2. Unapproved hole3. Poor clamping4. Capacity exceeded | 1. Thickness unknown2. Drawing outdated3. Grip area absent4. Bit range unchecked | 1. Match plate and drawing2. Identify hole criteria3. Review fixture layout4. Check tool limits | 1. Plate identity2. Drawing and hole ID3. Fixture grip area4. Machine and bit limits | ||||
| 2. Inspect machine area | 1. Belt entanglement2. Chip eye injury3. Electric shock4. Bystander strike | 1. Cover open2. Shield absent3. Cable damaged4. Stock in walkway | 1. Check covers and stop2. Provide eye protection3. Inspect supply4. Separate stock projection | 1. Cover and stop2. Shield and eye PPE3. Cable condition4. Access boundary | ||||
| 3. Set up isolated | 1. Unexpected start2. Chuck-key ejection3. Bit breakage4. Table drop | 1. Stop only2. Key left in chuck3. Wrong speed4. Height lock loose | 1. Isolate and verify2. Remove chuck key3. Match bit and speed4. Lock adjusted table | 1. Isolation point2. Bit grip and key3. Speed basis4. Table lock and clearance | ||||
| 4. Clamp plate and fixture | 1. Plate rotation2. Vise rotation3. Plate lift4. Breakthrough puncture | 1. Hand-held plate2. Vise unsecured3. Thin plate unsupported4. Hand below hole | 1. Clamp plate in fixture2. Secure fixture to table3. Support plate properly4. Clear breakthrough path | 1. Plate-to-fixture grip2. Fixture-to-table fixing3. Plate support4. Lower clearance | ||||
| 5. Drill and monitor | 1. Entanglement2. Plate lift3. Bit catch4. Hot chip injury | 1. Loose glove or sleeve2. Excessive feed3. Movement ignored4. Live chip clearing | 1. Keep rotation zone clear2. Follow breakthrough feed3. Stop movement or binding4. Maintain chip shielding | 1. Hair and clothing2. Feed and support3. Noise and movement4. Chip and lubricant control | ||||
| 6. Stop clean inspect | 1. Coastdown contact2. Chip and burr cuts3. Unexpected restart4. Bad hole released | 1. Hand braking2. Barehand chip pickup3. Isolation omitted4. Visual check only | 1. Wait without touching2. Use chip tools3. Prevent restart4. Inspect hole criteria | 1. Full stop and isolation2. Chip tools and heat3. Restart prevention4. Hole and burr results | ||||
| 7. Hold binding or change | 1. Plate swing2. Broken bit release3. Repeat failure4. Shift restart | 1. Powered freeing2. Forced fragment removal3. Bit alone replaced4. Hold not transferred | 1. Stop and preserve fault2. Use designated recovery3. Review entire setup4. Verify before restart | 1. Fault and hole ID2. Isolation and fragments3. Corrected setup4. Restart authorization | ||||
| 8. Close and hand over | 1. Bad part mixed in2. Sharp waste3. Defective reuse4. Lost traceability | 1. No inspection marking2. Coolant left3. Hold tag removed4. Hole ID missing | 1. Separate accepted parts2. Collect chips and fluid3. Hold damaged equipment4. Transfer unresolved work | 1. Plate and hole status2. Floor and tools3. Guard and safe state4. Recipient and restrictions |
P = likelihood; S = severity; R = risk under the site method; A = site-defined acceptance/authorization. These actual assessment cells are blank. A low score never overrides a missing safeguard or a legal or manufacturer restriction.
4. Fictional scenario and failure mechanisms
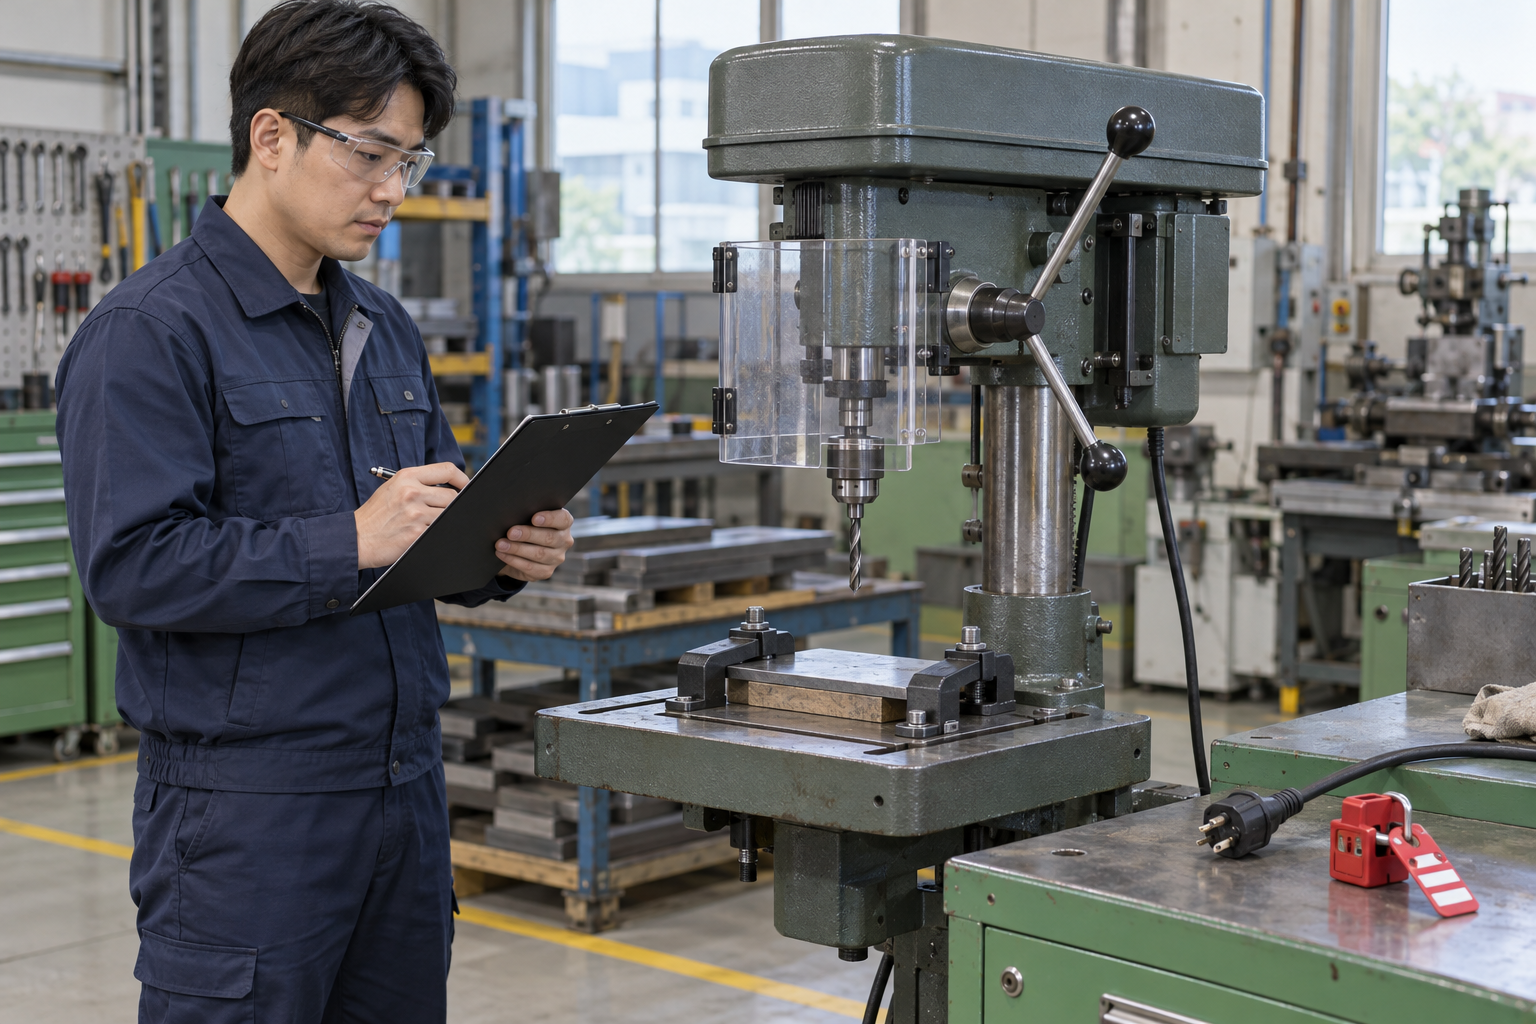
This illustration provides educational context. It is not an actual incident photograph or evidence of equipment suitability; any AI-generated depiction is illustrative only.
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Stage | Fictional situation |
|---|---|
| Initial situation | A fictional worker drills a thin plate held in a small vise. |
| Changed condition | The vise is not attached to the table. |
| Failure path | At breakthrough the bit catches and turns the plate and vise together. |
| Possible outcome | The swinging assembly could strike or cut the operator. |
| Prevention barrier | Do not grab it; stop, isolate, preserve the fault information and redesign the complete restraint and breakthrough clearance before release. |
Failure mechanisms
The plate-to-fixture connection and the fixture-to-table connection both need restraint. A heavy vise can rotate with its plate when the bit catches; vise mass is not a substitute for attachment. Keep the drill breakthrough path below the plate clear of hands and equipment.
A stopped switch does not prove a stopped spindle. Never brake the chuck by hand. Secure hair, sleeves and jewelry and remove gloves before operating near exposed rotation; use suitable gloves only for safe, isolated handling of sharp stock or chips.
A new bit running smoothly without a load does not validate clamping. After binding, isolate and inspect the bit, fixture, plate and affected hole. Replacing the bit alone does not resolve a moving fixture or an unsuitable feed condition.
Work sequence: Identify plate and hole → Inspect machine area → Set up isolated → Clamp plate and fixture → Drill and monitor → Stop clean inspect → Hold binding or change → Close and hand over. This is a teaching flow, not a device drawing or a complete operating procedure.
5. Conditional decisions and common errors
| Situation | Required action | Evidence | Proceed when |
|---|---|---|---|
| Vise or plate moves | Stop without grabbing | Both restraint connections | Setup corrected |
| Bit binds or breaks | Isolate and inspect | Bit, hole and fixture condition | Cause resolved |
| Plate repositioned | Repeat clamp check | Hole ID and clearance | Setup accepted |
| Hole complete | Inspect before release | Location, size, burr and distortion | Disposition recorded |
Similar observations, different decisions
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Observation | Insufficient conclusion | Required distinction |
|---|---|---|
| Plate clamped | Plate held to vise | Vise may still rotate |
| Switch off | Stop command | Coastdown still possible |
| New bit fitted | Tool replaced | Fixture fault may remain |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Confirm plate identity and the task scope, resources, interfaces and stop authority. |
| Qualified technical reviewer | Review cover and stop, model limits, compatibility and unresolved technical conditions within assigned competence. |
| Work crew | Apply the listed controls, report changes and stop when evidence or safeguards are missing. |
| Inspector / assessor | Record actual hair and clothing and other relevant checks; do not mark unverified conditions as accepted. |
| Handover authority | Reconcile plate and hole status, restrictions and outstanding actions before the next task. Role labels do not establish a legal credential. |
Supervision and handover focus
| Stage | Management action | Evidence |
|---|---|---|
| Identify plate and hole | 1. Record plate identity2. Record drawing and hole id3. Record fixture grip area | 1. Plate identity2. Drawing and hole ID3. Fixture grip area |
| Inspect machine area | 1. Record cover and stop2. Record shield and eye ppe3. Record cable condition | 1. Cover and stop2. Shield and eye PPE3. Cable condition |
| Clamp plate and fixture | 1. Record plate-to-fixture grip2. Record fixture-to-table fixing3. Record plate support | 1. Plate-to-fixture grip2. Fixture-to-table fixing3. Plate support |
| Drill and monitor | 1. Record hair and clothing2. Record feed and support3. Record noise and movement | 1. Hair and clothing2. Feed and support3. Noise and movement |
| Hold binding or change | 1. Record fault and hole id2. Record isolation and fragments3. Record corrected setup | 1. Fault and hole ID2. Isolation and fragments3. Corrected setup |
| Close and hand over | 1. Record plate and hole status2. Record floor and tools3. Record guard and safe state | 1. Plate and hole status2. Floor and tools3. Guard and safe state |
7. Hold points and record comparison
| Hold point | Evidence before release | Actual approval |
|---|---|---|
| HP-0 Scope | Manual-feed drilling of a single identified metal plate on a securely installed drill press, using a suitable fixture. Recheck restraint at every repositioning and inspect holes after full stop and safe isolation. | |
| HP-1 Inspect machine area | Cover and stop; Shield and eye PPE; Cable condition; Access boundary | |
| HP-2 Clamp plate and fixture | Plate-to-fixture grip; Fixture-to-table fixing; Plate support; Lower clearance | |
| HP-3 Hold binding or change | Fault and hole ID; Isolation and fragments; Corrected setup; Restart authorization | |
| HP-4 Close and hand over | Plate and hole status; Floor and tools; Guard and safe state; Recipient and restrictions |
Hold points are internal project checks. They are not universal statutory permits and do not grant work permission. Reassess after defects, changed conditions and shift changes.
Record comparison
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
The boxes are static record prompts, not interactive or saved approvals. A tick does not establish suitability or permission to restart. Record the evidence, person, time and unresolved issues; retain the change history.
| Record | Insufficient record | Record checklist |
|---|---|---|
| Identify plate and hole | Only marked “OK” | □ Plate identity□ Drawing and hole ID□ Fixture grip area□ Machine and bit limits |
| Clamp plate and fixture | Only marked “OK” | □ Plate-to-fixture grip□ Fixture-to-table fixing□ Plate support□ Lower clearance |
| Hold binding or change | Only marked “OK” | □ Fault and hole ID□ Isolation and fragments□ Corrected setup□ Restart authorization |
| Close and hand over | Only marked “OK” | □ Plate and hole status□ Floor and tools□ Guard and safe state□ Recipient and restrictions |
8. Site checklist and emergency response
| Site check | Actual result | Person / action |
|---|---|---|
| Identify plate and hole: Plate identity; Drawing and hole ID; Fixture grip area; Machine and bit limits | ||
| Inspect machine area: Cover and stop; Shield and eye PPE; Cable condition; Access boundary | ||
| Set up isolated: Isolation point; Bit grip and key; Speed basis; Table lock and clearance | ||
| Clamp plate and fixture: Plate-to-fixture grip; Fixture-to-table fixing; Plate support; Lower clearance | ||
| Drill and monitor: Hair and clothing; Feed and support; Noise and movement; Chip and lubricant control | ||
| Stop clean inspect: Full stop and isolation; Chip tools and heat; Restart prevention; Hole and burr results | ||
| Hold binding or change: Fault and hole ID; Isolation and fragments; Corrected setup; Restart authorization | ||
| Close and hand over: Plate and hole status; Floor and tools; Guard and safe state; Recipient and restrictions |
Stop work
Stop for unverified restraint, any plate or vise movement, abnormal vibration, binding, broken tools, faulty guarding or stop controls. Reassess after repositioning, bit replacement and any changed condition.
Emergency response
Use the accessible stop without grabbing rotating stock. Keep others clear; call the site emergency response and 911 for serious injury. Isolate before trained release or fragment recovery, preserving the affected plate and hole identification.
9. Sources and review limits
Public-source access/review: 2026-10-12.
| Official source | Reviewed scope and limits |
|---|---|
| OSHA 1910.212 | General-industry machine guarding, chips and fixed-machine anchoring. |
| OSHA 1910.147 | Covered servicing and verified hazardous-energy control; construction excluded. |
No actual equipment model, SDS, site measurements, design calculations or authorization record was supplied. Product-specific limits and methods must be verified before use. Federal OSHA is a baseline within its scope; determine the applicable State Plan and local requirements. Manufacturer guidance is not government approval; an incorporated standard differs from voluntary guidance. No nationwide-compliance or expert-approval claim is made.
10. PDF guidance and FAQ
PDF A covers basic task controls; B focuses on technical failures; C covers supervision, records and handover. P/S/R/A, measurements, confirmations and signatures remain blank for actual site assessment.
PDFs are complementary six-stage extracts. Apply all eight body stages and the actual equipment/site procedure.
Can the plate be held by hand at low speed?
No. Reduced speed does not establish a safe restraint arrangement.
Can gloves be worn beside the rotating chuck?
Keep gloves and loose clothing away from exposed rotation. Handle sharp stock only after the safe stopped/isolated condition is established.
When can chips be removed?
After full stop and safe isolation, using suitable tools rather than hands.
Has a professional verified or approved this document?
No. Public sources and editorial, layout and consistency checks were reviewed using AI. No site inspection or professional technical approval has been performed. Obtain appropriate professional review before use.
11. Revision history and authorship
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and site authorization are required before use.
| Date | Version | Change | Review status |
|---|---|---|---|
| 2026-10-12 | US 1.0 | New US edition from assigned Korean source; task decisions, records and PDFs localized. | AI editorial review; no professional technical approval |
Korean edition revision dates: 2026-03-02, 2026-08-01, 2026-09-23. US v1.0 adapts the earlier edition to United States requirements and terminology.
Site reviewers must add their actual qualifications, scope, date and approval only after the review occurs.