A closing kerf can pinch the cutting wheel and drive the tool back toward the operator. Support the parent stock and offcut, confirm the wheel-and-guard combination, and control the entire spark path.
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
Stop conditions first
Stop for unknown wheel rating or guard compatibility, damage, unusual vibration, narrowing kerf, moving support or uncontrolled sparks. Never restart in a bound cut or pull a rotating wheel free.
1. US legal and technical basis
Apply 1910.243(c) in general industry or 1926.303 for construction abrasive-wheel work, with the applicable PPE, fire and exposure provisions. Select the governing sector before approving the job. Korean minimum trial-run times are not presented as US requirements.
| Reference | Use and limit |
|---|---|
| OSHA 29 CFR 1910.243 | Portable abrasive-wheel guards, mounting inspection, speed compatibility and wheel fit; general industry. |
| OSHA 29 CFR 1926.303 | Construction abrasive-wheel guarding, inspection/ring-testing and incorporated B7.1-1970 provisions; the full incorporated standard was not independently read. |
| OSHA State Plans | Federal baseline and State Plan coverage reviewed. Confirm the applicable state program and employer coverage; this edition does not establish nationwide compliance. |
Determine whether Federal OSHA or an applicable State Plan governs the employer and work. Standards incorporated into a regulation must be read in their legally applicable edition. Other NFPA/ANSI guidance and manufacturer instructions have distinct roles; they are not automatically federal law.
2. Scope and required inputs
Included
Dry cutting ordinary metal stock secured on a ground-level workbench with a manufacturer-permitted bonded cutting wheel and compatible cutting guard.
Separate assessment
Weld grinding, masonry, wood saw blades, live pressurized pipe, unidentified tanks, explosive atmospheres, confined spaces, overhead work and structural demolition are outside this scope.
| Input | Evidence needed |
|---|---|
| Confirm stock | Material identification; Coating or residue data; Cut layout; Scope exclusions |
| Match wheel | Tool and wheel markings; Supply condition; Isolation state; Guard and flange match |
| Mount and test | Inspection/test method; Mounting instructions; Guard position; Vibration and clearance |
| Close and hand over | Spark-reach inspection; Defect record; Cut-stock status; Fire-watch handover |
Selected public official provisions were checked on October 12, 2026. This is not a complete legal audit. No actual equipment manual, site measurements, engineering calculations, product certification or professional technical approval was supplied. Full paid NFPA/ANSI standards and state/local amendments were not reviewed. Check actual equipment, jurisdiction and project requirements before use.
Select task-appropriate eye, hand, foot, skin and hearing protection from the exposure assessment. Where respiratory protection is necessary, use the applicable respiratory-protection program; PPE does not replace isolation, guarding, support or ventilation.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Confirm stock | 1. Fire2. Toxic coating dust3. Falling offcut4. Unexpected contents | 1. Coating unknown2. Tank contents assumed3. Separation not planned4. Wrong material selected | 1. Identify metal and coating2. Exclude unknown containers3. Plan separated shapes4. Assess dust and fire | 1. Material identification2. Coating or residue data3. Cut layout4. Scope exclusions | ||||
| 2. Match wheel | 1. Wheel burst2. Electric shock3. Unexpected start4. Guard failure | 1. Speed rating too low2. Damaged lead3. Energy connected4. Wrong guard or flange | 1. Match speed and dimensions2. Inspect cord and switch3. Disconnect before fitting4. Use approved combination | 1. Tool and wheel markings2. Supply condition3. Isolation state4. Guard and flange match | ||||
| 3. Support and screen | 1. Kickback2. Offcut drop3. Spark burns4. Bystander injury | 1. Kerf support wrong2. Offcut unsupported3. Combustibles exposed4. Public enters plane | 1. Secure stock and offcut2. Plan movement after cut3. Control full spark reach4. Exclude nearby people | 1. Clamps and supports2. Offcut destination3. Fire-control survey4. Exclusion boundary | ||||
| 4. Mount and test | 1. Wheel release2. Burst fragments3. Loss of control4. Accidental contact | 1. Damaged wheel mounted2. Wrong tightening3. Trial omitted4. People in wheel plane | 1. Inspect and test as applicable2. Mount per actual instructions3. Fit handle and cutting guard4. Run protected trial | 1. Inspection/test method2. Mounting instructions3. Guard position4. Vibration and clearance | ||||
| 5. Make the cut | 1. Binding kickback2. Hot fragments3. Dust exposure4. Cord damage | 1. Wheel twisted2. Side pressure applied3. Extraction unsuitable4. Lead crosses cut | 1. Maintain two-hand control2. Avoid twisting and side load3. Observe kerf and supports4. Keep leads clear | 1. Grip and body position2. Kerf condition3. Spark and dust controls4. Cable routing | ||||
| 6. Stop and inspect | 1. Coasting contact2. Hot offcut burns3. Sharp-edge cuts4. Falling stock | 1. Tool set down running2. Offcut caught by hand3. Heat unmarked4. Clamp released early | 1. Wait for complete stop2. Place tool securely3. Keep hot stock supported4. Protect sharp edges | 1. Wheel stationary2. Tool disconnected3. Offcut temperature hazard4. Stock stability | ||||
| 7. Handle binding | 1. Restart kickback2. Wheel fracture3. Stock movement4. Unexpected start | 1. Trigger retried in cut2. Wheel forced free3. Support removed4. Power remains connected | 1. Stop and disconnect2. Stabilize stock first3. Inspect cause and damage4. Retest before new cut | 1. Binding location2. Revised support layout3. Wheel disposition4. Restart test record | ||||
| 8. Close and hand over | 1. Hidden fire2. Defect reused3. Cuts in handling4. Premature area release | 1. Spark reach unchecked2. Damaged wheel stored3. Burrs unmarked4. Watch ended early | 1. Inspect fire-risk locations2. Quarantine defects3. Mark hot or sharp parts4. Transfer required fire watch | 1. Spark-reach inspection2. Defect record3. Cut-stock status4. Fire-watch handover |
Actual risk assessments, measurements, checks, approvals and signatures have not been performed. Keep unverified fields blank and link the actual site records. P/S/R/A mean likelihood, severity, site-method risk and site-defined acceptance/authorization; a score cannot waive a required control.
4. Failure mechanisms and hypothetical case
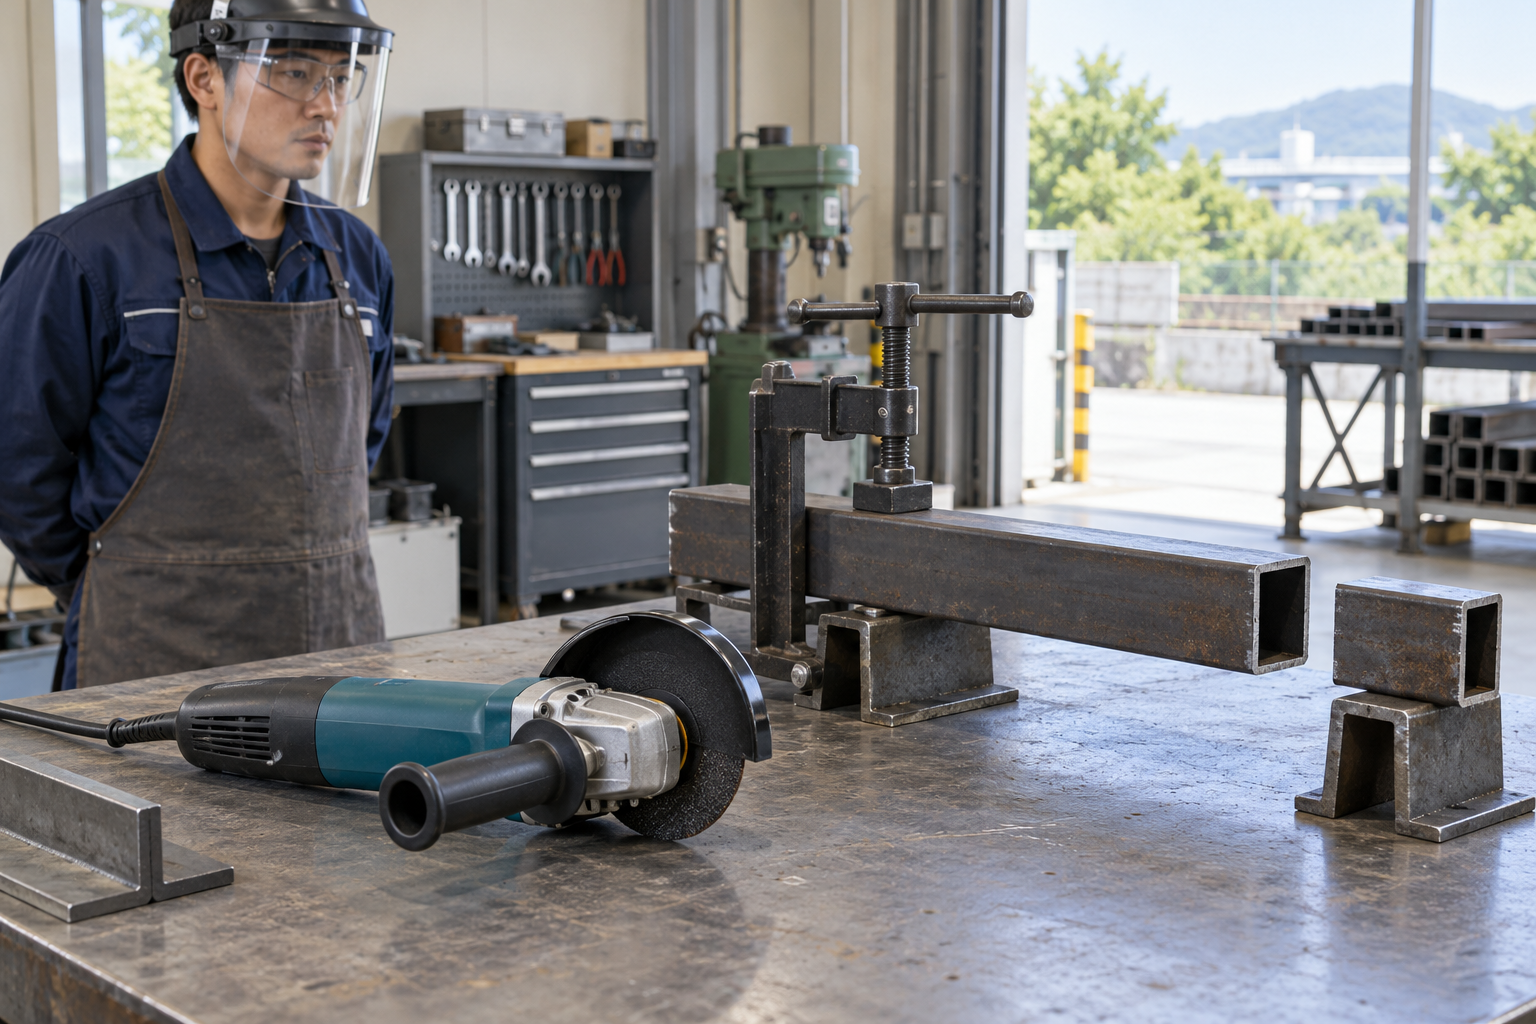
The retained illustration is an AI-generated educational image from the Korean source. It is not an actual incident photograph, approved drawing, equipment certification or proof that the depicted arrangement is safe.
A wheel fitting the spindle does not establish compatibility. Match intended material and cutting use, speed rating, diameter, thickness, mounting hardware and the cutting guard to the actual tool. Do not side-grind with a cutting wheel.
The cut changes the load path. Long stock and offcuts can sag or twist and close the kerf. Do not substitute a coworker holding the hot offcut for suitable mechanical support.
Inspection and the applicable wheel test must precede mounting. Sounding methods depend on wheel construction; resolve the appropriate method against the OSHA requirement and wheel supplier rather than assuming every bonded wheel makes a clear ring. Follow the actual manufacturer trial-run procedure from a protected position. The source Korean one/three-minute rule is not a US-wide rule.
Sparks can ignite material below, behind partitions or through gaps. Eye protection, appropriate face protection and exposure-based hearing/respiratory controls supplement the guard, support and fire prevention plan.
Hypothetical decision example
Hypothetical example: an overhanging tube sags, pinches the wheel and stops it. The operator proposes pressing the trigger while pulling backward; the correct hold is to isolate and stabilize before investigating.
The example is fictional; no incident, measurement, inspection or approval is asserted.
Task flow: Confirm stock → Match wheel → Support and screen → Mount and test → Make the cut → Stop and inspect → Handle binding → Close and hand over
5. Hold and proceed decisions
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Wheel mismatch | Remove from service pending matching | Tool, wheel, flange and guard data | Compatible combination |
| Kerf closes | Stop, isolate and stabilize stock | Support layout and wheel examination | Stable open cut path |
| Spark escape | Stop and extend fire controls | Reach area and combustible survey | Spark path controlled |
| After binding | Resolve cause and replace damaged parts | Inspection and protected trial record | Defect cleared and tested |
Similar observation, different conclusion
| Observation | Supported conclusion | What remains unresolved |
|---|---|---|
| Wheel fits | Ratings, use and guard all match | Spindle fit alone proves little |
| Switch released | Wheel stationary and stock secured | Coasting wheel and moving offcut remain |
6. Roles and supervision
| Role | Responsibility |
|---|---|
| Work supervisor | Coordinate confirm stock, affected operations, stop signals and stage transitions. |
| Technical/equipment reviewer | Verify Material identification, Coating or residue data, actual instructions and unresolved technical limits. |
| Task crew | Apply the stated controls, report changes and keep actual checks and signatures factual. |
| Inspector/test lead | Connect Wheel stationary, Tool disconnected to the required acceptance criteria. |
| Receiving authority | Accept the recorded restrictions, Cut-stock status, Fire-watch handover, and follow-up ownership. |
These are responsibility examples, not invented statutory credentials. Verify actual competence, training and authority for the assigned work.
Supervision and handover controls
| Stage | Management controls | Evidence |
|---|---|---|
| Plan review | 1. Assign technical owner2. Close task-specific questions3. Identify metal and coating | 1. Material identification2. Coating or residue data3. Scope exclusions |
| Competence | 1. Verify required competence2. Assign stop authority3. Match speed and dimensions | 1. Tool and wheel markings2. Training and task briefing3. Guard and flange match |
| Prestart evidence | 1. Inspect actual equipment2. Link evidence to this stage3. Inspect and test as applicable | 1. Inspection/test method2. Mounting instructions3. Vibration and clearance |
| Change control | 1. Stop and secure the area2. Review affected controls3. Stop and disconnect | 1. Binding location2. Revised support layout3. Restart test record |
| Shift handover | 1. Identify remaining restrictions2. Confirm receiving responsibility3. Inspect fire-risk locations | 1. Spark-reach inspection2. Defect record3. Fire-watch handover |
| Closeout | 1. Record defect disposition2. Archive factual evidence3. Inspect fire-risk locations | 1. Spark-reach inspection2. Defect record3. Fire-watch handover |
7. Hold points and record quality
| Hold point | Evidence before release | Actual record |
|---|---|---|
| HP-0 Start | Dry cutting ordinary metal stock secured on a ground-level workbench with a manufacturer-permitted bonded cutting wheel and compatible cutting guard. | |
| HP-1 Match wheel | Tool and wheel markings; Supply condition; Isolation state; Guard and flange match | |
| HP-2 Mount and test | Inspection/test method; Mounting instructions; Guard position; Vibration and clearance | |
| HP-3 Handle binding | Binding location; Revised support layout; Wheel disposition; Restart test record | |
| HP-4 Close and hand over | Spark-reach inspection; Defect record; Cut-stock status; Fire-watch handover |
Hold points are internal evidence gates. They do not establish that a statutory permit exists or has been approved. Recheck affected gates after changes, faults and shift handover.
Record comparison - hypothetical templates
The 16 boxes below identify record elements, not completed checks or approvals. They are static symbols. Link equipment/location, date, actual findings and the separate record reference; preserve unresolved items.
| Record | Insufficient entry | Required record elements |
|---|---|---|
| Confirm stock | "Checked" without supporting facts | □ Material identification□ Coating or residue data□ Cut layout□ Scope exclusions |
| Support and screen | "Checked" without supporting facts | □ Clamps and supports□ Offcut destination□ Fire-control survey□ Exclusion boundary |
| Make the cut | "Checked" without supporting facts | □ Grip and body position□ Kerf condition□ Spark and dust controls□ Cable routing |
| Handle binding | "Checked" without supporting facts | □ Binding location□ Revised support layout□ Wheel disposition□ Restart test record |
8. Pre-work checks and emergency response
| Check required | Result | Checker/action |
|---|---|---|
| Confirm stock: Material identification | ||
| Match wheel: Tool and wheel markings | ||
| Support and screen: Clamps and supports | ||
| Mount and test: Inspection/test method | ||
| Make the cut: Grip and body position | ||
| Stop and inspect: Wheel stationary | ||
| Handle binding: Binding location | ||
| Close and hand over: Spark-reach inspection |
Stop work
Stop for unknown wheel rating or guard compatibility, damage, unusual vibration, narrowing kerf, moving support or uncontrolled sparks. Never restart in a bound cut or pull a rotating wheel free.
Emergency response
Stop the grinder from a safe position and keep people clear of the wheel, flying fragments and unstable workpiece. Allow complete standstill and control power before access. For a fire, raise the alarm and evacuate; only trained personnel may attempt the site-authorized response when escape remains available. Call 911 for serious injury or uncontrolled fire and identify wheel fragments, hot metal and the electrical supply.
9. Official sources and review limits
Official public-source check: October 12, 2026. The review concerns the selected passages described below, not endorsement of this article.
| Official source | Checked scope and limit |
|---|---|
| OSHA 29 CFR 1910.243 | Portable abrasive-wheel guards, mounting inspection, speed compatibility and wheel fit; general industry. |
| OSHA 29 CFR 1926.303 | Construction abrasive-wheel guarding, inspection/ring-testing and incorporated B7.1-1970 provisions; the full incorporated standard was not independently read. |
| OSHA State Plans | Federal baseline and State Plan coverage reviewed. Confirm the applicable state program and employer coverage; this edition does not establish nationwide compliance. |
Selected public official provisions were checked on October 12, 2026. This is not a complete legal audit. No actual equipment manual, site measurements, engineering calculations, product certification or professional technical approval was supplied. Full paid NFPA/ANSI standards and state/local amendments were not reviewed. Check actual equipment, jurisdiction and project requirements before use.
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
10. PDF use and frequently asked questions
PDF A summarizes core controls; B emphasizes technical failures; C covers supervision, records and handover. Each uses six stages from or aligned with the eight-stage body. All actual risk, measurement, check and signature fields are blank. Use a separate linked record where more space is needed.
Can a grinding guard be used for cutting?
Use the guard/accessory combination specified for the actual cutting operation by the tool maker.
Can I grind burrs with the wheel side?
Not with a cutting wheel that is not designed for side grinding. Change to suitable equipment and reassess.
Is the Korean one/three-minute test mandatory in the US?
This edition does not adopt that foreign rule. Apply the governing US provisions and actual wheel/tool inspection and trial-run instructions.
What if the wheel binds?
Stop, disconnect energy and stabilize the stock before controlled recovery. Do not restart inside the cut.
Has a professional approved this JSA?
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
11. Authorship and revision history
This is reference content written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site authorization are necessary before use.
| Date/version | Editorial history | Technical approval |
|---|---|---|
| 2026-09-30 | Korean source retained as an unchanged snapshot; source ID 7813c46a-99ba-4ab2-a0b3-2b02059c0762 | Not asserted |
| 2026-10-12 / US v1.0 | US localization: Preserves the source kerf-closing case, separate weld-grinding scope, offcut support, cutting-guard match and hidden spark reach. Removes Korean trial-run timing as a US legal claim and distinguishes federal construction/general-industry requirements from manufacturer instructions. | Not performed |
Source topic: https://smartjsabridge.com/ko/case-study/jsa-angle-grinder-metal-cutting
Content group: jsa-angle-grinder-metal-cutting