Degreasing and oxide removal address different contamination. Confirm a suitable solvent and dryness before dedicated clean tooling; protect prepared joints and filler from recontamination.
This reference material was written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
Stop before proceeding
Stop if tool mixed, hood moved, electrode contacts. Keep the affected operation on hold until the listed evidence and proceed conditions are satisfied; a low risk score does not release missing safeguards.
1. Legal and technical scope
Apply 1910.252 to general-industry welding and applicable Part 1926 welding provisions, including 1926.352, to construction. Actual piping service, jurisdiction and project specifications determine welding qualifications and examination. Miller preparation guidance is technical advice, not a qualified WPS or legal approval; no universal current, balance or gas-flow value is supplied.
Confirm whether federal OSHA or an OSHA-approved State Plan covers this employer and worksite; state requirements and public-sector coverage can differ. Apply the task-specific provisions and limitations identified above.
| Basis | Application |
|---|---|
| OSHA 29 CFR 1910.252 | Applicable welding protection, ventilation and fire prevention. |
| OSHA 29 CFR 1926.352 | Construction fire prevention and watch. |
| Miller aluminum preparation | Degreasing before dedicated brushing, dry storage and avoiding chlorinated solvents; public article reviewed 2026-10-13. |
| OSHA State Plans | Official overview of federal and State Plan jurisdiction and differing public-sector coverage, checked 2026-10-13. Individual state rules require a site-specific check. |
2. Scope and required inputs
Included scope
Identify, isolate, prepare, AC TIG weld, cool and inspect aluminum pipe joints with traceable material, filler and approved welding procedure.
Separate assessment
Live or contaminated process lines, confined-space entry, other welding processes and pressure-test execution require separate plans.
| Input | Evidence needed |
|---|---|
| Identify joint | Pipe and isolation; Alloy and filler lot; WPS revision; Screen and contacts. |
| Clean joint | Residual contents; Clean dry surfaces; Solvent suitability; Material and WPS. |
| Weld joint | Screens and PPE; Current balance and gas; Fit and sequence; Electrode and weld. |
| Handoff | Temperature and marking; Supply and ventilation; Open-item closure; Joint repair history. |
No site measurements, equipment manuals for the actual installation, inspection records or signed technical approvals were supplied. Confirm the applicable requirements and actual product instructions before use; record each criterion with its units, source and equipment or work-area ID.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Technical and procedural controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Identify joint | 1. Residue fire2. Wrong alloy joint3. Bystander arc exposure4. Delayed gas response | 1. Isolation incomplete2. Filler mismatch3. Screen absent4. Roles unclear | 1. Verify pipe boundary2. Match alloy and WPS3. Plan screening4. Assign stop and response | 1. Pipe and isolation2. Alloy and filler lot3. WPS revision4. Screen and contacts | ||||
| 2. Prepare station | 1. Joint contamination2. Pipe rolls3. Cylinder falls4. Hose trip | 1. Tools mixed2. Support loose3. Cylinder unsecured4. Route cluttered | 1. Separate clean tools2. Secure pipe jig3. Secure correct cylinder4. Protect cables and hoses | 1. Tool cleanliness2. Pipe support3. Cylinder and regulator4. Clear escape route | ||||
| 3. Clean joint | 1. Residue ignition2. Porosity3. Toxic solvent gas4. Wrong preparation | 1. Oil retained2. Moisture remains3. Chlorinated cleaner4. Oxide not removed | 1. Confirm isolation and cleaning2. Degrease and dry3. Check solvent SDS4. Use dedicated clean brush | 1. Residual contents2. Clean dry surfaces3. Solvent suitability4. Material and WPS | ||||
| 4. Check power and gas | 1. Electric shock2. Oxygen depletion3. Gas leak4. Ozone exposure | 1. Insulation damaged2. Gas accumulates3. Connection defective4. Extraction ineffective | 1. Inspect torch and circuit2. Assess atmosphere3. Check gas connections4. Provide effective extraction | 1. Insulation and return2. Gas and air assessment3. Cylinder restraint4. Hood and shielding | ||||
| 5. Weld joint | 1. Arc injury2. Burn-through3. Distortion4. Tungsten inclusion | 1. Protection unsuitable2. Heat input wrong3. Support shifts4. Electrode contact ignored | 1. Use suitable arc protection2. Apply approved AC settings3. Maintain stable support4. Stop for electrode contact | 1. Screens and PPE2. Current balance and gas3. Fit and sequence4. Electrode and weld | ||||
| 6. Cool and inspect | 1. Residual heat burn2. Gas remains3. Defect released4. Repair contamination | 1. Color trusted2. Supply left open3. Inspection incomplete4. Recleaning skipped | 1. Mark hot material2. Shut down per manual3. Complete required examination4. Reclean before repair | 1. Temperature method2. Power and gas state3. Examination result4. Repair and retest | ||||
| 7. Resolve abnormality | 1. Fire2. Repeated defect3. Unexpected restart4. Exposure recurs | 1. Cause unknown2. Joint unmarked3. Conditions changed4. Ventilation unverified | 1. Stop affected welding2. Identify impacted joints3. Review changed conditions4. Verify before restart | 1. Stop condition2. Joint range3. Cause and correction4. Restart authority | ||||
| 8. Handoff | 1. Hot pipe contact2. Gas leakage3. Untested joint used4. Traceability lost | 1. Temperature unchecked2. Shutoff missed3. Appearance accepted4. Records separated | 1. Verify safe temperature2. Check shutdown state3. Close examination items4. Transfer joint records | 1. Temperature and marking2. Supply and ventilation3. Open-item closure4. Joint repair history |
P = likelihood; S = severity; R = risk under the site method; A = the site-defined acceptance/authorization decision. Complete only after actual assessment. Blank cells and checklist prompts are not completed inspections.
4. Fictional scenario and failure mechanisms
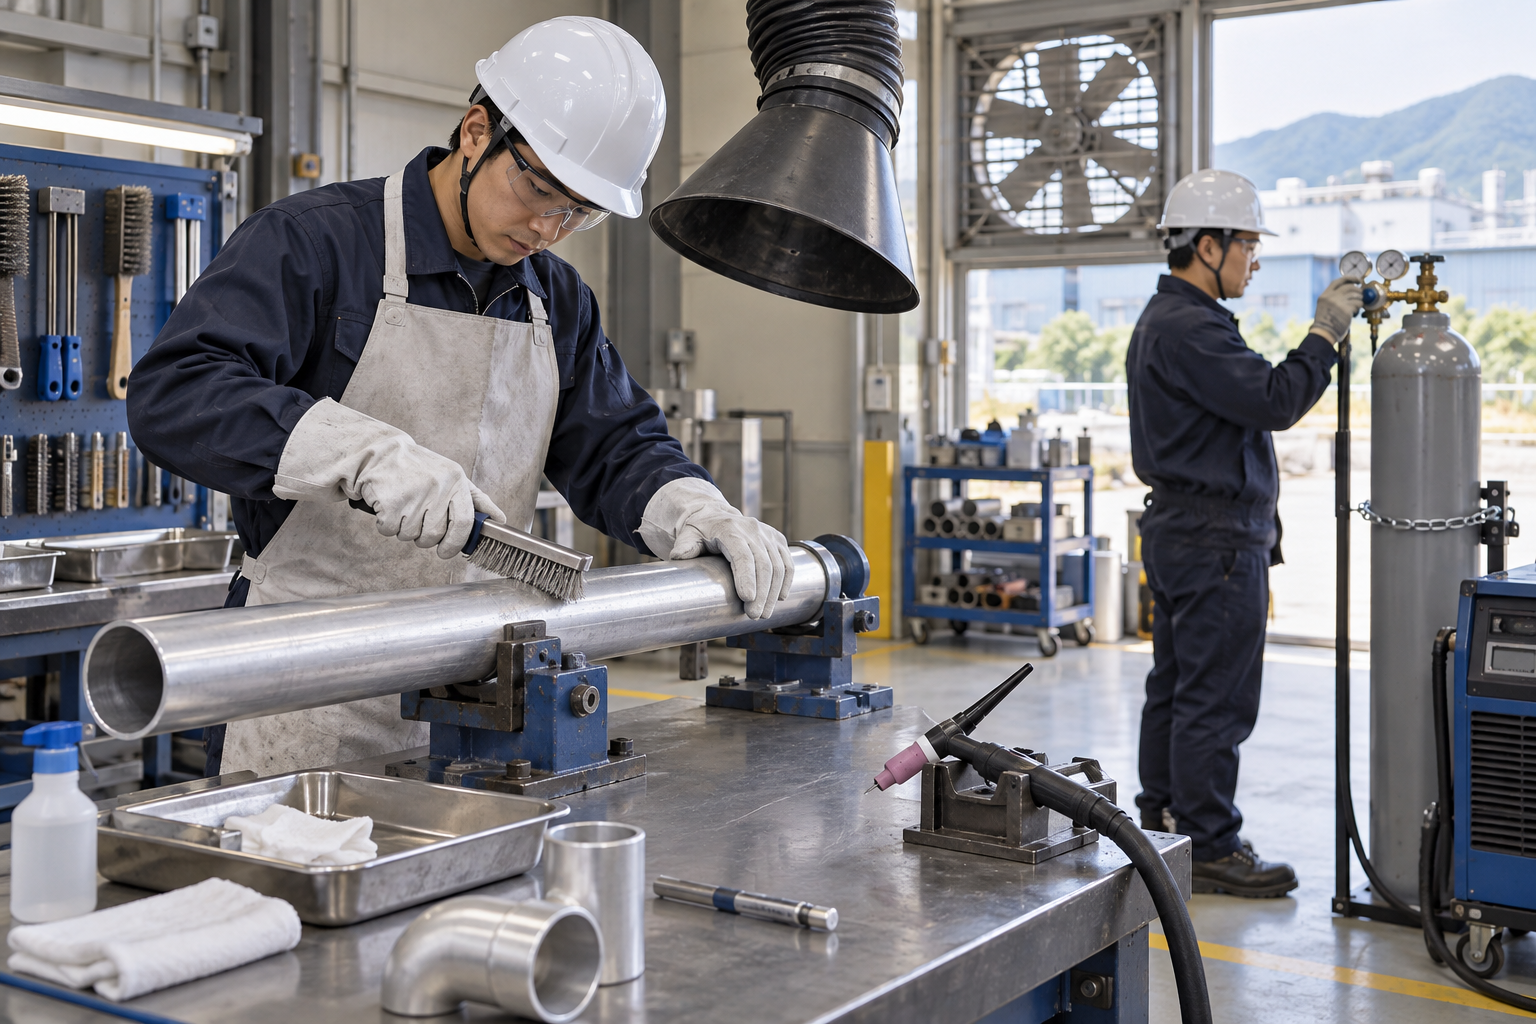
Retained AI-generated educational illustration from the source edition; not a real incident photograph, approved installation drawing or evidence of equipment suitability.
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Item | Fictional scenario |
|---|---|
| Initial | An isolated aluminum pipe joint is ready for preparation. |
| Change | A brush previously used on other material is substituted and drying is skipped. |
| Failure | Contamination remains despite a bright surface. |
| Outcome | Porosity or other defects may require examination and repair; appearance does not identify a single cause. |
| Barrier | Hold welding, restore clean dry preparation and connect affected joints to the approved inspection disposition. |
Why the controls matter
Degreasing and oxide removal address different contamination. Confirm a suitable solvent and dryness before dedicated clean tooling; protect prepared joints and filler from recontamination.
Little visible smoke does not establish clean air. Assess ozone and argon accumulation, while locating extraction so it does not defeat shielding. Neither a hood nor PPE alone proves control.
Aluminum color is not a cooling test. Use an appropriate temperature check and hot-material marking. Accept welds through the specified examination and repair process, linked to joint identity.
Decision sequence
| Step | Decision |
|---|---|
| Known | A brush previously used on other material is substituted and drying is skipped. |
| Unknown | Actual condition, extent of damage and suitability of screens and ppe, current balance and gas remain to be established. |
| Hold | Contamination remains despite a bright surface. |
| Evidence | Link screens and ppe, current balance and gas, fit and sequence, electrode and weld, stop condition, joint range to the affected equipment or work area. |
| Next | Hold welding, restore clean dry preparation and connect affected joints to the approved inspection disposition. |
5. Conditional decisions and common errors
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Tool mixed | Hold and reclean | Tool identity and dry surface | Preparation accepted |
| Hood moved | Recheck air and shielding | Extraction and gas condition | Both controls effective |
| Electrode contacts | Stop and mark joint | WPS and affected weld | Disposition accepted |
| Inspection incomplete | Hold service handoff | Joint and examination record | Open items closed |
Similar appearance, different evidence
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Comparison | Supported decision | Insufficient basis |
|---|---|---|
| Condition | Tool identity and dry surface | Tool mixed has not been resolved. |
| Evidence | WPS and affected weld | A photograph or a completed-looking task without the relevant inspection record. |
| Release | Open items closed | Completion of one step does not release the excluded tasks in section 2. |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Assign the task boundary, stop authority, interfaces and emergency communication for aluminum pipe ac tig welding. |
| Technical lead | Confirm Pipe and isolation; Alloy and filler lot; WPS revision; Screen and contacts. Resolve design and manufacturer limits before work. |
| Authorized crew | Apply Residual contents; Clean dry surfaces; Solvent suitability; Material and WPS. Stop when the working arrangement changes. |
| Inspector / receiving lead | Review Screens and PPE; Current balance and gas; Fit and sequence; Electrode and weld. Transfer Temperature and marking; Supply and ventilation; Open-item closure; Joint repair history. |
Role labels allocate responsibilities; they do not confer a legal qualification. Verify the competence, training and authority required for the actual task.
Record and handoff perspective
| Stage | Record controls | Verification |
|---|---|---|
| Identify joint | 1. Record pipe and isolation2. Record alloy and filler lot3. Record wps revision | 1. Alloy and filler lot2. WPS revision3. Screen and contacts |
| Clean joint | 1. Record residual contents2. Record clean dry surfaces3. Record solvent suitability | 1. Clean dry surfaces2. Solvent suitability3. Material and WPS |
| Check power and gas | 1. Record insulation and return2. Record gas and air assessment3. Record cylinder restraint | 1. Gas and air assessment2. Cylinder restraint3. Hood and shielding |
| Weld joint | 1. Record screens and ppe2. Record current balance and gas3. Record fit and sequence | 1. Current balance and gas2. Fit and sequence3. Electrode and weld |
| Resolve abnormality | 1. Record stop condition2. Record joint range3. Record cause and correction | 1. Joint range2. Cause and correction3. Restart authority |
| Handoff | 1. Record temperature and marking2. Record supply and ventilation3. Record open-item closure | 1. Supply and ventilation2. Open-item closure3. Joint repair history |
7. Hold points and record comparison
| Hold point | Evidence before release | Actual record |
|---|---|---|
| HP-0 Start | Identify, isolate, prepare, AC TIG weld, cool and inspect aluminum pipe joints with traceable material, filler and approved welding procedure. | |
| HP-1 Identify joint | Pipe and isolation; Alloy and filler lot; WPS revision; Screen and contacts | |
| HP-2 Clean joint | Residual contents; Clean dry surfaces; Solvent suitability; Material and WPS | |
| HP-3 Check power and gas | Insulation and return; Gas and air assessment; Cylinder restraint; Hood and shielding | |
| HP-4 Handoff | Temperature and marking; Supply and ventilation; Open-item closure; Joint repair history |
These are internal hold points, not issued permits. Recheck affected points after a change, fault or shift handoff; link the actual approval record.
Record comparison
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
The boxes are static record prompts, not interactive or saved approvals. A tick does not establish suitability or permission to restart. Record the evidence, person, time and unresolved issues; retain the change history.
| Record | Insufficient | Record checklist |
|---|---|---|
| Identify joint | "Checked" without target, criteria or result | □ Pipe and isolation□ Alloy and filler lot□ WPS revision□ Screen and contacts |
| Clean joint | "Checked" without target, criteria or result | □ Residual contents□ Clean dry surfaces□ Solvent suitability□ Material and WPS |
| Weld joint | "Checked" without target, criteria or result | □ Screens and PPE□ Current balance and gas□ Fit and sequence□ Electrode and weld |
| Handoff | "Checked" without target, criteria or result | □ Temperature and marking□ Supply and ventilation□ Open-item closure□ Joint repair history |
8. Site checklist and emergency response
| Check | Result | Person / action |
|---|---|---|
| □ Identify joint: Pipe and isolation | ||
| □ Prepare station: Tool cleanliness | ||
| □ Clean joint: Residual contents | ||
| □ Check power and gas: Insulation and return | ||
| □ Weld joint: Screens and PPE | ||
| □ Cool and inspect: Temperature method | ||
| □ Resolve abnormality: Stop condition | ||
| □ Handoff: Temperature and marking | ||
| □ Emergency access and handoff restrictions |
Stop work
Stop if tool mixed, hood moved, electrode contacts. Keep the affected operation on hold until the listed evidence and proceed conditions are satisfied; a low risk score does not release missing safeguards.
Emergency response
Stop from a safe location, exclude people from the affected danger zone and activate the site emergency plan. Call 911 for injury or immediate danger. Do not enter an unstable, energized or confined danger area for an improvised rescue; trained responders must control the specific energy and access hazards.
9. Sources and review limits
Public-source review: 2026-10-14. Official regulation pages and specific technical references are distinguished below; no agency or manufacturer has approved this content.
| Source | Reviewed scope and limitation |
|---|---|
| OSHA 29 CFR 1910.252 | Applicable welding protection, ventilation and fire prevention. |
| OSHA 29 CFR 1926.352 | Construction fire prevention and watch. |
| Miller aluminum preparation | Degreasing before dedicated brushing, dry storage and avoiding chlorinated solvents; public article reviewed 2026-10-13. |
| OSHA State Plans | Official overview of federal and State Plan jurisdiction and differing public-sector coverage, checked 2026-10-13. Individual state rules require a site-specific check. |
No site measurements, equipment manuals for the actual installation, inspection records or signed technical approvals were supplied. Confirm the applicable requirements and actual product instructions before use; record each criterion with its units, source and equipment or work-area ID.
10. PDF guidance and FAQ
PDF A covers basic task controls; B focuses on technical failures; C covers supervision, records and handover. The article has eight stages with four items per main cell; each PDF has six key stages with three items per main cell. P/S/R/A, measurements, confirmations and signatures remain blank for actual site assessment.
Content group
jsa-aluminum-actig
Is a dedicated brush enough?
No. Degrease, dry and prevent recontamination as well.
Does little smoke mean ventilation is unnecessary?
No. Assess ozone, shielding gas and actual exposure.
May color establish a cool pipe?
No. Use an appropriate temperature-check method.
Does a smooth bead prove acceptance?
No. Complete the specified examination and any repair and retest.
Has a professional approved this JSA?
This reference material was written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
11. Revision history and authorship
This reference material was written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
Korean source created 2026-09-20. This US edition adapts the Korean source; earlier editorial revisions do not constitute professional approval of this edition.
| Date | Edition | Change | Review status |
|---|---|---|---|
| 2026-09-20 | Korean source v1.0 | Source editorial publication or revision; retained as provenance of the Korean edition. | Editorial record only; no professional approval of this US edition. |
| 2026-09-22 | Korean source v1.1 | Source editorial publication or revision; retained as provenance of the Korean edition. | Editorial record only; no professional approval of this US edition. |
| 2026-10-12 | Korean source v1.2 | Source editorial publication or revision; retained as provenance of the Korean edition. | Editorial record only; no professional approval of this US edition. |
| 2026-10-14 | 1.0 | US localization: preserve task judgments; replace Korean legal applicability with scoped US references. | AI editorial and output checks; no professional technical approval. |