Flux identity, wire pairing and storage history matter even when granules look dry. An unmarked container cannot be accepted by appearance. Identify any joints already welded with uncertain material.
This reference material was written and reviced with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
Stop before proceeding
Stop if flux untraceable, rail condition unknown, feed adjustment needed. Keep the affected operation on hold until the listed evidence and proceed conditions are satisfied; a low risk score does not release missing safeguards.
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to applicable Singapore requirements, the actual equipment/site and approved safe work procedures.
1. Legal and technical scope
Assess the Singapore welding workstation as an integrated powered system: rail carriage, wire feed, welding head, fixture, power source and extraction. The competent welding and equipment leads must agree the automatic travel boundary and separate production welding from isolated setup, cleaning and maintenance.
| Basis | Singapore application |
|---|---|
| Risk management | The employer, self-employed person and principal assess and control work risks. Include preparation, abnormal conditions and maintenance. Coordinate affected trades and communicate controls. |
| Activity-specific guidance | Use machinery guidance for guards, travel and energy isolation, hot-work guidance for fire controls, chemical/GHS guidance for flux and fumes, and electrical guidance for competent defect correction. |
| Permits and authority | Select permit requirements for the actual sector and activity. Site hold points and contractor role labels do not create statutory permits or qualifications. |
| Equipment and design | No generic flux-baking temperature, current range, travel speed or recovery ratio is assigned. Actual WPS, flux SDS and carriage instructions were not supplied. Integrated positioners, altered automatic sequences, multiple-electrode conversions and internal repairs require separate review. Full welding and machinery standards were not read. |
2. Scope and required inputs
Included scope
Prepare plate, fixtures and rail carriage; control wire and flux identity; perform automatic submerged arc welding; then stop, isolate, cool, recover flux, inspect and hand over joints.
Separate assessment
Integrated positioners or roller beds, multielectrode changes, internal electrical repair and improvised regeneration of unidentified flux require separate review.
| Input | Evidence needed |
|---|---|
| Identify joint and WPS | Joint and base material; Wire flux and WPS; Fixture and fit; Fire and ventilation plan. |
| Prepare consumables | Flux lot and packaging; Storage and drying; Recovery permission; Wire and feed guard. |
| Run automatic weld | Operator and stop; Travel and heat; Fire and extraction; Joint conditions. |
| Close and handover | Temperature marking; Parking and power; Open-item disposition; Weld consumable history. |
No site measurements, equipment manuals for the actual installation, inspection records or signed technical approvals were supplied. Confirm the applicable requirements and actual product instructions before use; record each criterion with its units, source and equipment or work-area ID.
Singapore site planning
Verify the actual wire/flux combination and lot against the WPS and manufacturer storage, drying and permitted recovery instructions. Keep unidentified or contaminated recovered flux separate and trace any affected weld length before a technical disposition. Record current in A, travel speed in the specified SI units and any drying or preheat temperature in °C. Secure rails and stops, prevent crush access along the carriage path, manage lead slack and test stopping from a protected position. Control dust when handling flux, retain fume extraction and fire precautions even when the arc is covered, and isolate the drive/feed before intervention. Mark hot slag and workpieces and hand over weld examination and flux restrictions.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Technical and procedural controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Identify joint and WPS | 1. Wrong weld properties2. Joint moves3. Fire4. Untraceable weld | 1. Wire flux mismatch2. Fixture inadequate3. Fuel nearby4. Joint ID absent | 1. Match approved pairing2. Verify plate support3. Plan hot-work controls4. Identify weld intervals | 1. Joint and base material2. Wire flux and WPS3. Fixture and fit4. Fire and ventilation plan | ||||
| 2. Set rail carriage | 1. Carriage falls2. Pinch injury3. Cable pulls4. Unexpected travel | 1. Rail loose2. Access unguarded3. Cable too short4. Stop defective | 1. Secure rated rail support2. Control travel boundary3. Provide cable allowance4. Check travel stop functions | 1. Rail and end stops2. Carriage stability3. Cable path4. Stop and exclusion | ||||
| 3. Prepare consumables | 1. Dust exposure2. Defective weld3. Mixed flux4. Wire-feed injury | 1. SDS ignored2. Storage unknown3. Container unlabelled4. Feed accessed live | 1. Control handling dust2. Verify storage history3. Keep lots identified4. Isolate feed for access | 1. Flux lot and packaging2. Storage and drying3. Recovery permission4. Wire and feed guard | ||||
| 4. Check power and setup | 1. Electric shock2. Wrong heat input3. Unexpected feed4. Fume exposure | 1. Insulation damaged2. Polarity wrong3. Guard bypassed4. Extraction absent | 1. Inspect welding circuit2. Match approved settings3. Verify feed protection4. Check exposure controls | 1. Insulation and return2. Polarity, current/A, speed3. Feed guard4. Ventilation and PPE | ||||
| 5. Run automatic weld | 1. Carriage crush2. Hot-metal burn3. Fire4. Weld defect | 1. Person in travel path2. Flux hides heat3. Watch absent4. Conditions drift | 1. Keep travel area clear2. Mark hot work zone3. Maintain fire controls4. Monitor recorded settings | 1. Operator and stop2. Travel and heat3. Fire and extraction4. Joint conditions | ||||
| 6. Recover and inspect | 1. Hot slag burn2. Unexpected motion3. Flux contamination4. Defect hidden | 1. Cooling assumed2. Stop only trusted3. Recovered lots mixed4. Slag masks weld | 1. Isolate before access2. Verify cooling3. Separate recovered flux4. Perform specified examination | 1. Isolation and rest2. Temperature and slag3. Recovered flux status4. Joint inspection | ||||
| 7. Hold uncertain flux | 1. Repeat defect2. Affected joint lost3. Unsafe rework4. Unapproved restart | 1. New flux seen as cure2. Usage map absent3. Cause unreviewed4. History ignored | 1. Quarantine uncertain material2. Identify prior intervals3. Obtain technical disposition4. Release new work separately | 1. Container and lot2. Affected joint and weld length3. Examination and repair4. Restart authority | ||||
| 8. Close and handover | 1. Hot joint contact2. Carriage moves3. Unaccepted weld used4. Consumable history lost | 1. Heat unmarked2. Park unsecured3. Open defects4. Records separated | 1. Mark residual heat2. Secure carriage and power3. Close required examinations4. Transfer joint and lot records | 1. Temperature marking2. Parking and power3. Open-item disposition4. Weld consumable history |
P = likelihood; S = severity; R = risk using the site method; A = site acceptance/authorisation. Complete after actual assessment; no score overrides an unresolved hold point or equipment limit.
4. Fictional scenario and failure mechanisms
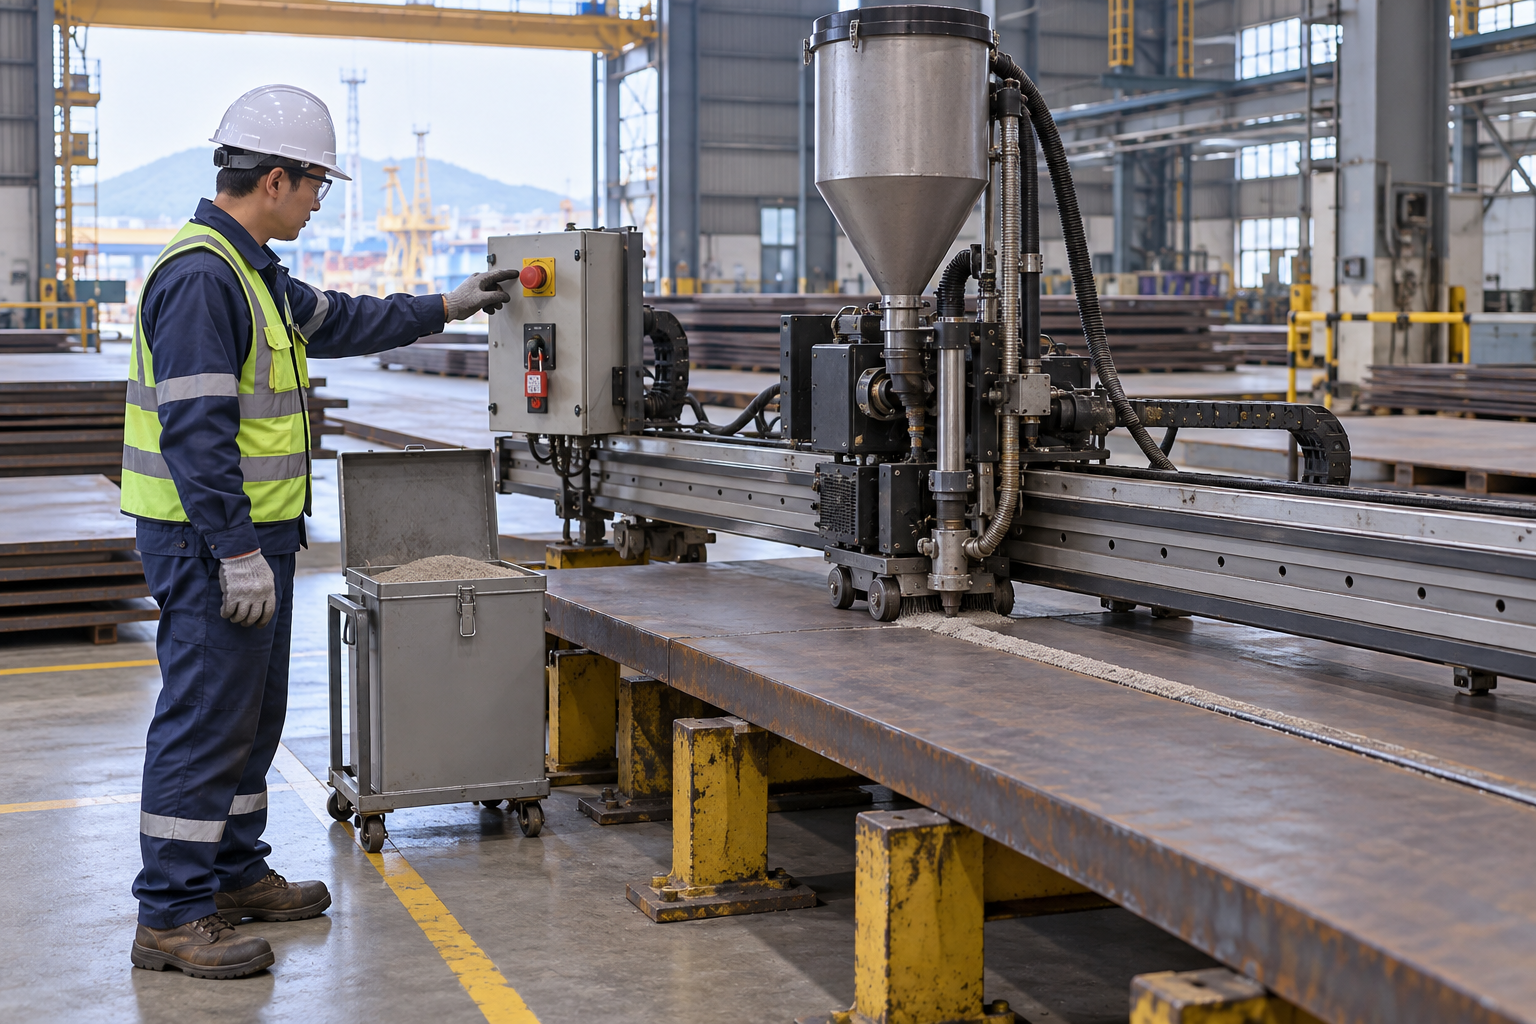
Retained AI-generated educational illustration from the source edition; not a real incident photograph, approved installation drawing or evidence of equipment suitability.
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Item | Fictional scenario |
|---|---|
| Initial | An opened flux container is ready for the next joint. |
| Change | Its label and storage history are missing. |
| Failure | Dry appearance is treated as proof of suitability. |
| Outcome | Consumable conformity and affected weld coverage cannot be established. |
| Barrier | Hold the container, identify prior weld intervals and separately decide material disposition, joint examination and new-work release. |
Why the controls matter
Flux identity, wire pairing and storage history matter even when granules look dry. An unmarked container cannot be accepted by appearance. Identify any joints already welded with uncertain material.
Redrying does not universally correct contamination or missing traceability. First establish product identity and permission to reuse, then follow its specified process. New flux does not retrospectively accept earlier welds.
Emergency stopping the carriage does not isolate wire feed, power or residual motion for access. Flux can hide hot metal and slag; verify safe access and temperature before recovery and cleaning.
Decision sequence
| Step | Decision |
|---|---|
| Known | Its label and storage history are missing. |
| Unknown | Actual condition, extent of damage and suitability of operator and stop, travel and heat remain to be established. |
| Hold | Dry appearance is treated as proof of suitability. |
| Evidence | Link operator and stop, travel and heat, fire and extraction, joint conditions, container and lot, affected weld range to the affected equipment or work area. |
| Next | Hold the container, identify prior weld intervals and separately decide material disposition, joint examination and new-work release. |
5. Conditional decisions and common errors
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Flux untraceable | Hold container and affected joints | Lot storage and usage map | Disposition established |
| Rail condition unknown | Hold travel | Support stops and cable path | Travel envelope verified |
| Feed adjustment needed | Stop and isolate | Power feed and residual motion | Safe access verified |
| New flux installed | Review earlier welds separately | Affected joints and examination | Both releases documented |
Similar appearance, different evidence
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Comparison | Supported decision | Insufficient basis |
|---|---|---|
| Condition | Lot storage and usage map | Flux untraceable has not been resolved. |
| Evidence | Power feed and residual motion | A photograph or a completed-looking task without the relevant inspection record. |
| Release | Both releases documented | Completion of one step does not release the excluded tasks in section 2. |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Assign the task boundary, stop authority, interfaces and emergency communication for submerged arc welding with rail carriage. |
| Technical lead | Confirm Joint and base material; Wire flux and WPS; Fixture and fit; Fire and ventilation plan. Resolve design and manufacturer limits before work. |
| Authorised crew | Apply Flux lot and packaging; Storage and drying; Recovery permission; Wire and feed guard. Stop when the working arrangement changes. |
| Inspector / receiving lead | Review Operator and stop; Travel and heat; Fire and extraction; Joint conditions. Transfer Temperature marking; Parking and power; Open-item disposition; Weld consumable history. |
Role labels allocate responsibilities; they do not confer a legal qualification. Verify the competence, training and authority required for the actual task.
The principal and employers coordinate the risk assessment and safe work procedures. These role labels allocate work; verify any qualifications and statutory appointments required for the actual Singapore activity. The receiving person must be given restrictions and unresolved defects before handover.
Record and handover perspective
| Stage | Record controls | Verification |
|---|---|---|
| Identify joint and WPS | 1. Record joint and base material2. Record wire flux and wps3. Record fixture and fit | 1. Wire flux and WPS2. Fixture and fit3. Fire and ventilation plan |
| Prepare consumables | 1. Record flux lot and packaging2. Record storage and drying3. Record recovery permission | 1. Storage and drying2. Recovery permission3. Wire and feed guard |
| Check power and setup | 1. Record insulation and return2. Record polarity, current/a, speed3. Record feed guard | 1. Polarity, current/A, speed2. Feed guard3. Ventilation and PPE |
| Run automatic weld | 1. Record operator and stop2. Record travel and heat3. Record fire and extraction | 1. Travel and heat2. Fire and extraction3. Joint conditions |
| Hold uncertain flux | 1. Record container and lot2. Record affected joint and weld length3. Record examination and repair | 1. Affected joint and weld length2. Examination and repair3. Restart authority |
| Close and handover | 1. Record temperature marking2. Record parking and power3. Record open-item disposition | 1. Parking and power2. Open-item disposition3. Weld consumable history |
7. Hold points and record comparison
| Hold point | Evidence before release | Actual record |
|---|---|---|
| HP-0 Start | Task boundary, site RA, SWP, responsibilities and emergency arrangements | |
| HP-1 Set rail carriage | Rail and end stops; Carriage stability; Cable path; Stop and exclusion | |
| HP-2 Prepare consumables | Flux lot and packaging; Storage and drying; Recovery permission; Wire and feed guard | |
| HP-3 Recover and inspect | Isolation and rest; Temperature and slag; Recovered flux status; Joint inspection | |
| HP-4 Close and handover | Temperature marking; Parking and power; Open-item disposition; Weld consumable history |
These are internal hold points, not issued permits. Recheck affected points after a change, fault or shift handover; link the actual approval record.
Record comparison
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
The boxes are static record prompts, not interactive or saved approvals. A tick does not establish suitability or permission to restart. Record the evidence, person, time and unresolved issues; retain the change history.
| Record | Insufficient | Record checklist |
|---|---|---|
| Identify joint and WPS | "Checked" without target, criteria or result | □ Joint and base material□ Wire flux and WPS□ Fixture and fit□ Fire and ventilation plan |
| Prepare consumables | "Checked" without target, criteria or result | □ Flux lot and packaging□ Storage and drying□ Recovery permission□ Wire and feed guard |
| Run automatic weld | "Checked" without target, criteria or result | □ Operator and stop□ Travel and heat□ Fire and extraction□ Joint conditions |
| Close and handover | "Checked" without target, criteria or result | □ Temperature marking□ Parking and power□ Open-item disposition□ Weld consumable history |
Hold points are internal checks. Determine separately whether Singapore statutory or site permit requirements apply to this work. Leave confirmation, measurements and approval records blank until the authorised site process is completed.
8. Site checklist and emergency response
| Check | Result | Person / action |
|---|---|---|
| □ Identify joint and WPS: Joint and base material | ||
| □ Set rail carriage: Rail and end stops | ||
| □ Prepare consumables: Flux lot and packaging | ||
| □ Check power and setup: Insulation and return | ||
| □ Run automatic weld: Operator and stop | ||
| □ Recover and inspect: Isolation and rest | ||
| □ Hold uncertain flux: Container and lot | ||
| □ Close and handover: Temperature marking | ||
| □ Emergency access and handover restrictions |
Stop work
Stop if flux untraceable, rail condition unknown, feed adjustment needed. Keep the affected operation on hold until the listed evidence and proceed conditions are satisfied; a low risk score does not release missing safeguards.
Emergency response
Stop from a safe location, exclude people from the affected danger zone and activate the site emergency plan. Call the site emergency service for injury or immediate danger. Do not enter an unstable, energised or confined danger area for an improvised rescue; trained responders must control the specific energy and access hazards.
9. Sources and review limits
Official public sources read for this Singapore edition on 2026-10-14. Guidance, statutory explanations and manufacturer limits have different roles; no source provider has approved this JSA.
| Source | Read scope and application limits |
|---|---|
| MOM — Risk management | Official explanation: employer, self-employed person and principal responsibilities; routine and non-routine risk assessment; hierarchy of controls; multidisciplinary assessment team. Official explanation of risk-management duties; no claim of reading the full linked statute. It does not specify task-specific equipment limits. Assess submerged arc welding with rail carriage with employers, principal and affected contractors; resolve the inputs in section 2. |
| MOM — When should my company review its risk assessment? | Review every three years, after significant changes, new machinery/substances/procedures, hazard-related injury or incident, and when assessment is inadequate. General review guidance. A review interval does not permit continued operation after a known hazard or change. Reassess this operation after changes, defects, incidents or an inadequate assessment; do not wait for a scheduled review. |
| MOM — Permit-to-Work Systems | Formal work authorisation and coordination; OPEC tripartite guidance and competent permit authority with authority to reject work. OPEC-focused guidance page; not evidence of a blanket statutory permit requirement for every task. Determine permits for this actual activity and workplace; distinguish the section 7 internal hold points from statutory or site permits. |
| WSH Council — Guidelines on Safe Use of Machinery | Sections 1.1 and 1.3: scope and explanation of safeguarding/LOTO duties. Sections 4.3–4.4.3: training, maintenance, specified replacement parts and isolation of all energy sources; commissioning safety-device checks. Official practical guidance and explanation; complete current subsidiary legislation and every annex were not read. Actual manufacturer isolation and restoration instructions remain necessary. Use machinery guidance for guards, travel and energy isolation, hot-work guidance for fire controls, chemical/GHS guidance for flux and fumes, and electrical guidance for competent defect correction. |
| WSH Council — Flammable Materials Guidelines (2015) | Page 36 hot-work permit subsection: competent site check, combustible removal, flammable-gas assessment and fire protection/fire watch. Selected guidance for flammable-material environments only, not a complete current statute review or universal fire-watch duration. Site/sector permit conditions must be checked. Use machinery guidance for guards, travel and energy isolation, hot-work guidance for fire controls, chemical/GHS guidance for flux and fumes, and electrical guidance for competent defect correction. |
| WSH Council — Preventing Chemical Hazards | Chemical exposure routes, employer/employee roles, risk assessment, safe work procedures, communication, SDS, exposure monitoring and substance-dependent health surveillance. Official overview; linked exposure schedules and medical examination regulations were not read in full. Do not infer a numerical exposure limit or a universal medical examination duty. Use machinery guidance for guards, travel and energy isolation, hot-work guidance for fire controls, chemical/GHS guidance for flux and fumes, and electrical guidance for competent defect correction. |
| WSH Council — GHS classification and labelling | GHS purpose and role table: suppliers provide product classification/labels/SDS; occupiers and employers obtain accessible SDS, label containers, train and inform workers. Official hazard-communication explanation, not approval of any product or proof of equipment material compatibility. Full SS 586 was not read. Use machinery guidance for guards, travel and energy isolation, hot-work guidance for fire controls, chemical/GHS guidance for flux and fumes, and electrical guidance for competent defect correction. |
| WSH Council — Electrocution-related Workplace Fatal Injuries in 2H2023 | Complete one-page advisory, particularly competent workers, equipment labelling, de-energisation, lockout, permit coordination, protective measures and defect maintenance. Official advisory recommendations, not a blanket statutory live-work permission. Direct General Provisions statute access failed; linked SS 638/SS 571 full texts were not read. Use an appropriate complete proving-dead method for the actual equipment; a general detector recommendation does not settle every circuit test. Use machinery guidance for guards, travel and energy isolation, hot-work guidance for fire controls, chemical/GHS guidance for flux and fumes, and electrical guidance for competent defect correction. |
No generic flux-baking temperature, current range, travel speed or recovery ratio is assigned. Actual WPS, flux SDS and carriage instructions were not supplied. Integrated positioners, altered automatic sequences, multiple-electrode conversions and internal repairs require separate review. Full welding and machinery standards were not read.
Actual site measurements, equipment instructions, engineering checks and signed approval records were not supplied. A qualified person must resolve these before use.
10. PDF guidance and FAQ
PDF A covers basic task controls; B focuses on technical failures; C covers supervision, records and handover. The article has eight stages with four items per main cell; each PDF has six key stages with three items per main cell. P/S/R/A, measurements, confirmations and signatures remain blank for actual site assessment.
Content group
jsa-submerged-arc
Is dry-looking flux acceptable?
Only with verified identity, storage and approved pairing.
Can all questionable flux be redried?
No. Follow product-specific reuse criteria after resolving identity and contamination.
Does emergency stop allow nozzle adjustment?
No. Establish the required isolation and safe access state.
Does new flux release earlier joints?
No. Track and assess the prior affected intervals separately.
Has a professional approved this JSA?
This reference material was written and reviced with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
11. Revision history and authorship
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to applicable Singapore requirements, the actual equipment/site and approved safe work procedures.
This Singapore edition was adapted from the Korean original and its assigned US technical reference. Earlier source revisions are archival editorial history, not Singapore technical approval.
| Date | Edition | Change | Review status |
|---|---|---|---|
| 2026-09-20 | Korean source v1.0 | Source editorial publication or revision; retained as provenance of the Korean edition. | Editorial record only; no professional technical approval recorded. |
| 2026-09-23 | Korean source v1.1 | Source editorial publication or revision; retained as provenance of the Korean edition. | Editorial record only; no professional technical approval recorded. |
| 2026-10-14 | 1.0 en-SG | Singapore legal scope, local planning, responsibility interfaces and SI terminology; new PDF A/B/C. | AI editorial and visual review only; no professional approval. |