Select, mount and use a suitable portable grinder wheel to finish an identified weld within its approved finishing limits, followed by stopped inspection and handover.
Stop for unknown wheel purpose/rating, damage, unsuitable guards/handles, workpiece movement, abnormal vibration/noise or suspected overgrinding. Wait for standstill and separate power before investigation.
AI-generated reference material. It has not been professionally verified or approved. Before use, a suitably qualified person must review and adapt it to applicable Singapore requirements, the actual equipment and site, and approved safe work procedures.
1. Legal and technical scope
Apply Singapore workplace risk management to the actual weld, coating, grinder and surrounding work. WSHC machinery guidance supports suitable guards, trained users and safe isolation for wheel changes; electrical repairs requiring licensed work go to the appropriate LEW. Assess metal and coating dust and noise, and arrange applicable hygiene monitoring rather than accepting a mask or visible ventilation as sufficient evidence. Coordinate spark-producing grinding with site hot-work controls, including hidden and lower-level combustibles. This worksheet does not establish a universal statutory permit or trial duration.
Assess the actual activity under the applicable Singapore WSH requirements. Statutory duties, official guidance, manufacturer instructions and approved project documents have distinct roles. A site hold point is not automatically a statutory permit. Use competent local review to resolve the applicable industry, installation, access and permit requirements.
| Basis | Application and limits |
|---|---|
| MOM risk management | Official explanation: risk assessment, control, monitoring and communication for routine and non-routine work, including maintenance; reviewed 14 October 2026. |
| WSHC preventing machine hazards | Official guidance: hierarchy of controls, guarding, competent operators and maintenance LOTO. It is not a model-specific isolation instruction. |
| WSHC electrical safety | Official guidance: maintenance energy isolation, stored-energy control, verification and reinstatement; electrical scope still requires applicable EMA authorisation. |
| EMA worker licences | Official explanation of licensed electrical work, supervision and the distinction where equipment work involves no wiring. Actual electrical duties require the appropriate licence class. |
| MOM requirements for hygiene monitoring | Official toxic-substance and noise monitoring guidance: competent personnel, exposure-dependent requirements, records, worker information and reporting. No site exposure result is asserted. |
| MOM safe storage of combustible materials in construction | Two-page 2016 circular reviewed: elevated hot-work sparks can reach combustible material below; separate ignition sources, control storage and maintain protective covering/SWP. Historical examples are not the fictional case in this article. |
| Bosch Professional angle-grinder application guidance | Selected inspection, preparation, handling and mounting sections: isolation, accessory purpose/speed/dimensions, guarding, workholding, sparks and standstill. Regional spindle dimensions and product settings are not Singapore requirements. |
| SCDF emergency medical services | Official 995 emergency ambulance service information; use emergency services for actual emergencies. |
2. Scope and required inputs
Included: Select, mount and use a suitable portable grinder wheel to finish an identified weld within its approved finishing limits, followed by stopped inspection and handover.
Separate review: Metal cutoff, design section changes, defect-removal repair, confined spaces and hazardous classified locations require separate procedures. This article does not authorize weld repair or supply acceptance dimensions.
| Input | Required evidence |
|---|---|
| Match weld scope | Weld/drawing ID; Material/coating data; Fire and exposure assessment; Work boundary |
| Select wheel | Tool/wheel rating; Permitted contact face; Dimensions and guard; Bore/flange method |
| Grind within limits | Contact and snag points; Handle/stance/direction; Remaining dimensions; Capture and boundary |
| Close and transfer | Fire-watch disposition; Tool/wheel status; Pending work/holds; Weld inspection/handover |
Match maximum tool speed, wheel purpose, dimensions, mounting and guard to the actual manufacturer instructions. Obtain approved weld finishing limits, remaining dimensions and inspection criteria. No universal wheel angle, tightening value, removal depth or trial-running time is provided.
3. Eight-stage JSA
P = likelihood; S = severity; R = risk under the site method; A = acceptance or authorization as defined by the site. Leave these blank until actual assessment and control verification. A low score does not override a legal requirement, product limit or unreleased hold point.
| Job stage | Hazards and effects | Failure factors | Required controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Match weld scope | 1. Section loss2. Coating-dust exposure3. Nearby fire4. Bystander struck | 1. Finish limits unclear2. Material unknown3. Spark travel missed4. Work boundary absent | 1. Match weld and finish drawing2. Identify metal/coating3. Plan sparks/dust control4. Coordinate adjacent work | 1. Weld/drawing ID2. Material/coating data3. Fire and exposure assessment4. Work boundary | ||||
| 2. Secure work area | 1. Workpiece movement2. Awkward-posture fall3. Electric shock4. Fragment exposure | 1. Support unsuitable2. Edge access restricted3. Lead touches work4. Eye/face gaps | 1. Secure workpiece2. Plan approach and stance3. Protect power leads4. Select assessed PPE | 1. Clamp/support state2. Approach/kickback route3. Lead/connectors4. Eye/face/hearing controls | ||||
| 3. Select wheel | 1. Wheel fracture2. Side-load failure3. Guard interference4. Mounting release | 1. Speed mismatch2. Cutoff purpose confused3. Wrong diameter/thickness4. Wrong flange/bore | 1. Match maximum speed2. Verify actual grinding purpose3. Match guard dimensions4. Use specified mounting | 1. Tool/wheel rating2. Permitted contact face3. Dimensions and guard4. Bore/flange method | ||||
| 4. Mount and trial | 1. Unexpected start2. Damaged-wheel breakup3. Vibration4. Bystander hit | 1. Power left connected2. Inspection omitted3. Mount/handle loose4. Trial boundary absent | 1. Separate power at standstill2. Inspect/test for wheel type3. Mount guards and handle4. Run instructed safe trial | 1. Isolated/stopped state2. Wheel damage/history3. Mount and guard checks4. Trial duration/observations | ||||
| 5. Grind within limits | 1. Kickback2. Wheel overload3. Base-metal gouge4. Spark/dust exposure | 1. Bad edge approach2. Unapproved contact face3. Removal limit ignored4. Capture/boundary lost | 1. Use intended wheel face2. Maintain two-hand control3. Check geometry progressively4. Maintain sparks/dust controls | 1. Contact and snag points2. Handle/stance/direction3. Remaining dimensions4. Capture and boundary | ||||
| 6. Stop and inspect | 1. Coasting contact2. Hot-metal burn3. Overground weld used4. Hidden defect | 1. Tool laid down spinning2. Heat ignored3. Appearance accepted4. Weld ID not linked | 1. Wait for complete stop2. Check heat and smouldering3. Verify dimensions/inspection4. Link unresolved findings | 1. Standstill/power state2. Residual heat3. Geometry/inspection4. Weld-specific hold | ||||
| 7. Hold abnormality | 1. Continued wheel breakup2. Wrong wheel reused3. Unresolved restart4. Further weld loss | 1. Noise ignored2. Replacement unidentified3. Trial omitted4. Repair improvised | 1. Stop and restrict access2. Inspect isolated configuration3. Recheck matched wheel/trial4. Review weld disposition | 1. Fault time/tool/weld2. Wheel/mount/guard3. Replacement and trial4. Affected area/release | ||||
| 8. Close and transfer | 1. Hidden fire spreads2. Damaged tool reused3. Uninspected weld covered4. Wrong acceptance scope | 1. Spark destinations missed2. Defect unmarked3. Hold not passed on4. Record detached from weld | 1. Check heat/spark reach2. Segregate defective tools3. Transfer use restrictions4. Link inspection and changes | 1. Fire-watch disposition2. Tool/wheel status3. Pending work/holds4. Weld inspection/handover |
4. Hypothetical scenario and failure mechanisms
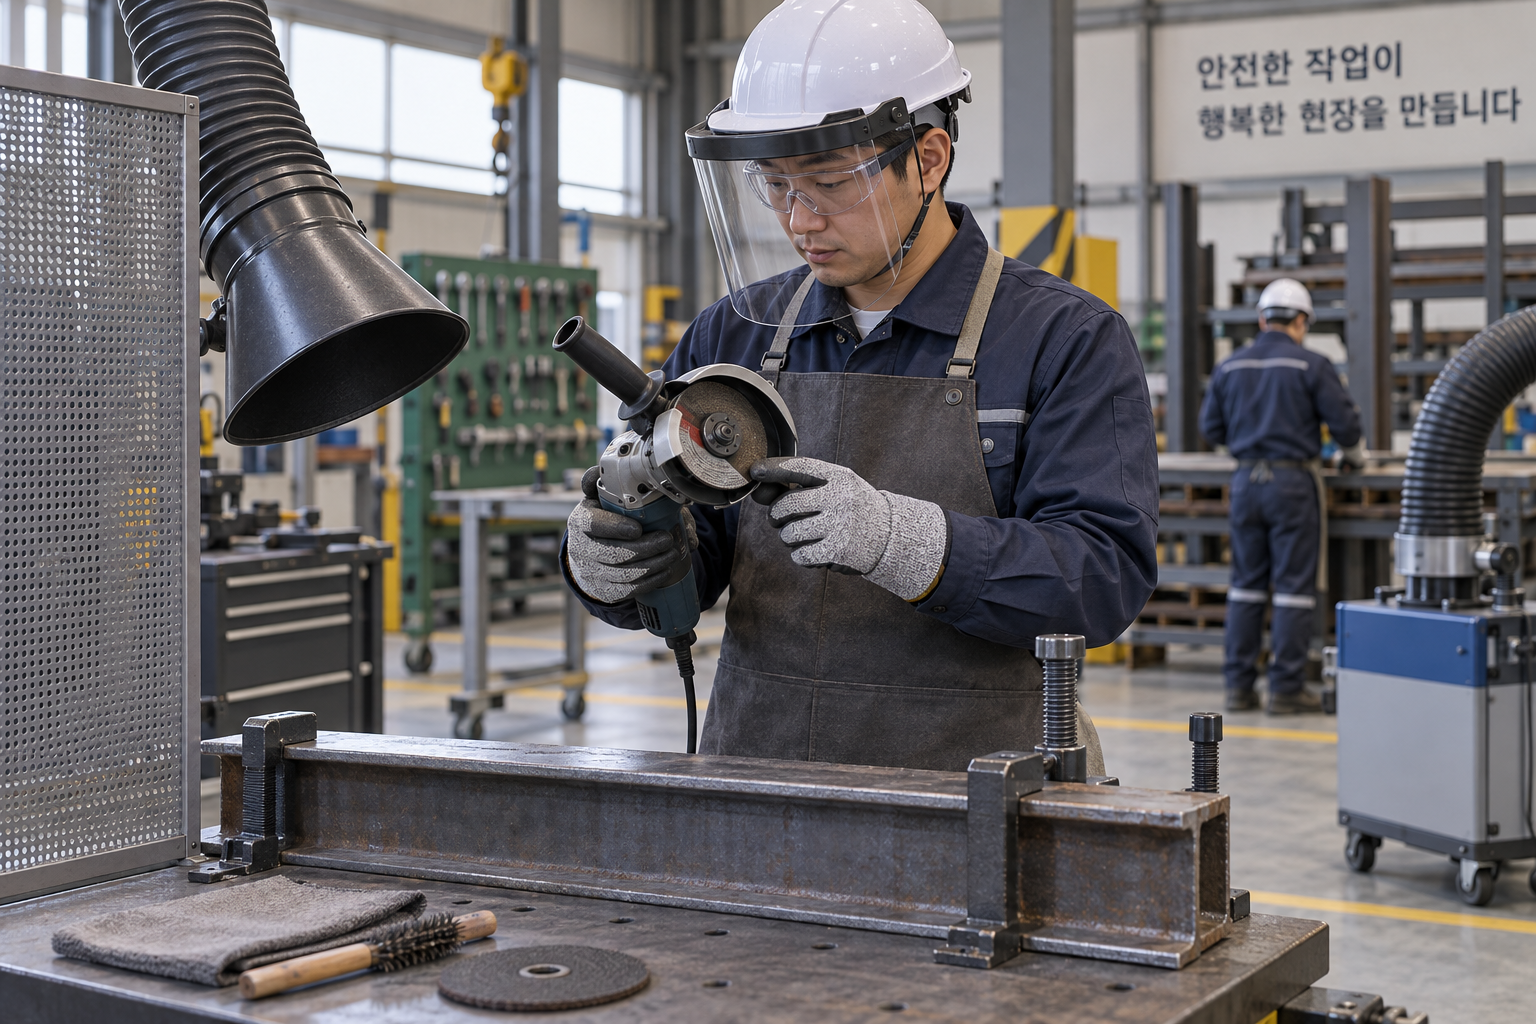 Retained source illustration: an AI-generated educational concept, not a real incident photograph or evidence of equipment suitability.
The following scenario, comparisons and example records are hypothetical teaching material. They do not reproduce actual incidents, measurements, signatures or approvals.
| Item | Hypothetical situation |
|---|---|
| Initial state | A wheel fits the grinder and its speed rating appears suitable. |
| Change | The worker uses its side on a weld although the wheel is not intended for side grinding. |
| Failure path | Physical fit and speed are treated as full permission for that contact direction. |
| Possible harm | Unintended side load can damage the wheel and expose people to fragments; the weld may also require inspection. |
| Barrier | Stop, wait for standstill, disconnect and identify the tool and affected weld before checking suitable replacement, guarding, trial and weld disposition. |
Speed compatibility is only one condition. A cutoff wheel not designed for side loading remains unsuitable for side grinding even at a lower speed. Match all accessory and guard instructions.
Kickback from a snag and wheel fracture are different failure paths. Either can occur without the other; plan approach, secure the work and maintain control without forcing the tool.
Inspect and test the wheel using methods applicable to its construction and actual instructions. Do not assume a sound or ring test is suitable for every accessory. A trial cannot make a damaged or unsuitable wheel acceptable.
A smooth bead can hide excess material removal. Compare remaining geometry and required inspection to the identified weld; hold suspect areas from further grinding and follow-on work pending disposition.
Trace sparks beyond the immediate bench, through openings and to lower floors. Assign the site fire-watch and closeout arrangements to the actual exposure. Separately review metal/coating dust and noise with the workplace exposure-control programme.
| Decision | Reason and evidence |
|---|---|
| Known facts | The worker uses its side on a weld although the wheel is not intended for side grinding. |
| Unresolved | Physical fit and speed are treated as full permission for that contact direction. |
| Hold reason | Stop for unknown wheel purpose/rating, damage, unsuitable guards/handles, workpiece movement, abnormal vibration/noise or suspected overgrinding. Wait for standstill and separate power before investigation. |
| Evidence needed | Standstill/power state; Residual heat; Geometry/inspection; Weld-specific hold. |
| Next decision | Stop, wait for standstill, disconnect and identify the tool and affected weld before checking suitable replacement, guarding, trial and weld disposition. |
5. Conditional decisions and common errors
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Wheel use unclear | Do not mount/use | Accessory marking and actual instructions | Purpose matched |
| Vibration develops | Stop, separate power and inspect | Wheel, mounting, guard and workholding | Cause resolved |
| Possible overgrind | Hold affected weld and follow-on work | Dimensions and required inspection | Disposition accepted |
| Sparks escape | Stop and restore boundaries | Combustibles, hidden spaces and exposure controls | Area controlled |
| Comparison | Situation A | Situation B |
|---|---|---|
| Wheel fits spindle | Physical assembly may be possible | Use, rating and guard compatibility unresolved |
| Weld looks smooth | Surface appearance changed | Remaining size and inspection acceptance unproved |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Confirm scope, task sequence, exclusion and stop authority. Coordinate match weld scope with affected operations. |
| Technical reviewer | Resolve the actual design and equipment limits: Weld/drawing ID; Material/coating data; Fire and exposure assessment; Work boundary. |
| Work crew | Perform select wheel using the approved procedure; report any mismatch before proceeding. |
| Inspector / assessor | Verify Standstill/power state; Residual heat; Geometry/inspection; Weld-specific hold. Record what was actually checked and what remains unresolved. |
| Release / receiving authority | Confirm Fire-watch disposition; Tool/wheel status; Pending work/holds; Weld inspection/handover. Transfer restrictions and the next permitted stage. |
These are responsibility examples, not invented statutory credentials. Meet the actual training, competent-person, qualified-person and licensing requirements for the assigned work. Anyone may raise a hazard and request a stop; only the designated authority may release the affected stage after evidence is reviewed.
7. Hold points and record comparison
| Hold point | Evidence before release | Confirmation / approval |
|---|---|---|
| HP-0 Start | Scope, jurisdiction, equipment identity, responsible people and emergency arrangements. | |
| HP-1 Select wheel | Tool/wheel rating; Permitted contact face; Dimensions and guard; Bore/flange method | |
| HP-2 Mount and trial | Isolated/stopped state; Wheel damage/history; Mount and guard checks; Trial duration/observations | |
| HP-3 Grind within limits | Contact and snag points; Handle/stance/direction; Remaining dimensions; Capture and boundary | |
| HP-4 Stop and inspect | Standstill/power state; Residual heat; Geometry/inspection; Weld-specific hold |
Hold points are internal evidence gates. They do not replace statutory permits or actual signatures. Recheck affected gates after a change, abnormal event or shift transfer. The blank record must identify the evidence, person, time, limits and release scope.
| Record | Insufficient record | Record checklist |
|---|---|---|
| Wheel | Fits the spindle | □ Tool/wheel rating□ Permitted contact face□ Dimensions and guard□ Bore/flange method |
| Trial | Runs normally | □ Isolated/stopped state□ Wheel damage/history□ Mount and guard checks□ Trial duration/observations |
| Weld | Looks smooth | □ Standstill/power state□ Residual heat□ Geometry/inspection□ Weld-specific hold |
| Handover | Grinding finished | □ Fire-watch disposition□ Tool/wheel status□ Pending work/holds□ Weld inspection/handover |
The □ boxes are static prompts, not saved or interactive approvals. Each checks one record element. A tick alone does not establish suitability or permission to restart. Link equipment IDs and supporting records; retain unresolved matters and the earlier record when conditions change.
8. Site checklist and emergency response
| Check item | Result | Person / action |
|---|---|---|
| Weld/drawing ID | ||
| Clamp/support state | ||
| Tool/wheel rating | ||
| Isolated/stopped state | ||
| Contact and snag points | ||
| Standstill/power state | ||
| Fault time/tool/weld | ||
| Fire-watch disposition | ||
| Emergency arrangements and unresolved restrictions communicated |
Stop work: Stop for unknown wheel purpose/rating, damage, unsuitable guards/handles, workpiece movement, abnormal vibration/noise or suspected overgrinding. Wait for standstill and separate power before investigation.
Emergency response: Stop safely and keep people clear of fragments, hot metal and unstable work. Do not grasp a coasting wheel. Raise the site alarm and evacuate for uncontrolled smoke or fire; call SCDF 995 for serious injury or urgent rescue. Preserve tool and weld identification and retain the hold until the fault and affected work are assessed.
9. Sources and review limits
Official-source review date: October 14, 2026. The following review is limited to the public provisions or selected manufacturer material identified below. It does not establish that any authority approved this article or the actual installation.
- MOM risk management: Official explanation: risk assessment, control, monitoring and communication for routine and non-routine work, including maintenance; reviewed 14 October 2026.
- WSHC preventing machine hazards: Official guidance: hierarchy of controls, guarding, competent operators and maintenance LOTO. It is not a model-specific isolation instruction.
- WSHC electrical safety: Official guidance: maintenance energy isolation, stored-energy control, verification and reinstatement; electrical scope still requires applicable EMA authorisation.
- EMA worker licences: Official explanation of licensed electrical work, supervision and the distinction where equipment work involves no wiring. Actual electrical duties require the appropriate licence class.
- MOM requirements for hygiene monitoring: Official toxic-substance and noise monitoring guidance: competent personnel, exposure-dependent requirements, records, worker information and reporting. No site exposure result is asserted.
- MOM safe storage of combustible materials in construction: Two-page 2016 circular reviewed: elevated hot-work sparks can reach combustible material below; separate ignition sources, control storage and maintain protective covering/SWP. Historical examples are not the fictional case in this article.
- Bosch Professional angle-grinder application guidance: Selected inspection, preparation, handling and mounting sections: isolation, accessory purpose/speed/dimensions, guarding, workholding, sparks and standstill. Regional spindle dimensions and product settings are not Singapore requirements.
- SCDF emergency medical services: Official 995 emergency ambulance service information; use emergency services for actual emergencies.
Paid consensus standards and site-specific calculations, manuals, inspection records and product certificates were not independently obtained or verified unless specifically identified. Korean and overseas legal references are source history, not Singapore statutory duties. Singapore Standards and model-specific limits were not read in full unless expressly identified.
10. PDF guidance and FAQ
PDF A covers basic task controls; B examines technical failures; C focuses on supervision, evidence and handover. Each has six rows and three items per main cell. They are complementary extracts: apply all eight body stages and the applicable site procedure. An omitted stage is not permission to omit its controls. PDF HP-0 through HP-4 are worksheet labels; match the event, evidence and authority rather than assuming they match another permit by number.
P/S/R/A, actual measurements, confirmations and signatures remain blank. The PDFs are uncompleted reference worksheets, not issued work permits.
Content group ID: jsa-grinder-weldfinish
Can a cutoff wheel side grind?
Only a wheel specifically intended for the actual grinding use may be selected; fitting and speed rating alone do not permit side loading.
Should vibration be managed by pressing more lightly?
Stop and investigate after standstill and power separation. Do not continue with unexplained vibration.
Does a smooth weld pass inspection?
No. Verify the required geometry and specified inspection and disposition any overground area.
What follows wheel replacement?
Record accessory identity, fit/guard checks and the actual instructed trial, plus the cause of the previous fault and weld impact.
Has a professional verified or approved this document?
AI-generated reference material. It has not been professionally verified or approved. Before use, a suitably qualified person must review and adapt it to applicable Singapore requirements, the actual equipment and site, and approved safe work procedures.
11. Revision history and authorship
AI-generated reference material. It has not been professionally verified or approved. Before use, a suitably qualified person must review and adapt it to applicable Singapore requirements, the actual equipment and site, and approved safe work procedures.
This system has not physically inspected the equipment, structures, ground, atmosphere or worksite. The document does not replace legal advice, manufacturer procedures, engineering design, inspection certificates, qualification evidence, the site risk assessment or an actual work permit.
Before use, a suitably qualified and authorized person must review the actual equipment, loads, methods, protection, inspection and emergency arrangements and resolve open issues. Record the real reviewer, organization, qualifications, delegated authority, reviewed documents, date, signature, exclusions and conditions of approval separately.
| Date | Version | Change | Review status |
|---|---|---|---|
| 2026-09-20 | 1.0 | Korean source revision retained in the source snapshot. | Historical editorial status; not Singapore professional approval. |
| 2026-09-23 | 1.1 | Korean source revision retained in the source snapshot. | Historical editorial status; not Singapore professional approval. |
| 2026-10-14 | SG 1.0 | Singapore localisation of the Korean source with its assigned US technical reference; local applicability, task controls and sources reviewed. | AI-assisted editorial work; professional approval not performed. |