The clutch setting limits a tool response under particular conditions; it does not prove actual joint torque, thread engagement or seating. Same-number trials on another material do not establish an acceptable joint.
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to Singapore requirements, the actual equipment/site and approved safe work procedures.
Stop before starting
Stop for unresolved gaps, repeated slipping or reaction, poor workholding, damaged bits, abnormal battery heat/swelling or defective controls. Do not increase the setting to overcome an unexplained defect.
1. Legal and technical scope
| Basis | Scope and limits |
|---|---|
| MOM: Risk management | Assess reaction, screw penetration, joint defects and abnormal jam recovery. Official explanation of statutory duties; linked SSO text was not independently read for this item. This is not a legal opinion. |
| WSH Council: Preventing Machine Hazards | Use suitable guarding/control, competent operators and defect removal from service. Official practical guidance, not the actual machine isolation procedure or proof of equipment compliance. |
| WSH Council: Safe Use of Machinery | Prevent unexpected start during bit changes, inspection and jam recovery. Official guidance; cited paid Singapore Standards were not obtained. No universal wheel test duration or gap is inferred. |
| SCDF: Emergency Medical Services | Use 995 for a medical emergency while keeping people away from an unsafe battery or moving parts. Official emergency-response information, not a site-specific rescue plan or authorisation for untrained rescue. |
Apply Singapore WSH risk management and WSH Council machinery guidance to the assembly, rotating tool, workholding and battery. Establish the actual tool/battery instructions and the approved joint-inspection method before setting the clutch. A clutch index is not a calibrated torque value. Isolation for bit changes and fault recovery means the model-specific safe battery-disconnected state, not merely a direction lock or released trigger. This task does not provide structural-joint approval.
2. Scope and required inputs
Included work
Rotary screw fastening or removal on a secured ground-level bench assembly in a dry indoor area, using a removable-battery drill/driver in its specified fastening mode.
Separate assessment
Drilling, hammer or impact work, work at height, concealed live services, structural high-strength bolt acceptance and internal tool repair require separate assessment.
| Required input | Evidence to obtain |
|---|---|
| Check assembly | Workpiece and screw IDs; Drawing and revision; Backside clearance; Acceptance criteria |
| Inspect tool | Tool and battery model; Housing and terminal condition; Switch operation; Defect status |
| Fit bit and clamp | Bit fit and wear; Chuck engagement; Fixture security; Hand and backside clearance |
| Set and trial | Mode and setting; Trial assembly result; Reaction-control position; Inspection method used |
No actual equipment model, site measurements, design calculations or signed approval was supplied. Check the applicable Singapore requirements and approved safe work procedures against the actual equipment and site before use. Statutory duties, official guidance and manufacturer limits serve different purposes; editorial checks do not establish legal or professional approval.
Singapore site application
At a shared Singapore assembly bench, separate accepted and held parts and keep battery charging/storage away from loose metal screws and escape routes. Assign the assembly inspector separately from the person setting the tool.
Record screw length and relevant clearance in mm. If the joint specification gives torque, retain its N·m requirement and specified verification method; never translate a clutch number into N·m or reuse it across different materials without an accepted trial.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Technical and procedural controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Check assembly | 1. Joint separation2. Hidden-service damage3. Wrong screw penetration4. Defective product release | 1. Screw and material mismatch2. Backside not checked3. Length not specified4. Acceptance method unclear | 1. Match assembly instruction2. Check both sides of work3. Confirm screw specification4. Define inspection method | 1. Workpiece and screw IDs2. Drawing and revision3. Backside clearance4. Acceptance criteria | ||||
| 2. Inspect tool | 1. Unexpected start2. Battery thermal event3. Electrical contact4. Loss of speed control | 1. Battery installed for inspection2. Damaged housing ignored3. Contaminated terminals4. Switch defective | 1. Remove battery to inspect2. Reject damaged equipment3. Match battery to tool4. Check controls before use | 1. Tool and battery model2. Housing and terminal condition3. Switch operation4. Defect status | ||||
| 3. Fit bit and clamp | 1. Flying bit2. Rotating workpiece3. Finger puncture4. Chuck contact | 1. Wrong or worn bit2. Small part hand-held3. Chuck not secured4. Hand behind screw | 1. Fit specified bit2. Secure chuck per manual3. Clamp workpiece firmly4. Keep hands outside path | 1. Bit fit and wear2. Chuck engagement3. Fixture security4. Hand and backside clearance | ||||
| 4. Set and trial | 1. Wrist reaction injury2. Stripped thread3. Overtightened joint4. Unexpected direction | 1. Drill mode selected2. Clutch number assumed torque3. Trial omitted4. Direction not checked | 1. Select fastening mode2. Use approved setup3. Trial on suitable sample4. Verify direction and grip | 1. Mode and setting2. Trial assembly result3. Reaction-control position4. Inspection method used | ||||
| 5. Drive or remove | 1. Slipping-bit puncture2. Uncontrolled reaction3. Falling released part4. Entanglement | 1. Bit axis misaligned2. Workholding loosens3. Last screw unsupported4. Loose clothing near chuck | 1. Maintain stable axial grip2. Keep workpiece clamped3. Support parts before removal4. Keep clear of rotation | 1. Hand and bit separation2. Fixture remains secure3. Component support4. Screw and joint condition | ||||
| 6. Stop and inspect | 1. Contact with coasting bit2. Faulty assembly passed3. Tool falls from bench4. Sharp screw exposure | 1. Tool set down while rotating2. Clutch click accepted alone3. Unstable resting position4. Rejected parts mixed in | 1. Wait for complete stop2. Inspect by specified method3. Set tool down securely4. Separate rejected assemblies | 1. Rotation stopped2. Joint acceptance record3. Safe tool position4. Rejected part identification | ||||
| 7. Hold on jam | 1. Repeated wrist reaction2. Bit fracture3. Battery fire4. Worsening joint damage | 1. Trigger repeatedly pulsed2. Setting raised without cause3. Hot battery reused4. Damaged thread ignored | 1. Stop and remove battery2. Find jam and fit cause3. Quarantine unsafe battery4. Revalidate corrected setup | 1. Jam and affected parts2. Bit and fixture condition3. Battery defect assessment4. Trial and inspection evidence | ||||
| 8. Store and transfer | 1. Terminal short circuit2. Defective product use3. Wrong setup reused4. Unreported tool defect | 1. Battery stored with screws2. Rejected parts unmarked3. Setting basis not recorded4. Fault not transferred | 1. Protect battery terminals2. Label held assemblies3. Record accepted setup4. Transfer tool restrictions | 1. Tool and battery storage2. Accepted and held part IDs3. Setup and inspection basis4. Receiving person record |
P = likelihood; S = severity; R = risk under the site method; A = site-defined acceptance/authorization. These actual assessment cells are blank. A low score never overrides a missing safeguard or a legal or manufacturer restriction.
4. Fictional scenario and failure mechanisms
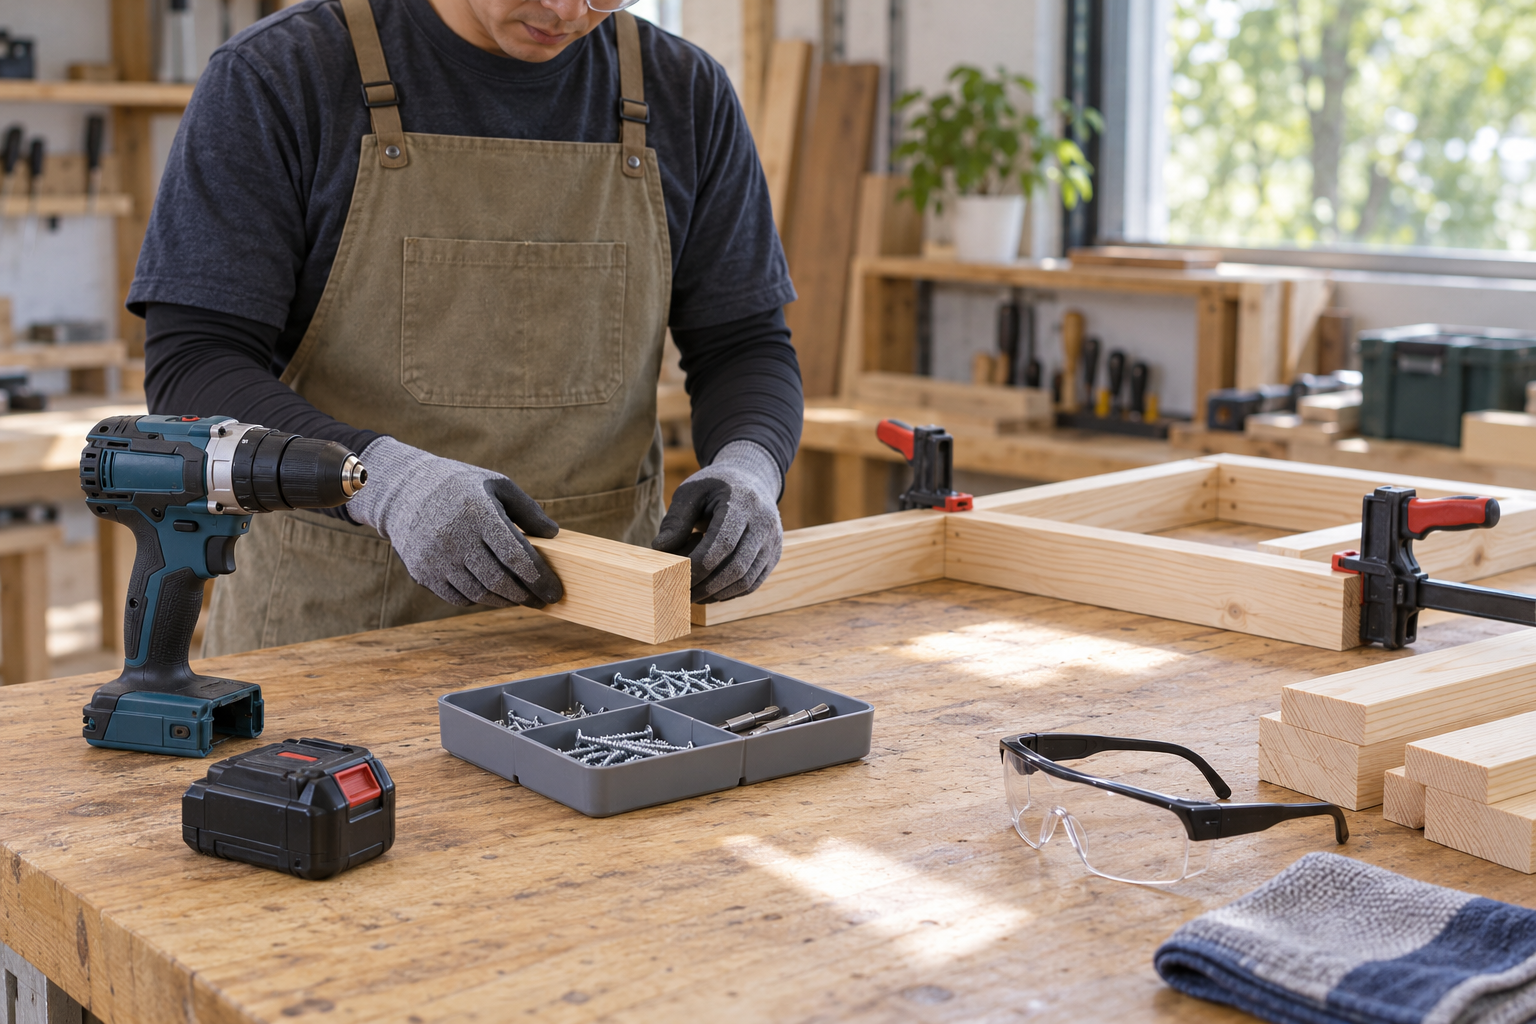
This illustration provides educational context. It is not an actual incident photograph or evidence of equipment suitability; any AI-generated depiction is illustrative only.
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Stage | Fictional situation |
|---|---|
| Initial situation | A fictional operator finds a gap after driving assembly screws. |
| Changed condition | The tool has clicked at its usual clutch setting. |
| Failure path | The operator proposes raising the setting and retightening every screw without checking length, alignment or thread condition. |
| Possible outcome | The joint could strip or crack while still appearing fastened. |
| Prevention barrier | Hold affected assemblies, inspect the cause, correct the setup and validate a trial with the specified acceptance method. |
Failure mechanisms
The clutch setting limits a tool response under particular conditions; it does not prove actual joint torque, thread engagement or seating. Same-number trials on another material do not establish an acceptable joint.
A persistent gap can result from incorrect screw length, misalignment, damaged threads or an unsuitable assembly sequence. Increasing the clutch may strip threads or damage the assembly without resolving the gap.
Clamp small workpieces and keep hands outside both the bit-slip line and the screw exit path. Before removing the final screw, support any cover or component that it retains. Use the specified handle and reaction-control method for the actual tool.
Stop fully and remove the battery before changing the bit or clearing a jam. A hot, swollen or damaged battery needs the site’s safe isolation and response method; do not handle an unsafe battery merely to complete a routine storage step.
Decision sequence
| Step | Decision |
|---|---|
| Known | A gap remains despite clutch operation. |
| Unknown | Screw engagement, alignment, length and thread condition are unresolved. |
| Hold | Do not raise the setting or repeatedly pulse the trigger as a diagnostic shortcut. |
| Evidence | Link part/screw IDs, fixture condition, corrected setup and trial inspection. |
| Release | Separate defective parts and release only assemblies meeting the specified joint criteria. |
Work sequence: Check assembly → Inspect tool → Fit bit and clamp → Set and trial → Drive or remove → Stop and inspect → Hold on jam → Store and transfer. This is a teaching flow, not a device drawing or a complete operating procedure.
5. Conditional decisions and common errors
| Situation | Required action | Evidence | Proceed when |
|---|---|---|---|
| Gap persists | Hold affected assembly | Length, alignment and thread checks | Cause corrected |
| Bit slips or jams | Stop; disconnect battery safely | Bit, fixture and screw condition | Trial accepted |
| Battery abnormal | Stop and restrict access | Safe battery assessment | Safe replacement arranged |
| Final screw removed | Support retained part | Support and clearance | Part controlled |
Similar observations, different decisions
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Observation | Insufficient conclusion | Required distinction |
|---|---|---|
| Clutch clicks | Required torque is proven. | Use the specified joint acceptance method; the index is not N·m. |
| Same clutch number | Another material will respond identically. | Validate the actual screw/material/setup combination. |
| Trigger released | Bit changes are safe. | Wait for full stop and establish the specified battery-disconnected state. |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Confirm workpiece and screw ids and the task scope, resources, interfaces and stop authority. |
| Qualified technical reviewer | Review tool and battery model, model limits, compatibility and unresolved technical conditions within assigned competence. |
| Work crew | Apply the listed controls, report changes and stop when evidence or safeguards are missing. |
| Inspector / assessor | Record actual hand and bit separation and other relevant checks; do not mark unverified conditions as accepted. |
| Handover authority | Reconcile tool and battery storage, restrictions and outstanding actions before the next task. Role labels do not establish a legal credential. |
Supervision and handover focus
| Stage | Management action | Evidence |
|---|---|---|
| Check assembly | 1. Record workpiece and screw ids2. Record drawing and revision3. Record backside clearance | 1. Workpiece and screw IDs2. Drawing and revision3. Backside clearance |
| Inspect tool | 1. Record tool and battery model2. Record housing and terminal condition3. Record switch operation | 1. Tool and battery model2. Housing and terminal condition3. Switch operation |
| Set and trial | 1. Record mode and setting2. Record trial assembly result3. Record reaction-control position | 1. Mode and setting2. Trial assembly result3. Reaction-control position |
| Drive or remove | 1. Record hand and bit separation2. Record fixture remains secure3. Record component support | 1. Hand and bit separation2. Fixture remains secure3. Component support |
| Hold on jam | 1. Record jam and affected parts2. Record bit and fixture condition3. Record battery defect assessment | 1. Jam and affected parts2. Bit and fixture condition3. Battery defect assessment |
| Store and transfer | 1. Record tool and battery storage2. Record accepted and held part ids3. Record setup and inspection basis | 1. Tool and battery storage2. Accepted and held part IDs3. Setup and inspection basis |
7. Hold points and record comparison
| Hold point | Evidence before release | Actual approval |
|---|---|---|
| HP-0 Scope | Rotary screw fastening or removal on a secured ground-level bench assembly in a dry indoor area, using a removable-battery drill/driver in its specified fastening mode. | |
| HP-1 Fit bit and clamp | Bit fit and wear; Chuck engagement; Fixture security; Hand and backside clearance | |
| HP-2 Set and trial | Mode and setting; Trial assembly result; Reaction-control position; Inspection method used | |
| HP-3 Hold on jam | Jam and affected parts; Bit and fixture condition; Battery defect assessment; Trial and inspection evidence | |
| HP-4 Store and transfer | Tool and battery storage; Accepted and held part IDs; Setup and inspection basis; Receiving person record |
Hold points are internal project checks. They are not universal statutory permits and do not grant work permission. Reassess after defects, changed conditions and shift changes.
Record comparison
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
The boxes are static record prompts, not interactive or saved approvals. A tick does not establish suitability or permission to restart. Record the evidence, person, time and unresolved issues; retain the change history.
| Record | Insufficient record | Record checklist |
|---|---|---|
| Check assembly | Only marked “OK” | □ Workpiece and screw IDs□ Drawing and revision□ Backside clearance□ Acceptance criteria |
| Set and trial | Only marked “OK” | □ Mode and setting□ Trial assembly result□ Reaction-control position□ Inspection method used |
| Hold on jam | Only marked “OK” | □ Jam and affected parts□ Bit and fixture condition□ Battery defect assessment□ Trial and inspection evidence |
| Store and transfer | Only marked “OK” | □ Tool and battery storage□ Accepted and held part IDs□ Setup and inspection basis□ Receiving person record |
8. Site checklist and emergency response
| Site check | Actual result | Person / action |
|---|---|---|
| Check assembly: Workpiece and screw IDs; Drawing and revision; Backside clearance; Acceptance criteria | ||
| Inspect tool: Tool and battery model; Housing and terminal condition; Switch operation; Defect status | ||
| Fit bit and clamp: Bit fit and wear; Chuck engagement; Fixture security; Hand and backside clearance | ||
| Set and trial: Mode and setting; Trial assembly result; Reaction-control position; Inspection method used | ||
| Drive or remove: Hand and bit separation; Fixture remains secure; Component support; Screw and joint condition | ||
| Stop and inspect: Rotation stopped; Joint acceptance record; Safe tool position; Rejected part identification | ||
| Hold on jam: Jam and affected parts; Bit and fixture condition; Battery defect assessment; Trial and inspection evidence | ||
| Store and transfer: Tool and battery storage; Accepted and held part IDs; Setup and inspection basis; Receiving person record |
Stop work
Stop for unresolved gaps, repeated slipping or reaction, poor workholding, damaged bits, abnormal battery heat/swelling or defective controls. Do not increase the setting to overcome an unexplained defect.
Emergency response
Release the trigger and move clear of moving parts. Keep people away from a smoking or otherwise unsafe battery and use the site emergency response; do not improvise handling or repair. Call 995 for a medical emergency. Isolate safely before recovering a trapped bit or component.
9. Sources and review limits
Public-source access/review: 2026-10-14.
| Official source | Reviewed scope and limits |
|---|---|
| MOM: Risk management | Assess reaction, screw penetration, joint defects and abnormal jam recovery. Official explanation of statutory duties; linked SSO text was not independently read for this item. This is not a legal opinion. |
| WSH Council: Preventing Machine Hazards | Use suitable guarding/control, competent operators and defect removal from service. Official practical guidance, not the actual machine isolation procedure or proof of equipment compliance. |
| WSH Council: Safe Use of Machinery | Prevent unexpected start during bit changes, inspection and jam recovery. Official guidance; cited paid Singapore Standards were not obtained. No universal wheel test duration or gap is inferred. |
| SCDF: Emergency Medical Services | Use 995 for a medical emergency while keeping people away from an unsafe battery or moving parts. Official emergency-response information, not a site-specific rescue plan or authorisation for untrained rescue. |
No actual equipment model, site measurements, design calculations or signed approval was supplied. Check the applicable Singapore requirements and approved safe work procedures against the actual equipment and site before use. Statutory duties, official guidance and manufacturer limits serve different purposes; editorial checks do not establish legal or professional approval.
10. PDF guidance and FAQ
PDF A covers basic task controls; B focuses on technical failures; C covers supervision, records and handover. The article has eight stages with four items per main cell; each PDF has six key stages with three items per main cell. P/S/R/A, measurements, confirmations and signatures remain blank for actual site assessment.
PDFs are complementary six-stage extracts. Apply all eight body stages and the actual equipment/site procedure.
Can the clutch number be entered as torque?
No. Record the setting as a setting; use the specified verification method for any torque requirement.
Can I tighten harder to close a gap?
Hold and inspect screw length, alignment and damage first.
Does the direction lock isolate the tool?
No. Follow the actual battery-removal and restart-prevention procedure.
What must be handed over?
Accepted and held part IDs, the validated setup, inspection evidence and tool/battery restrictions.
Has a professional verified or approved this document?
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to Singapore requirements, the actual equipment/site and approved safe work procedures.
11. Revision history and authorship
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to Singapore requirements, the actual equipment/site and approved safe work procedures.
| Date | Version | Change | Review status |
|---|---|---|---|
| 2026-10-14 | SG 1.0 | New Singapore edition from assigned Korean source; task decisions, records and PDFs localized. | AI editorial review; no professional technical approval |
Korean edition revision history: 2026-09-30 (v1.0): initial article, sources, fictional analysis and PDF editorial checks. These are editorial records, not professional technical approval. Singapore v1.0 adapts the earlier edition to Singapore requirements and terminology.
Site reviewers must add their actual qualifications, scope, date and approval only after the review occurs.