An extinguished arc does not stop a gas leak. CO2 is nonflammable but can accumulate and harm workers; an oxygen reading alone is not a CO2 exposure assessment.
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to Singapore requirements, the actual equipment/site and approved safe work procedures.
Stop before starting
Stop for suspected gas leakage, ineffective ventilation or fume capture, damaged insulation, abnormal wire feed or a WPS deviation. Restrict any area with an unverified atmosphere; arc-off is not clearance to enter.
1. Legal and technical scope
| Basis | Scope and limits |
|---|---|
| MOM: Risk management | Assess welding, breaks, gas leakage and feeder fault recovery as separate exposure conditions. Official explanation of statutory duties; linked SSO text was not independently read for this item. This is not a legal opinion. |
| MOM/NEA/SCDF: Revised SS 586 adoption | Verify actual gas and consumable identification and the Singapore-appropriate SDS. Official adoption circular, not full paid SS 586 text or a classification of the actual product; verify current supplier label and SDS. |
| WSH Council: Managing WSH for SMEs in Metalworking | Plan fire prevention, screens, fume extraction, opposite-side checks and post-work fire watch. Official sector guidance and sample controls, not a universal statutory permit rule, a qualified WPS or a current-edition certificate. Linked paid standards were not read; direct SSO General Provisions access returned 403. |
| MOM: Requirements for Hygiene Monitoring | Have competent personnel select relevant gas/fume exposure monitoring and Singapore criteria. Actual substances, exposure results and legal limits must be established for the site. No concentration or noise result is asserted. |
| WSH Council: Safe Use of Machinery | Isolate the powered feeder for intervention even when the arc is extinguished. Official guidance; cited paid Singapore Standards were not obtained. No universal wheel test duration or gap is inferred. |
| SCDF: Emergency Medical Services | Call 995 for a medical emergency without unprotected entry into a suspect atmosphere. Official emergency-response information, not a site-specific rescue plan or authorisation for untrained rescue. |
Assess CO2-shielded GMAW under Singapore WSH risk management, including fire, gas accumulation, welding fumes, electrical hazards and wire-feed maintenance. Use the Singapore-appropriate supplier SDS and applicable hygiene-monitoring requirements for actual substances and exposure. WSH Council metalworking guidance supports coordinated hot-work precautions and fire-watch checks; determine the actual site permit system rather than assuming one universal hot-work permit. Confined-space entry requires a separate assessment and permit/rescue arrangements and is excluded here.
2. Scope and required inputs
Included work
Prepare cylinders, wire feed, electrical equipment and workpieces for semiautomatic GMAW using carbon dioxide shielding gas; weld, stop, inspect and hand over affected joints.
Separate assessment
Confined-space welding, robotic cells, gas-system modification and internal power-source repair require separate plans. CO2 is an active shielding gas; this is not an inert-gas-only process.
| Required input | Evidence to obtain |
|---|---|
| Plan gas and weld | SDS and gas/fume monitoring; Joint and WPS; Fume control plan; Supply shutoff point |
| Arrange work | Cylinder restraint; Hose routing; Screens and access; Fixture condition |
| Check gas and feed | Gas compatibility; Leak test result; Feed guard and isolation; Wire path |
| Check electrical | Leads and grounding; Return connection; Workholding; Site hot-work permit conditions |
No actual equipment model, site measurements, design calculations or signed approval was supplied. Check the applicable Singapore requirements and approved safe work procedures against the actual equipment and site before use. Statutory duties, official guidance and manufacturer limits serve different purposes; editorial checks do not establish legal or professional approval.
Singapore site application
Review low sections, pits and poorly ventilated corners of the actual fabrication bay. Local fume capture at the arc may not control a separate hose leak; barriers and screens must not obstruct the planned ventilation or emergency exit.
Record joint ID, WPS revision, gas identity, current/voltage and the specified gas-flow units, such as L/min. Coordinate the fire-watch boundary with adjacent contractors and record affected welds after a gas-supply deviation.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Technical and procedural controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Plan gas and weld | 1. CO2 exposure2. Wrong weld conditions3. Coating fumes4. Delayed fire response | 1. Gas risk misunderstood2. WPS mismatch3. Unknown base material4. No watch assigned | 1. Assess gas environment2. Match gas and wire3. Identify coatings4. Assign fire response | 1. SDS and gas/fume monitoring2. Joint and WPS3. Fume control plan4. Supply shutoff point | ||||
| 2. Arrange work | 1. Cylinder overturn2. Hose damage3. Arc-light exposure4. Workpiece movement | 1. Unsecured cylinder2. Heat on hose3. Missing screens4. Poor fixture support | 1. Secure cylinders upright2. Protect hoses and leads3. Screen the arc area4. Support workpieces | 1. Cylinder restraint2. Hose routing3. Screens and access4. Fixture condition | ||||
| 3. Check gas and feed | 1. CO2 accumulation2. Pressure release3. Wire-roll pinch4. Wire puncture | 1. Leaking connection2. Wrong regulator3. Live roll adjustment4. Torch aimed at person | 1. Inspect gas connections2. Use correct regulator3. Isolate feed servicing4. Control torch direction | 1. Gas compatibility2. Leak test result3. Feed guard and isolation4. Wire path | ||||
| 4. Check electrical | 1. Electric shock2. Hot return joint3. Workpiece overturn4. Fire and fumes | 1. Damaged torch2. Poor return contact3. Missing clamps4. Combustible residue | 1. Inspect insulation2. Secure return path3. Clamp workpiece4. Control coating hazards | 1. Leads and grounding2. Return connection3. Workholding4. Site hot-work permit conditions | ||||
| 5. Weld and monitor | 1. Arc injury2. Fume inhalation3. Wire injury4. Defective joint | 1. Screen moved2. Hood misplaced3. Unsafe torch direction4. Wrong gas setting | 1. Maintain arc screens2. Capture fumes3. Keep wire clear4. Follow qualified WPS | 1. Hood and screen2. Wire feed direction3. Gas and consumables4. Weld parameters | ||||
| 6. Stop and inspect | 1. Residual gas leak2. Hot-metal burn3. Smoldering fire4. Unaccepted weld | 1. Valve left open2. Unsafe torch storage3. Fire check omitted4. Defects ignored | 1. Follow gas shutdown2. Park torch safely3. Check heat paths4. Inspect affected joints | 1. Valve and pressure2. Torch and leads3. Fire-watch closure4. Weld inspection | ||||
| 7. Hold abnormalities | 1. Gas exposure2. Feed entrapment3. Repeated weld fault4. Missed affected joints | 1. Arc-off assumption2. No feed isolation3. Repair-only restart4. Stop point unrecorded | 1. Restrict gas area2. Isolate feed adjustment3. Recheck air and setup4. Mark affected welds | 1. CO2/O2 and leak evidence2. Drive isolation3. Repair and restart4. Joint IDs and limits | ||||
| 8. Close and handover | 1. Later gas release2. Residual heat3. Unchecked weld used4. Damaged tool reused | 1. Supply not closed2. Hidden sparks missed3. Hold status absent4. Fault not transferred | 1. Close gas and power2. Check exposed areas3. Link joint inspections4. Tag defective equipment | 1. Supply and torch state2. Fire-watch completion3. Joint acceptance4. Equipment restrictions |
P = likelihood; S = severity; R = risk under the site method; A = site-defined acceptance/authorization. These actual assessment cells are blank. A low score never overrides a missing safeguard or a legal or manufacturer restriction.
4. Fictional scenario and failure mechanisms
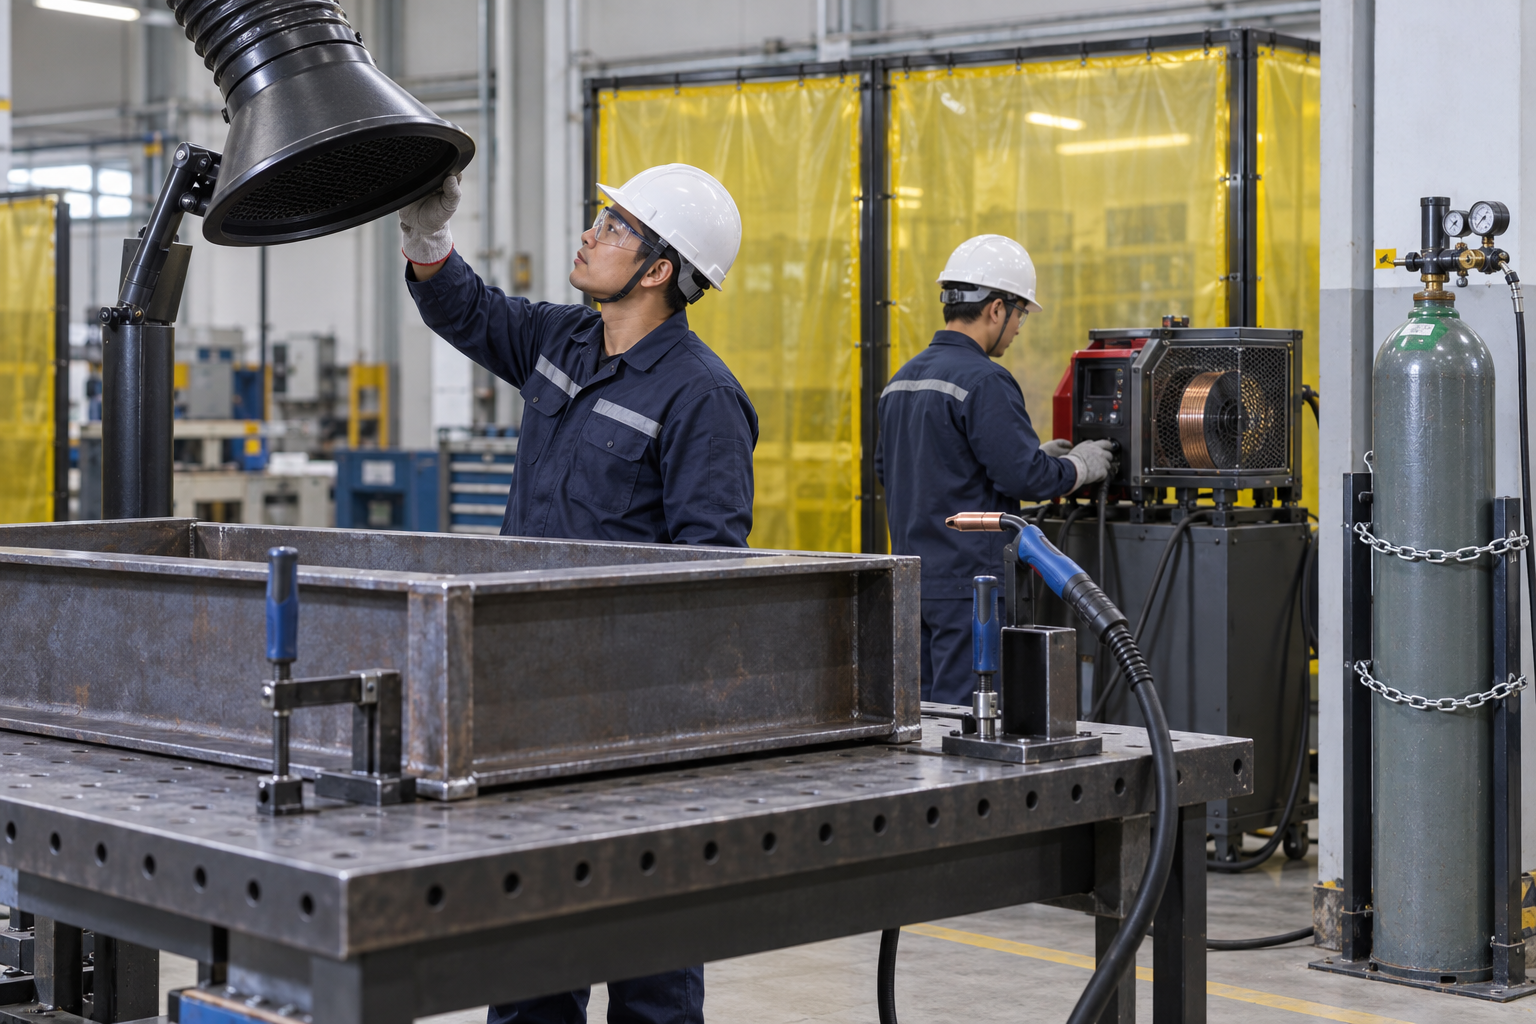
This illustration provides educational context. It is not an actual incident photograph or evidence of equipment suitability; any AI-generated depiction is illustrative only.
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Stage | Fictional situation |
|---|---|
| Initial situation | The arc is off during a break, but the cylinder and hose remain connected. |
| Changed condition | A leak is suspected near a low work area. |
| Failure path | The crew assumes nonflammable CO2 and a stopped arc mean the area is safe. |
| Possible outcome | Gas accumulation and harmful exposure can remain despite no visible welding fumes. |
| Prevention barrier | Restrict entry, shut the supply from a safe position and verify the repaired system, ventilation and required atmosphere measurements before restart. |
Failure mechanisms
An extinguished arc does not stop a gas leak. CO2 is nonflammable but can accumulate and harm workers; an oxygen reading alone is not a CO2 exposure assessment.
A functioning fume hood and an acceptable gas environment are different checks. Select measurement targets, locations and instruments for the actual gas and ventilation arrangement, including low areas.
Wire-feed rolls can pinch and wire can puncture while the arc is off. Isolate the feed system before covered adjustment, control torch direction, and evaluate already-welded joints separately after a gas-system defect.
Decision sequence
| Step | Decision |
|---|---|
| Known | The arc is off but leakage is suspected beside a low work area. |
| Unknown | Leak location/rate, CO2 concentration, oxygen condition and the extent of the affected area are unverified. |
| Hold | Nonflammability and arc-off do not remove gas exposure; restrict entry. |
| Evidence | Link gas-system IDs, safe supply shutoff, leak-test result, ventilation and suitable atmosphere measurements to time and location. |
| Restart | Release the repaired equipment, work-area conditions and affected weld inspection separately before resuming the accepted WPS. |
Work sequence: Plan gas and weld → Arrange work → Check gas and feed → Check electrical → Weld and monitor → Stop and inspect → Hold abnormalities → Close and handover. This is a teaching flow, not a device drawing or a complete operating procedure.
5. Conditional decisions and common errors
| Situation | Required action | Evidence | Proceed when |
|---|---|---|---|
| Suspected leak | Stop and restrict access | Supply isolation and leak test | Leak controlled |
| Air unknown | Assess CO2 and oxygen as needed | Instrument, location and results | Air criteria met |
| Feed fault | Isolate before adjustment | Energy and guard verification | Feeder restored |
| Gas repaired | Review environment and affected joints | Measurements and weld IDs | Restart scope released |
Similar observations, different decisions
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Observation | Insufficient conclusion | Required distinction |
|---|---|---|
| Connection replaced | The area is safe to enter. | Check the leaked gas, effective ventilation and the relevant atmosphere criteria. |
| Oxygen reading acceptable | CO2 is also acceptable. | Use gas-specific assessment and instruments; an oxygen result alone is insufficient. |
| Weld bead looks sound | Gas deviation caused no defect. | Identify affected joint lengths and apply the specified examination/disposition. |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Confirm sds and gas/fume monitoring and the task scope, resources, interfaces and stop authority. |
| Qualified technical reviewer | Review cylinder restraint, model limits, compatibility and unresolved technical conditions within assigned competence. |
| Work crew | Apply the listed controls, report changes and stop when evidence or safeguards are missing. |
| Inspector / assessor | Record actual hood and screen and other relevant checks; do not mark unverified conditions as accepted. |
| Handover authority | Reconcile supply and torch state, restrictions and outstanding actions before the next task. Role labels do not establish a legal credential. |
Supervision and handover focus
| Stage | Management action | Evidence |
|---|---|---|
| Plan gas and weld | 1. Record sds and gas/fume monitoring2. Record joint and wps3. Record fume control plan | 1. SDS and gas/fume monitoring2. Joint and WPS3. Fume control plan |
| Check gas and feed | 1. Record gas compatibility2. Record leak test result3. Record feed guard and isolation | 1. Gas compatibility2. Leak test result3. Feed guard and isolation |
| Check electrical | 1. Record leads and grounding2. Record return connection3. Record workholding | 1. Leads and grounding2. Return connection3. Workholding |
| Weld and monitor | 1. Record hood and screen2. Record wire feed direction3. Record gas and consumables | 1. Hood and screen2. Wire feed direction3. Gas and consumables |
| Hold abnormalities | 1. Record co2/o2 and leak evidence2. Record drive isolation3. Record repair and restart | 1. CO2/O2 and leak evidence2. Drive isolation3. Repair and restart |
| Close and handover | 1. Record supply and torch state2. Record fire-watch completion3. Record joint acceptance | 1. Supply and torch state2. Fire-watch completion3. Joint acceptance |
7. Hold points and record comparison
| Hold point | Evidence before release | Actual approval |
|---|---|---|
| HP-0 Scope | Prepare cylinders, wire feed, electrical equipment and workpieces for semiautomatic GMAW using carbon dioxide shielding gas; weld, stop, inspect and hand over affected joints. | |
| HP-1 Check gas and feed | Gas compatibility; Leak test result; Feed guard and isolation; Wire path | |
| HP-2 Check electrical | Leads and grounding; Return connection; Workholding; Site hot-work permit conditions | |
| HP-3 Weld and monitor | Hood and screen; Wire feed direction; Gas and consumables; Weld parameters | |
| HP-4 Close and handover | Supply and torch state; Fire-watch completion; Joint acceptance; Equipment restrictions |
Hold points are internal project checks. They are not universal statutory permits and do not grant work permission. Reassess after defects, changed conditions and shift changes.
Record comparison
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
The boxes are static record prompts, not interactive or saved approvals. A tick does not establish suitability or permission to restart. Record the evidence, person, time and unresolved issues; retain the change history.
| Record | Insufficient record | Record checklist |
|---|---|---|
| Plan gas and weld | Only marked “OK” | □ SDS and gas/fume monitoring□ Joint and WPS□ Fume control plan□ Supply shutoff point |
| Check electrical | Only marked “OK” | □ Leads and grounding□ Return connection□ Workholding□ Site hot-work permit conditions |
| Hold abnormalities | Only marked “OK” | □ CO2/O2 and leak evidence□ Drive isolation□ Repair and restart□ Joint IDs and limits |
| Close and handover | Only marked “OK” | □ Supply and torch state□ Fire-watch completion□ Joint acceptance□ Equipment restrictions |
8. Site checklist and emergency response
| Site check | Actual result | Person / action |
|---|---|---|
| Plan gas and weld: SDS and gas/fume monitoring; Joint and WPS; Fume control plan; Supply shutoff point | ||
| Arrange work: Cylinder restraint; Hose routing; Screens and access; Fixture condition | ||
| Check gas and feed: Gas compatibility; Leak test result; Feed guard and isolation; Wire path | ||
| Check electrical: Leads and grounding; Return connection; Workholding; Site hot-work permit conditions | ||
| Weld and monitor: Hood and screen; Wire feed direction; Gas and consumables; Weld parameters | ||
| Stop and inspect: Valve and pressure; Torch and leads; Fire-watch closure; Weld inspection | ||
| Hold abnormalities: CO2/O2 and leak evidence; Drive isolation; Repair and restart; Joint IDs and limits | ||
| Close and handover: Supply and torch state; Fire-watch completion; Joint acceptance; Equipment restrictions |
Stop work
Stop for suspected gas leakage, ineffective ventilation or fume capture, damaged insulation, abnormal wire feed or a WPS deviation. Restrict any area with an unverified atmosphere; arc-off is not clearance to enter.
Emergency response
Withdraw and prevent entry into the suspected gas area. Shut off gas and power only from a safe position under the site procedure. Call 995 for a medical emergency and give the gas, location and access details. Do not enter for an unprotected rescue; trained responders control the atmosphere and isolation hazards.
9. Sources and review limits
Public-source access/review: 2026-10-14.
| Official source | Reviewed scope and limits |
|---|---|
| MOM: Risk management | Assess welding, breaks, gas leakage and feeder fault recovery as separate exposure conditions. Official explanation of statutory duties; linked SSO text was not independently read for this item. This is not a legal opinion. |
| MOM/NEA/SCDF: Revised SS 586 adoption | Verify actual gas and consumable identification and the Singapore-appropriate SDS. Official adoption circular, not full paid SS 586 text or a classification of the actual product; verify current supplier label and SDS. |
| WSH Council: Managing WSH for SMEs in Metalworking | Plan fire prevention, screens, fume extraction, opposite-side checks and post-work fire watch. Official sector guidance and sample controls, not a universal statutory permit rule, a qualified WPS or a current-edition certificate. Linked paid standards were not read; direct SSO General Provisions access returned 403. |
| MOM: Requirements for Hygiene Monitoring | Have competent personnel select relevant gas/fume exposure monitoring and Singapore criteria. Actual substances, exposure results and legal limits must be established for the site. No concentration or noise result is asserted. |
| WSH Council: Safe Use of Machinery | Isolate the powered feeder for intervention even when the arc is extinguished. Official guidance; cited paid Singapore Standards were not obtained. No universal wheel test duration or gap is inferred. |
| SCDF: Emergency Medical Services | Call 995 for a medical emergency without unprotected entry into a suspect atmosphere. Official emergency-response information, not a site-specific rescue plan or authorisation for untrained rescue. |
No actual equipment model, site measurements, design calculations or signed approval was supplied. Check the applicable Singapore requirements and approved safe work procedures against the actual equipment and site before use. Statutory duties, official guidance and manufacturer limits serve different purposes; editorial checks do not establish legal or professional approval.
10. PDF guidance and FAQ
PDF A covers basic task controls; B focuses on technical failures; C covers supervision, records and handover. The article has eight stages with four items per main cell; each PDF has six key stages with three items per main cell. P/S/R/A, measurements, confirmations and signatures remain blank for actual site assessment.
PDFs are complementary six-stage extracts. Apply all eight body stages and the actual equipment/site procedure.
Does nonflammable CO2 eliminate ventilation needs?
No. Assess CO2 accumulation and welding fumes separately.
Does normal oxygen prove acceptable CO2?
No. Choose gas-specific monitoring and exposure criteria for the actual conditions.
Can feed rolls be adjusted with the arc off?
Arc-off does not establish feeder isolation. Follow the applicable servicing procedure.
Does replacing a hose authorise restart?
Verify leak control, the work-area atmosphere and welding conditions; identify joints affected by the defect.
Has a professional verified or approved this document?
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to Singapore requirements, the actual equipment/site and approved safe work procedures.
11. Revision history and authorship
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to Singapore requirements, the actual equipment/site and approved safe work procedures.
| Date | Version | Change | Review status |
|---|---|---|---|
| 2026-10-14 | SG 1.0 | New Singapore edition from assigned Korean source; task decisions, records and PDFs localized. | AI editorial review; no professional technical approval |
Korean edition revision history: 2026-09-20 (v1.0): initial article, sources, fictional analysis and PDF editorial checks; 2026-09-23 (v1.1): task decisions, record checklist, JSA and three PDF variants revised. These are editorial records, not professional technical approval. Singapore v1.0 adapts the earlier edition to Singapore requirements and terminology.
Site reviewers must add their actual qualifications, scope, date and approval only after the review occurs.