Transfer mounting force to the ring with the interference fit. Loading the opposite ring through rolling elements can damage internal contacts. A simultaneous interference fit requires the specified tooling for both rings.
This reference material was written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
Stop before proceeding
Do not load an unverified fit, ring contact, fixture or press configuration. Stop for skew, fixture movement, unexpected resistance, cracking, unusual noise or hydraulic leakage; control the load before inspection.
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to applicable Singapore requirements, the actual equipment/site and approved safe work procedures.
1. Legal and technical scope
Use the Singapore risk assessment and machinery safeguarding/energy-isolation framework for this maintenance hydraulic press. The WSH Council guide supplies general machine-control principles; it is not a bearing mounting specification. Identify the actual press type and applicable Singapore requirements rather than importing a foreign mechanical-power-press rule.
| Basis | Singapore application |
|---|---|
| Risk management | The employer, self-employed person and principal assess and control work risks. Include preparation, abnormal conditions and maintenance. Coordinate affected trades and communicate controls. |
| Activity-specific guidance | Use machinery guidance to establish competent operation, effective guards, safe setup/clearing and energy isolation; resolve ring loading, fit and bearing acceptance from the actual design and manufacturer. |
| Permits and authority | Select permit requirements for the actual sector and activity. Site hold points and contractor role labels do not create statutory permits or qualifications. |
| Equipment and design | The machinery guide refers power presses to separate guidance; this article applies its general safeguarding and isolation principles only. The press, bearing and fixture manuals were not supplied. No universal pressing force, hydraulic pressure or fixture rating is inferred. |
2. Scope and required inputs
Included scope
Cold press-fit an approved bearing onto a detached shaft or into a detached housing using a maintenance hydraulic press and verified support tooling.
Separate assessment
Bearing removal, heating, oil injection, hydraulic nuts, spring-loaded assemblies, tooling fabrication and production mechanical presses are separate assessments.
| Input | Evidence needed |
|---|---|
| Identify fit | Shaft and bearing IDs; Fit and tolerance; Direction and shoulder; Tool capacity. |
| Prepare parts | Handling method; Surface and burrs; Sleeve condition; Lubrication instruction. |
| Press and watch | Pressure and travel; Part alignment; Noise and leakage; Protected observation. |
| Handoff assembly | Assembly ID and values; Acceptance status; Press and fixture state; Receiving person. |
No site measurements, equipment manuals for the actual installation, inspection records or signed technical approvals were supplied. Confirm the applicable requirements and actual product instructions before use; record each criterion with its units, source and equipment or work-area ID.
Singapore site planning
The workshop employer and person controlling the press must approve a task-specific SWP that identifies the interference ring, support sleeve and full load path. Coordinate any lifting of the detached shaft or housing as a separate handling step. Record fit and travel in mm, force in kN where a valid conversion exists, and pressure with its stated unit. Retain a hold tag on any assembly exposed to skew or abnormal force; a completed seating dimension does not authorise installation back into plant.
3. Eight-stage JSA
| Job stage | Hazards and effects | Failure factors | Technical and procedural controls | Site verification | P | S | R | A |
|---|---|---|---|---|---|---|---|---|
| 1. Identify fit | 1. Internal damage2. Wrong insertion3. Overload4. Wrong assembly | 1. Part ID mismatch2. Wrong loaded ring3. Unknown fit4. Tool limit missed | 1. Match part drawing2. Identify interference ring3. Confirm insertion depth4. Check full load path | 1. Shaft and bearing IDs2. Fit/tolerance (mm)3. Direction and shoulder4. Tool capacity | ||||
| 2. Inspect press | 1. Press instability2. Flying tooling3. Fluid injection4. Crushed hand | 1. Weak bed support2. Missing shielding3. Damaged hose4. Bad controls | 1. Inspect frame and pins2. Provide suitable guards3. Reject leaking system4. Check stop controls | 1. Foundation and bed2. Guard arrangement3. Hoses and cylinder4. Operator position | ||||
| 3. Prepare parts | 1. Dropped component2. Contamination damage3. Tool failure4. Wrong orientation | 1. Poor handling support2. Burrs left in fit3. Improvised blocks4. No direction mark | 1. Support detached parts2. Clean and inspect fit3. Use rated tooling4. Mark assembly direction | 1. Handling method2. Surface and burrs3. Sleeve condition4. Lubrication instruction | ||||
| 4. Align tooling | 1. Ejected bearing2. Rolling-element damage3. Support collapse4. Finger crush | 1. Off-centre ram2. Wrong ring contact3. Small support area4. Hand-held alignment | 1. Align ram and part2. Load correct ring3. Secure stable supports4. Withdraw hands first | 1. Concentric contact2. Ring and sleeve path3. Support rating4. Hands and tools clear | ||||
| 5. Press and watch | 1. Bearing cracking2. Tool movement3. Overload failure4. Body crushing | 1. Skew continues2. Fixture shifts3. Resistance ignored4. Hand adjustment | 1. Follow mounting method2. Watch tooling position3. Stop abnormal resistance4. Keep clear under load | 1. Pressure/travel with units2. Part alignment3. Noise and leakage4. Protected observation | ||||
| 6. Unload and inspect | 1. Stored-load release2. Falling part3. Incomplete seating4. Hidden damage | 1. Support removed early2. Hands enter loaded zone3. No depth check4. Appearance-only pass | 1. Support before release2. Verify unloaded state3. Measure final seating4. Apply damage checks | 1. Unloading sequence2. Ram safe state3. Depth and dimensions4. Bearing disposition | ||||
| 7. Resolve fault | 1. Further breakage2. Damaged bearing reused3. Improvised repair4. Fixture recurrence | 1. More pressure applied2. Wrong path ignored3. Hammering attempted4. Tool defect retained | 1. Control load and stop2. Assess bearing damage3. Correct fit and path4. Approve rework plan | 1. Fault pressure and travel2. Affected ring and tool3. Dimensional evidence4. Retest or replacement | ||||
| 8. Handoff assembly | 1. Faulty assembly used2. Part mix-up3. Unsafe press reuse4. Unresolved defect | 1. Results lack ID2. Hold tag missing3. Leak left unreported4. Owner unclear | 1. Link assembly results2. Separate held parts3. Inspect press after work4. Transfer restrictions | 1. Assembly ID and values2. Accepted or held status3. Press and fixture state4. Receiving person |
P = likelihood; S = severity; R = risk using the site method; A = site acceptance/authorisation. Complete after actual assessment; no score overrides an unresolved hold point or equipment limit.
4. Fictional scenario and failure mechanisms
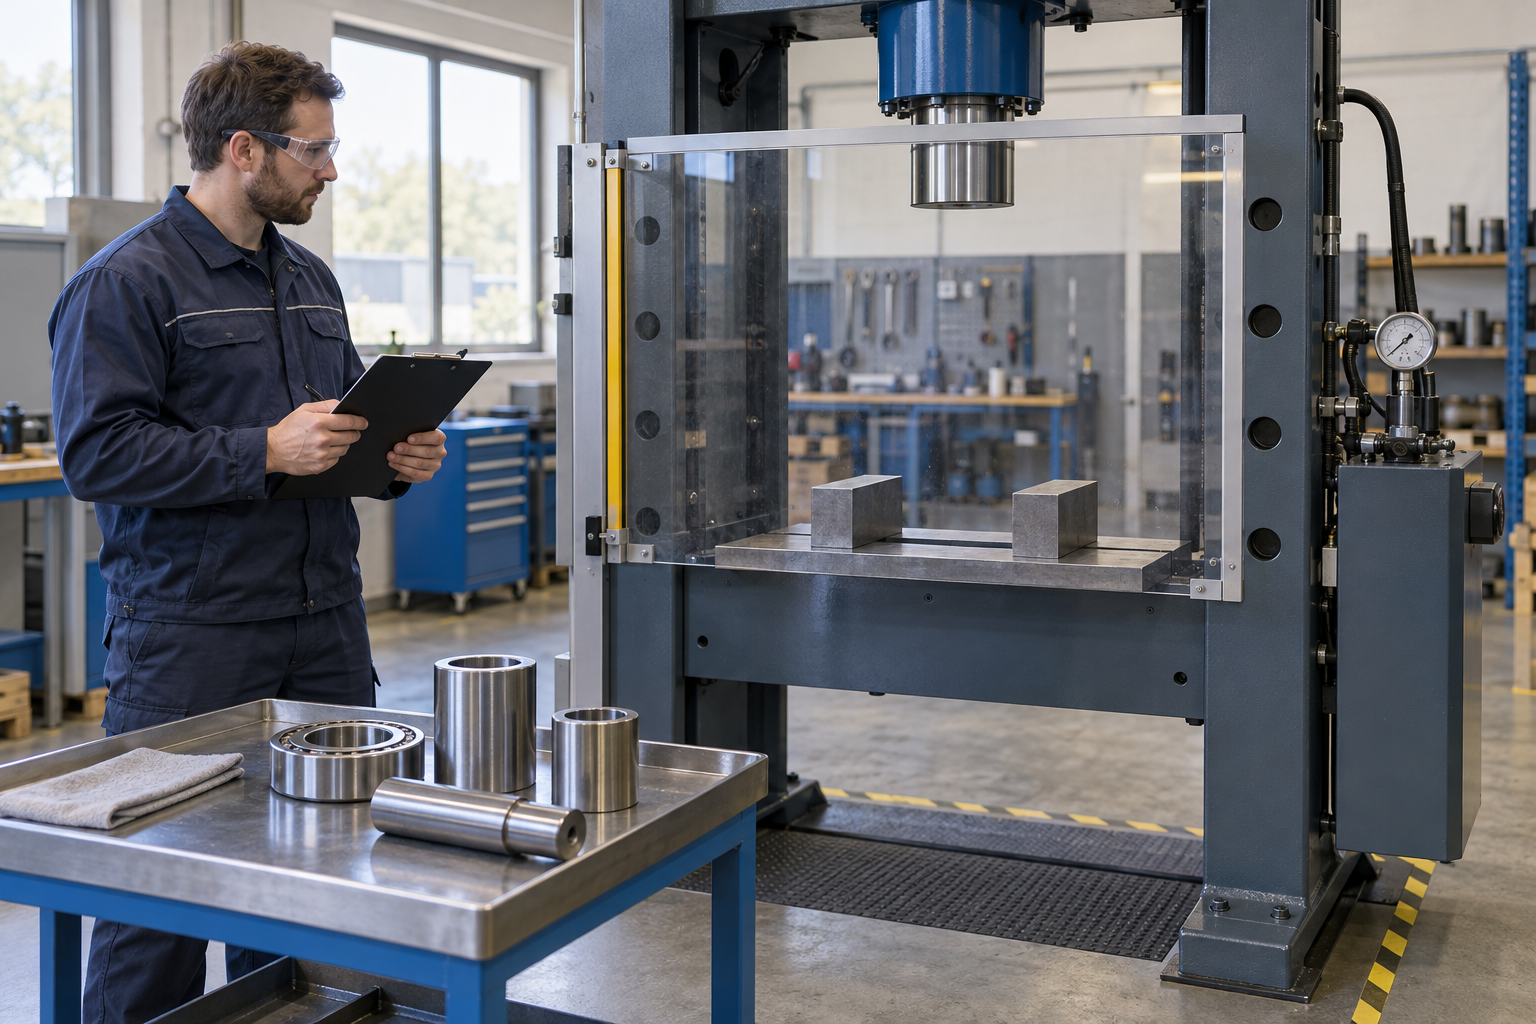
Retained AI-generated educational illustration from the source edition; not a real incident photograph, approved installation drawing or evidence of equipment suitability.
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Item | Fictional scenario |
|---|---|
| Initial | An inner ring is being fitted to a shaft. |
| Change | The sleeve bears on the outer ring and the bearing tilts. |
| Failure | Force crosses rolling elements while pressure rises. |
| Outcome | Internal bearing damage or ejected tooling can result. |
| Barrier | Stop, control the load, use the specified unloading method and inspect dimensions, tooling and the affected bearing before rework. |
Why the controls matter
Transfer mounting force to the ring with the interference fit. Loading the opposite ring through rolling elements can damage internal contacts. A simultaneous interference fit requires the specified tooling for both rings.
Gauge pressure alone does not certify force or tooling capacity. Check the cylinder relationship and the limits of the entire load path, including bed pins, supports and sleeves.
Full seating can coexist with damage from skew or the wrong load path. Stop on unexpected resistance, inspect the assembly and segregate it until the specified acceptance checks are complete.
Decision sequence
| Step | Decision |
|---|---|
| Known | The sleeve bears on the outer ring and the bearing tilts. |
| Unknown | Actual condition, extent of damage and suitability of pressure and travel, part alignment remain to be established. |
| Hold | Force crosses rolling elements while pressure rises. |
| Evidence | Link pressure and travel, part alignment, noise and leakage, protected observation, fault pressure and travel, affected ring and tool to the affected equipment or work area. |
| Next | Stop, control the load, use the specified unloading method and inspect dimensions, tooling and the affected bearing before rework. |
5. Conditional decisions and common errors
| Condition | Action | Evidence | Proceed when |
|---|---|---|---|
| Ring unclear | Verify interference and sleeve contact | Drawing and load-path sketch | Correct ring supported |
| Pressure rises | Stop and unload safely | Pressure, travel and symptom record | Cause corrected |
| Tooling shifts | Hold the assembly | Support and alignment inspection | Tooling stable |
| Fully seated | Inspect before release | Dimensions and damage disposition | Assembly accepted |
Similar appearance, different evidence
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
| Comparison | Supported decision | Insufficient basis |
|---|---|---|
| Condition | Drawing and load-path sketch | Ring unclear has not been resolved. |
| Evidence | Support and alignment inspection | A photograph or a completed-looking task without the relevant inspection record. |
| Release | Assembly accepted | Completion of one step does not release the excluded tasks in section 2. |
6. Roles and responsibilities
| Role | Responsibility |
|---|---|
| Work supervisor | Assign the task boundary, stop authority, interfaces and emergency communication for hydraulic press bearing installation. |
| Technical lead | Confirm Shaft and bearing IDs; Fit and tolerance; Direction and shoulder; Tool capacity. Resolve design and manufacturer limits before work. |
| Authorised crew | Apply Handling method; Surface and burrs; Sleeve condition; Lubrication instruction. Stop when the working arrangement changes. |
| Inspector / receiving lead | Review Pressure and travel; Part alignment; Noise and leakage; Protected observation. Transfer Assembly ID and values; Acceptance status; Press and fixture state; Receiving person. |
Role labels allocate responsibilities; they do not confer a legal qualification. Verify the competence, training and authority required for the actual task.
The principal and employers coordinate the risk assessment and safe work procedures. These role labels allocate work; verify any qualifications and statutory appointments required for the actual Singapore activity. The receiving person must be given restrictions and unresolved defects before handover.
Record and handover perspective
| Stage | Record controls | Verification |
|---|---|---|
| Identify fit | 1. Record shaft and bearing ids2. Record fit/tolerance (mm)3. Record direction and shoulder | 1. Fit/tolerance (mm)2. Direction and shoulder3. Tool capacity |
| Prepare parts | 1. Record handling method2. Record surface and burrs3. Record sleeve condition | 1. Surface and burrs2. Sleeve condition3. Lubrication instruction |
| Align tooling | 1. Record concentric contact2. Record ring and sleeve path3. Record support rating | 1. Ring and sleeve path2. Support rating3. Hands and tools clear |
| Press and watch | 1. Record pressure/travel with units2. Record part alignment3. Record noise and leakage | 1. Part alignment2. Noise and leakage3. Protected observation |
| Resolve fault | 1. Record fault pressure and travel2. Record affected ring and tool3. Record dimensional evidence | 1. Affected ring and tool2. Dimensional evidence3. Retest or replacement |
| Handoff assembly | 1. Record assembly id and values2. Record accepted or held status3. Record press and fixture state | 1. Accepted or held status2. Press and fixture state3. Receiving person |
7. Hold points and record comparison
| Hold point | Evidence before release | Actual record |
|---|---|---|
| HP-0 Start | Task boundary, site RA, SWP, responsibilities and emergency arrangements | |
| HP-1 Inspect press | Foundation and bed; Guard arrangement; Hoses and cylinder; Operator position | |
| HP-2 Prepare parts | Handling method; Surface and burrs; Sleeve condition; Lubrication instruction | |
| HP-3 Unload and inspect | Unloading sequence; Ram safe state; Depth and dimensions; Bearing disposition | |
| HP-4 Handoff assembly | Assembly ID and values; Accepted or held status; Press and fixture state; Receiving person |
These are internal hold points, not issued permits. Recheck affected points after a change, fault or shift handoff; link the actual approval record.
Record comparison
The scenario and record comparisons are fictional teaching examples, not records of real incidents, measurements, inspections, signatures or approvals.
The boxes are static record prompts, not interactive or saved approvals. A tick does not establish suitability or permission to restart. Record the evidence, person, time and unresolved issues; retain the change history.
| Record | Insufficient | Record checklist |
|---|---|---|
| Identify fit | "Checked" without target, criteria or result | □ Shaft and bearing IDs□ Fit and tolerance□ Direction and shoulder□ Tool capacity |
| Prepare parts | "Checked" without target, criteria or result | □ Handling method□ Surface and burrs□ Sleeve condition□ Lubrication instruction |
| Press and watch | "Checked" without target, criteria or result | □ Pressure and travel□ Part alignment□ Noise and leakage□ Protected observation |
| Handoff assembly | "Checked" without target, criteria or result | □ Assembly ID and values□ Acceptance status□ Press and fixture state□ Receiving person |
Hold points are internal checks. Determine separately whether Singapore statutory or site permit requirements apply to this work. Leave confirmation, measurements and approval records blank until the authorised site process is completed.
8. Site checklist and emergency response
| Check | Result | Person / action |
|---|---|---|
| □ Identify fit: Shaft and bearing IDs | ||
| □ Inspect press: Foundation and bed | ||
| □ Prepare parts: Handling method | ||
| □ Align tooling: Concentric contact | ||
| □ Press and watch: Pressure and travel | ||
| □ Unload and inspect: Unloading sequence | ||
| □ Resolve fault: Fault pressure and travel | ||
| □ Handoff assembly: Assembly ID and values | ||
| □ Emergency access and handoff restrictions |
Stop work
Do not load an unverified fit, ring contact, fixture or press configuration. Stop for skew, fixture movement, unexpected resistance, cracking, unusual noise or hydraulic leakage; control the load before inspection.
Emergency response
Stop from a safe location, exclude people from the affected danger zone and activate the site emergency plan. Call the site emergency service for injury or immediate danger. Do not enter an unstable, energised or confined danger area for an improvised rescue; trained responders must control the specific energy and access hazards.
9. Sources and review limits
Official public sources read for this Singapore edition on 2026-10-14. Guidance, statutory explanations and manufacturer limits have different roles; no source provider has approved this JSA.
| Source | Read scope and application limits |
|---|---|
| MOM — Risk management | Official explanation: employer, self-employed person and principal responsibilities; routine and non-routine risk assessment; hierarchy of controls; multidisciplinary assessment team. Official explanation of risk-management duties; no claim of reading the full linked statute. It does not specify task-specific equipment limits. Assess hydraulic press bearing installation with employers, principal and affected contractors; resolve the inputs in section 2. |
| MOM — When should my company review its risk assessment? | Review every three years, after significant changes, new machinery/substances/procedures, hazard-related injury or incident, and when assessment is inadequate. General review guidance. A review interval does not permit continued operation after a known hazard or change. Reassess this operation after changes, defects, incidents or an inadequate assessment; do not wait for a scheduled review. |
| MOM — Permit-to-Work Systems | Formal work authorisation and coordination; OPEC tripartite guidance and competent permit authority with authority to reject work. OPEC-focused guidance page; not evidence of a blanket statutory permit requirement for every task. Determine permits for this actual activity and workplace; distinguish the section 7 internal hold points from statutory or site permits. |
| WSH Council — Guidelines on Safe Use of Machinery | Sections 1.1 and 1.3: scope and explanation of safeguarding/LOTO duties. Sections 4.3–4.4.3: training, maintenance, specified replacement parts and isolation of all energy sources; commissioning safety-device checks. Official practical guidance and explanation; complete current subsidiary legislation and every annex were not read. Actual manufacturer isolation and restoration instructions remain necessary. Use machinery guidance to establish competent operation, effective guards, safe setup/clearing and energy isolation; resolve ring loading, fit and bearing acceptance from the actual design and manufacturer. |
The machinery guide refers power presses to separate guidance; this article applies its general safeguarding and isolation principles only. The press, bearing and fixture manuals were not supplied. No universal pressing force, hydraulic pressure or fixture rating is inferred.
Actual site measurements, equipment instructions, engineering checks and signed approval records were not supplied. A qualified person must resolve these before use.
10. PDF guidance and FAQ
PDF A covers basic task controls; B focuses on technical failures; C covers supervision, records and handover. The article has eight stages with four items per main cell; each PDF has six key stages with three items per main cell. P/S/R/A, measurements, confirmations and signatures remain blank for actual site assessment.
Content group
jsa-bearing-hydraulic-press-fit
Can the outer ring be pressed to fit an inner ring?
Do not transmit installation force through rolling elements. Apply the actual bearing mounting instructions.
Does a larger press solve rising resistance?
No. Investigate alignment, fit and load path before increasing force.
Is a seated bearing necessarily acceptable?
No. Check the specified position and damage criteria, especially after abnormal loading.
Does a general machine guide approve this press setup?
No. Establish the actual Singapore safeguarding and isolation requirements, then verify the press, tooling and bearing mounting instructions for this setup.
Has a professional approved this JSA?
This reference material was written and revised with AI. It has not been verified or approved by a professional. Review by a suitably qualified professional and required site approval are necessary before field use.
11. Revision history and authorship
AI-generated reference material; not professionally verified or approved. Before use, a qualified person must review and adapt it to applicable Singapore requirements, the actual equipment/site and approved safe work procedures.
This Singapore edition was adapted from the Korean original and its assigned US technical reference. Earlier source revisions are archival editorial history, not Singapore technical approval.
| Date | Edition | Change | Review status |
|---|---|---|---|
| 2026-09-23 | Korean source v1.0 | Source editorial publication or revision; retained as provenance of the Korean edition. | Editorial record only; no professional technical approval recorded. |
| 2026-10-14 | 1.0 en-SG | Singapore legal scope, local planning, responsibility interfaces and SI terminology; new PDF A/B/C. | AI editorial and visual review only; no professional approval. |